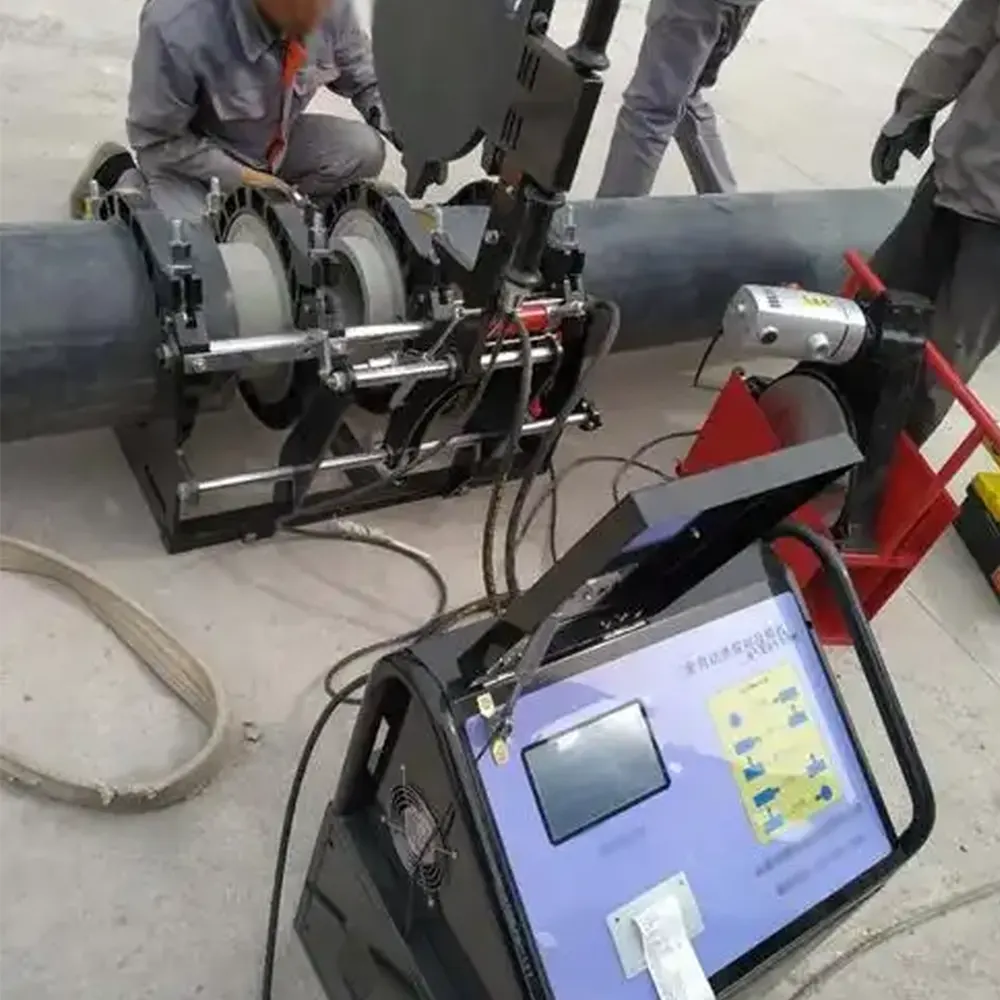
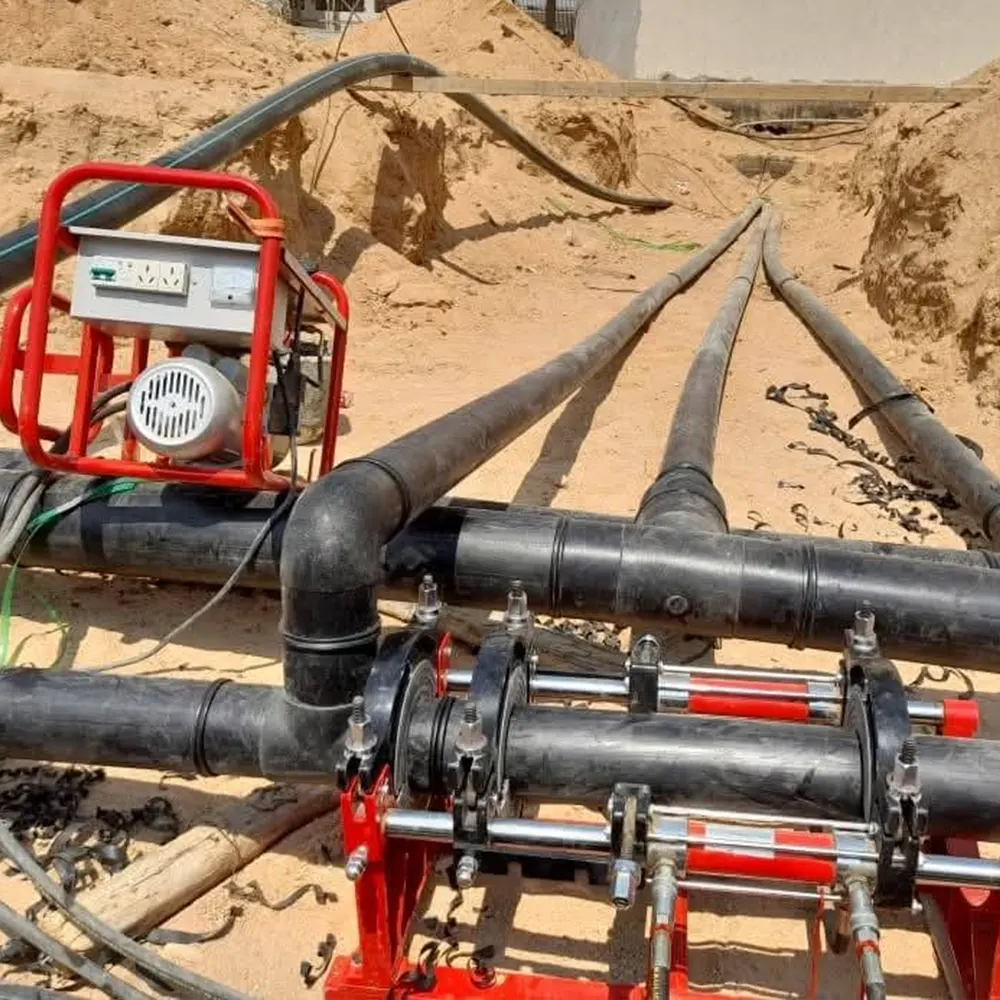
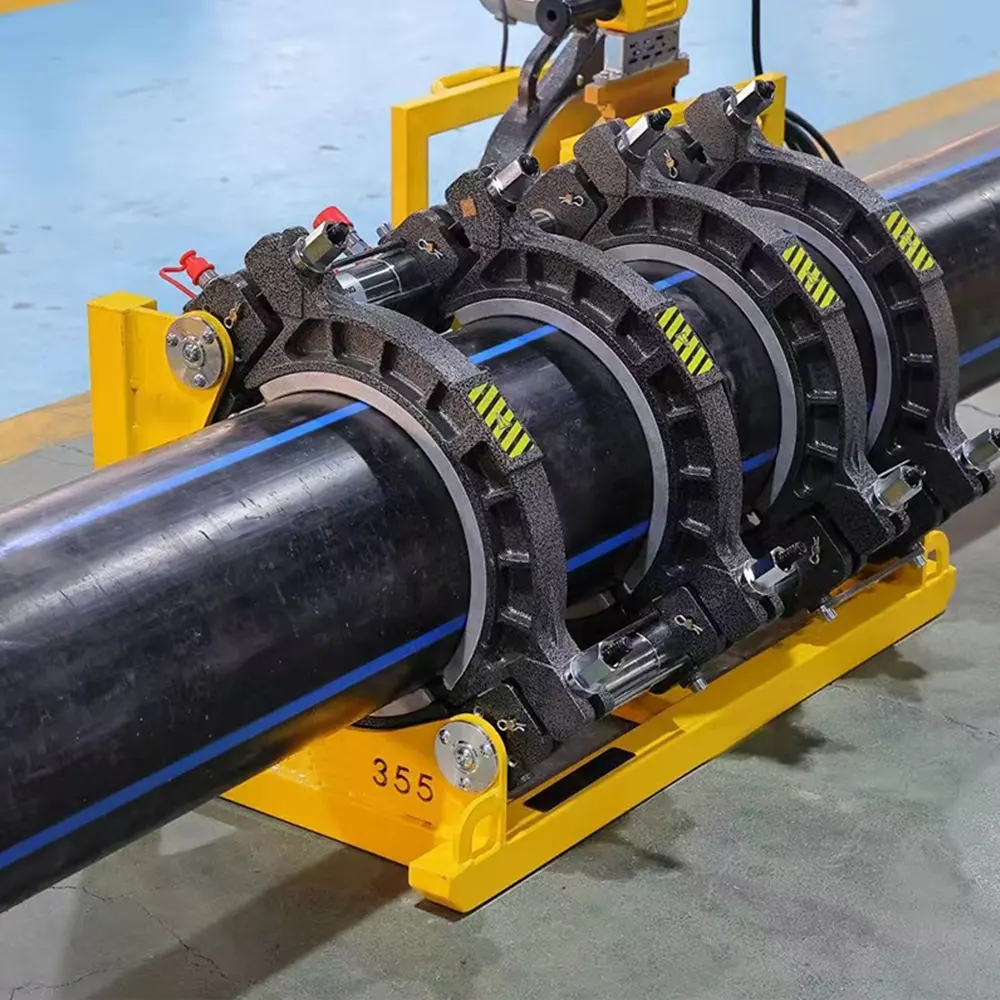
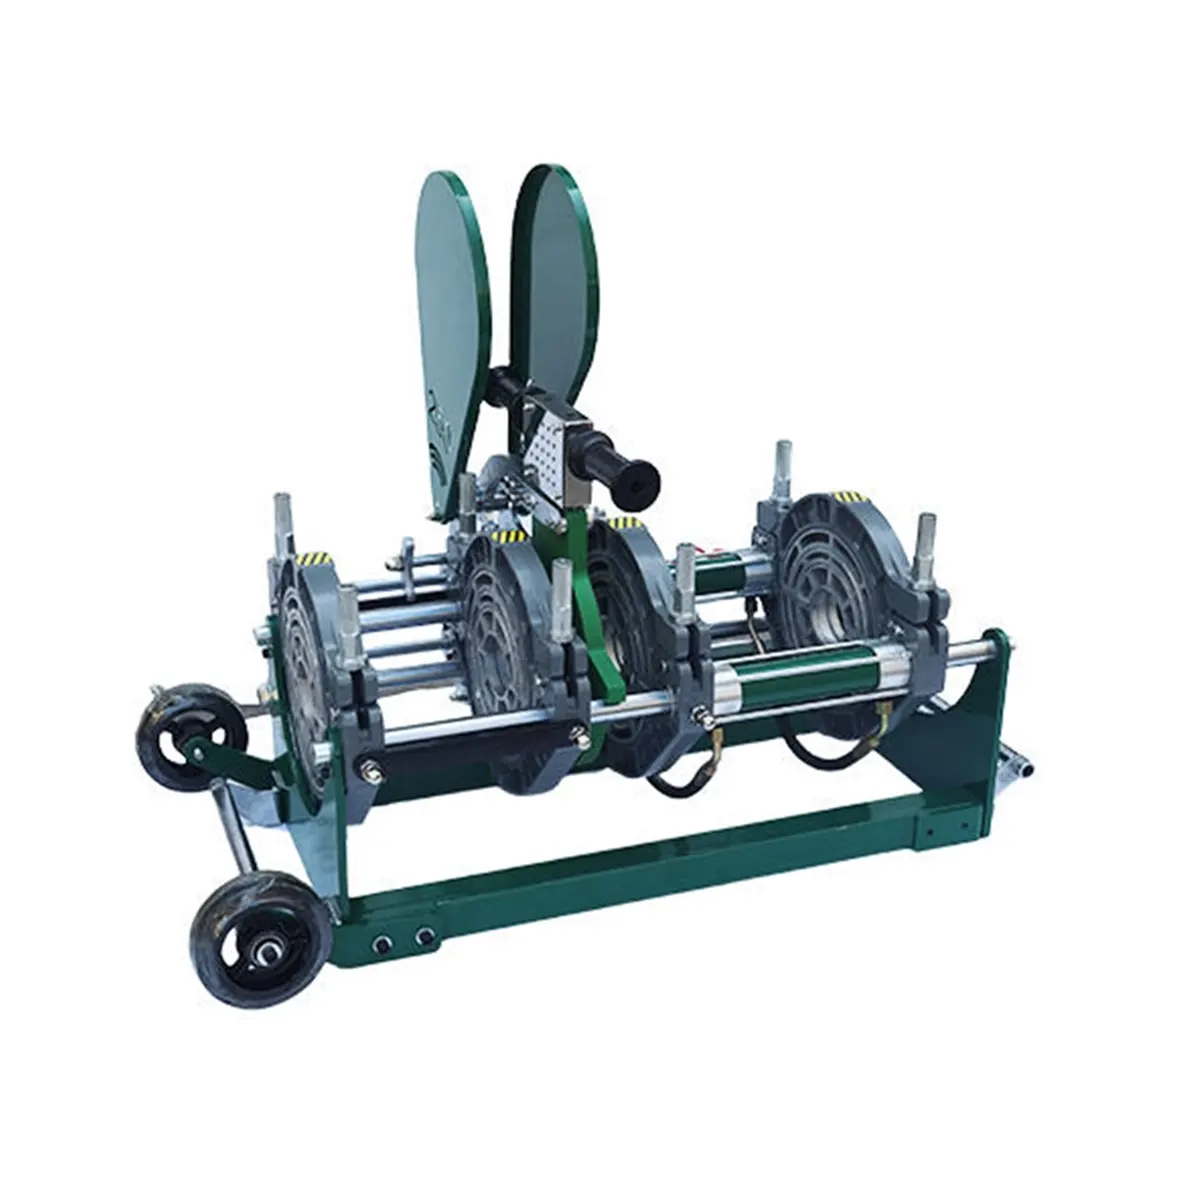
Polyethylene (PE) pipe welding equipment is essential for reliable HDPE pipeline installation, but even high-quality butt fusion machines can encounter recurring issues on site. This guide covers the most common problems, practical causes, and step-by-step solutions to help operators, contractors, and maintenance teams restore proper performance quickly.
Common Symptoms and Quick Checks
Before troubleshooting: verify power supply, confirm correct pipe material and SDR, and ensure an experienced operator is present. Quick pre-checks reduce downtime and avoid repeated weld defects.
- Cold or uneven weld bead: often visible immediately after cooling.
- Poor fusion line (voids or lack of bead): indicates temperature, pressure, or cleanliness issues.
- Machine stalls or inconsistent heating: could be electrical or sensor related.
- Misaligned pipes or clamp slippage: leads to weak joints and leak risk.
Problem 1 — Uneven Heating or Cold Spots
Causes: worn or contaminated heating plate, damaged thermostat, incorrect heater placement, or damaged insulation on the heater.
Solutions:
- Clean the heating plate with a soft cloth and isopropyl alcohol before each weld to remove contaminants.
- Inspect the heating plate surface for scratches or dents; replace if surface flatness is compromised.
- Verify thermostat calibration and use a contact thermometer to confirm plate temperature at several points.
- Replace or repair damaged heater insulation and wiring to ensure uniform heat distribution.
Problem 2 — Poor Fusion Line or Lack of Bead Formation
Causes: insufficient fusion time, wrong temperature settings, incorrect pressure, or contaminated pipe ends.
Solutions:
- Follow standardized fusion parameters: temperature, heating time, and upset/pressure based on pipe OD and SDR.
- Use proper facing/trimming tools to produce clean, square pipe ends; ensure no oxidation or debris remains.
- Increase heating time slightly for larger diameters or in cold environments (but follow recommended tolerance limits).
- Perform a test weld and cut a bead sample to visually confirm full penetration and consistent bead profile.
Problem 3 — Misalignment and Clamp Issues
Causes: worn clamp jaws, incorrect clamp setup, uneven bedding surface, or insufficient clamping pressure.
Solutions:
- Inspect and replace worn jaws, bolts, or locating pins. Keep spare clamps for high-utilization sites.
- Ensure the machine sits on a flat, stable base and use proper support blocks for large-diameter pipes.
- Set and monitor clamping pressure according to machine manuals; always lock clamp positions before heating.
- Use alignment gauges or laser guides for precision work on long pipelines or high-pressure systems.
Electrical, Sensor & Control Faults
Symptoms: inconsistent heater readings, error codes on the controller, or failure to maintain set temperature or hydraulic pressure.
Troubleshooting steps:
- Check main power, fuses, and grounding. Replace blown fuses and verify voltage stability.
- Inspect sensor connectors and replace corroded terminals. Re-calibrate or replace temperature sensors if readings drift.
- Examine the control unit for loose wiring, moisture ingress, or signs of overheating; consider a spare controller for critical projects.
- For hydraulic systems, confirm pump performance, fluid cleanliness, and correct oil level.
Operator Errors & Environmental Factors
Common human and site-driven issues: improper machine setup, incorrect parameter selection, windy/cold conditions, or dusty/wet work areas.
Mitigations:
- Provide operator training and reference quick-setup sheets near machines.
- Use windshields and tenting in adverse weather; adjust heating time per ambient temperature guidelines.
- Keep weld area clean and dry; use clean rags and approved cleaners for pipe ends and plates.
Troubleshooting Table — Fault, Likely Cause, Immediate Action
| Fault | Likely Cause | Immediate Action |
|---|---|---|
| Uneven bead | Heater damage/contamination | Clean/replace heater; verify temperature |
| No bead formation | Incorrect time/temp/pressure | Check parameters; perform test weld |
| Clamp slip | Worn jaws or loose fasteners | Tighten or replace clamp components |
| Controller errors | Sensor or wiring fault | Inspect wiring; swap sensor if available |
Preventive Maintenance Checklist
Routine upkeep reduces failures and extends machine life. Keep a simple log and check items before each shift.
| Interval | Task | Notes |
|---|---|---|
| Daily | Clean heating plate & facing tools | Use approved solvent; avoid abrasive pads |
| Weekly | Inspect clamps, bolts & hydraulic hoses | Replace worn parts; check hose fittings |
| Monthly | Test sensors & calibrate controller | Document calibration values |
| Annually | Full service: pump, motor, electrical checks | Use OEM parts where possible |
Field Tips for Contractors and Operators
Keep a small service kit on site: spare jaws, heater plates, thermostats, fuses, and basic hydraulic fittings. Always document weld parameters and environmental conditions for every joint — this helps diagnose repeat failures quickly.
When to Contact Manufacturer or Professional Service
If repeated defects persist after standard troubleshooting (heater replacement, sensor swap, calibration), escalate to certified service. For OEM parts, warranty checks, or complex electrical faults, contact the equipment manufacturer. Manufacturer: JQ-Fusion.
Consistent training, a disciplined maintenance routine, and quick access to spare parts dramatically reduce welding defects and downtime on PE pipeline projects. Use the steps above to diagnose and correct most common issues and keep weld quality high.