
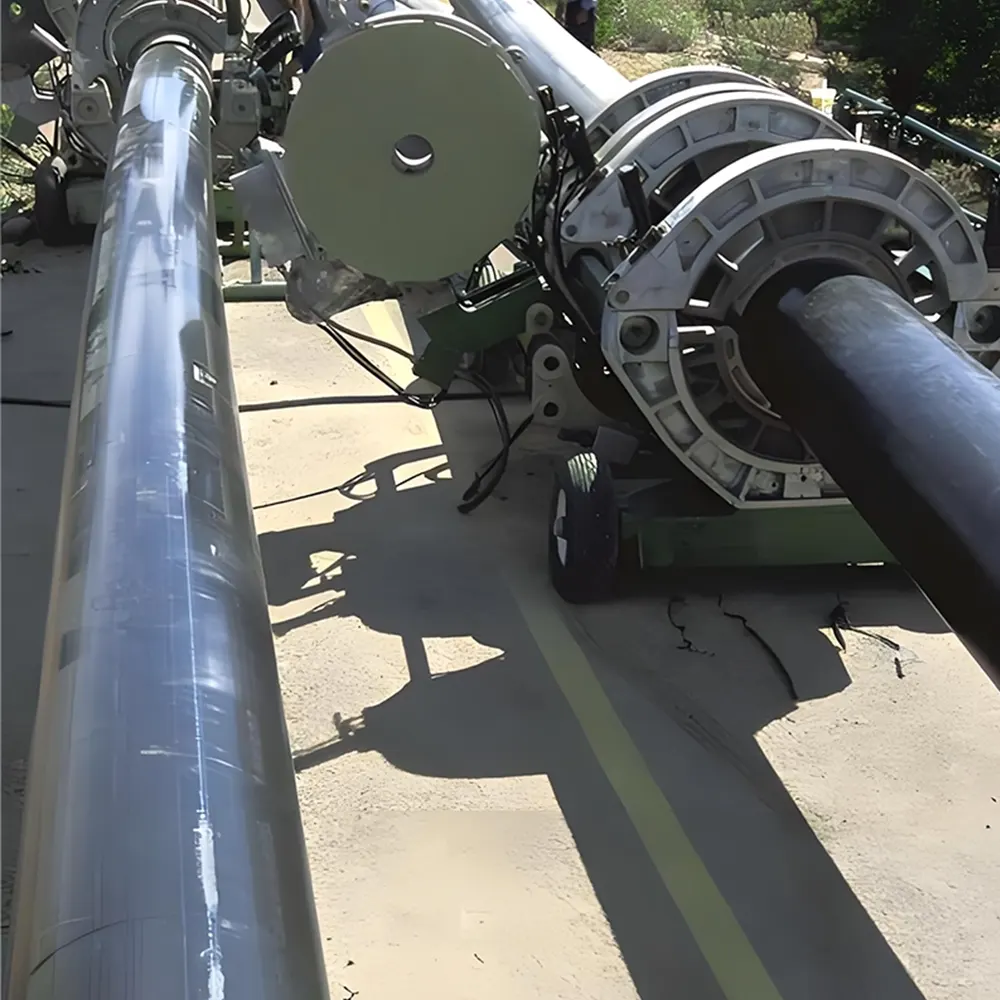
In the world of modern infrastructure, creating leak-proof, durable piping systems depends heavily on the quality of the joint. The butt fusion machine for pipeline construction has become the cornerstone of HDPE pipe welding, offering unmatched strength and reliability. Whether you are managing a municipal water supply project, a gas distribution network, or an industrial slurry line, selecting the right butt fusion equipment is a critical decision that impacts project timelines, budget, and long-term system integrity. This comprehensive guide walks you through everything you need to know before purchasing and operating your machine.
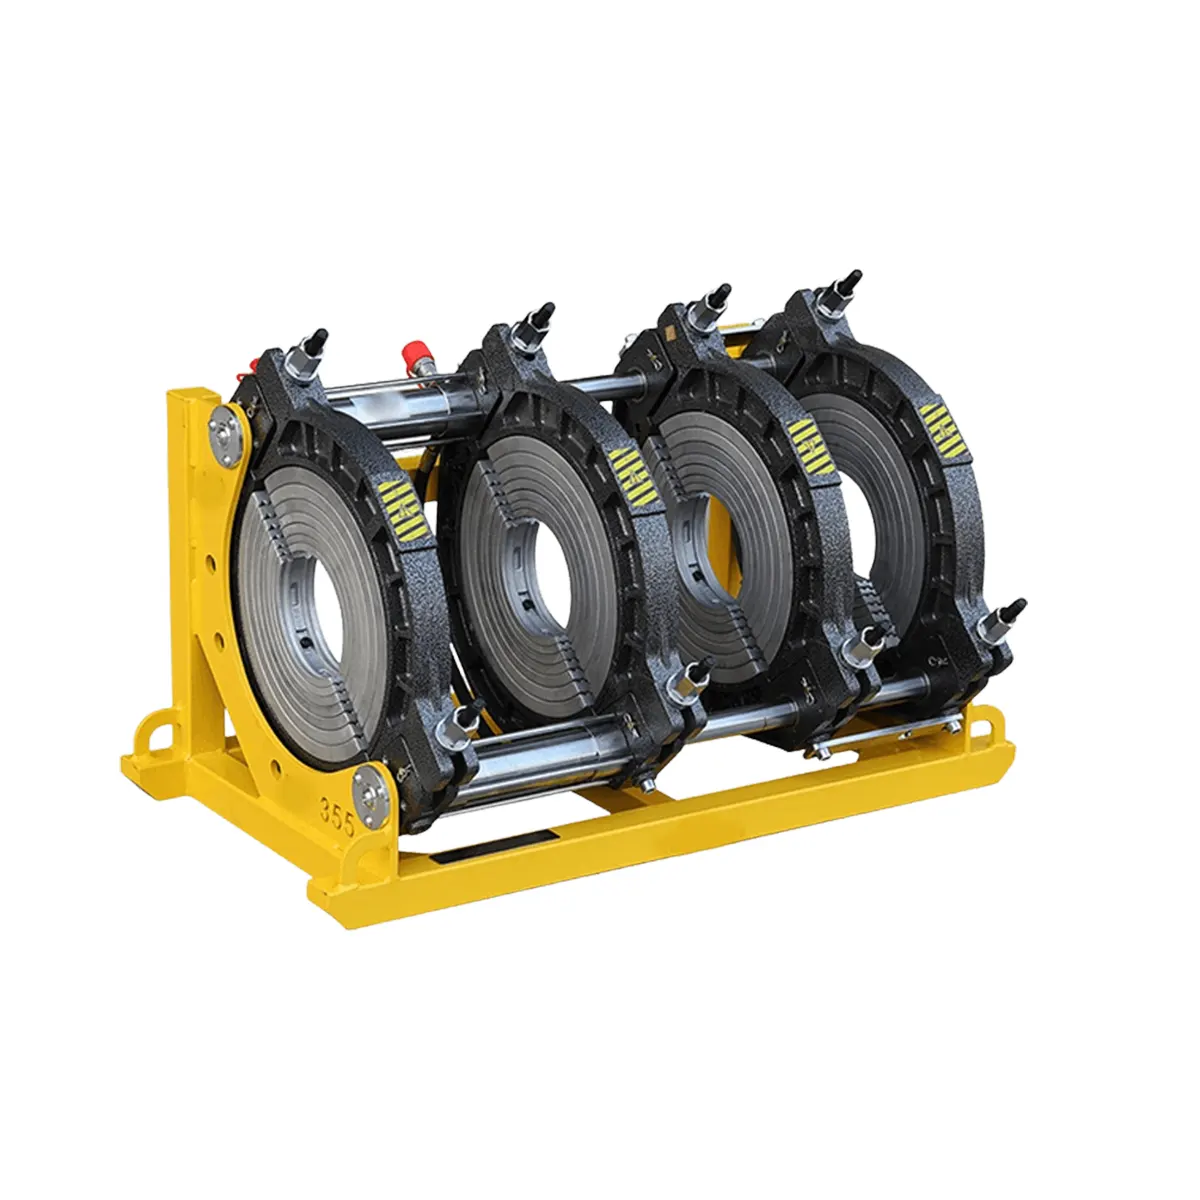
Understanding the Butt Fusion Process
Butt fusion welding is a thermofusion technique that joins the ends of two polyethylene (PE) pipes by heating them to a molten state and then pressing them together under a controlled force. Unlike mechanical joints, a properly executed butt fusion weld creates a monolithic, homogeneous bond that is actually stronger than the pipe itself. The procedure strictly follows standards like ISO 21307 butt fusion procedures, ensuring repeatability and safety across global pipeline networks.
Types of Butt Fusion Machines
Choosing the correct machine type depends on your specific job site requirements and pipe diameters. The three primary categories in the market are manual, hydraulic, and CNC automatic machines. Below is a breakdown to help you identify the best fit for your workflow:
| Machine Type | Operating Principle | Best Applications |
|---|---|---|
| Manual Butt Fusion | Hand-lever pressure application | Small diameters (≤315mm), rural water lines, tight spaces |
| Hydraulic Butt Fusion | Hydraulic power unit for force control | Medium to large diameters, consistent high-force requirements |
| CNC Automatic | Programmable logic control and data logging | Critical gas and water mains, heavy-duty industrial usage |
Key Features to Evaluate Before Buying
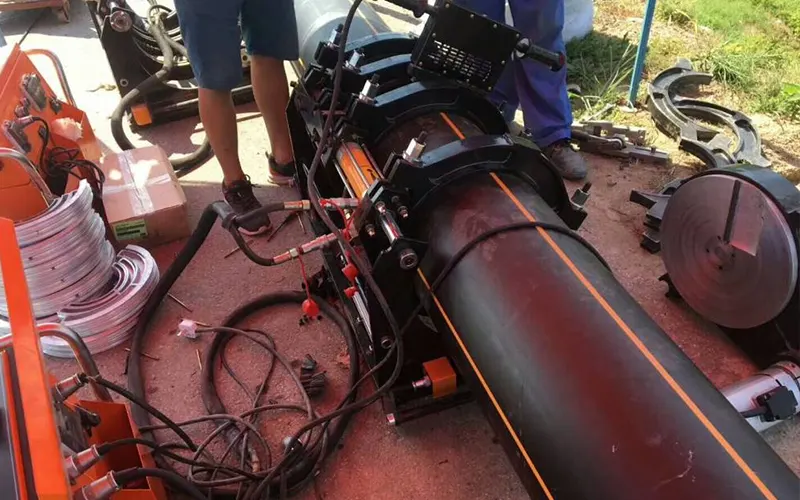
Not all fusion equipment is created equal. When specifying a butt fusion machine for pipeline construction, you must assess several structural and functional components to ensure compliance with the PE butt fusion equipment standard. Pay close attention to these areas:
- Clamping System: The clamps must hold the pipes rigidly without slippage. Hydraulic models often feature a guide-rail chassis for precise alignment during the final fusion phase.
- Trimmer Performance: A dual-blade rotary trimmer ensures perfectly flat pipe ends. The trimmer should be robust and resistant to warping under heavy use, ensuring a smooth interface.
- Heating Plate Quality: The heart of the machine. Look for a non-stick coated (PTFE) plate with even surface temperature distribution and a precise digital controller to avoid thermal degradation of the PE material.
- Pressure Regulation: Hydraulic units must deliver steady, measurable pressure. The ability to calculate and set interfacial pressure based on pipe diameter (drag pressure compensation) is vital.
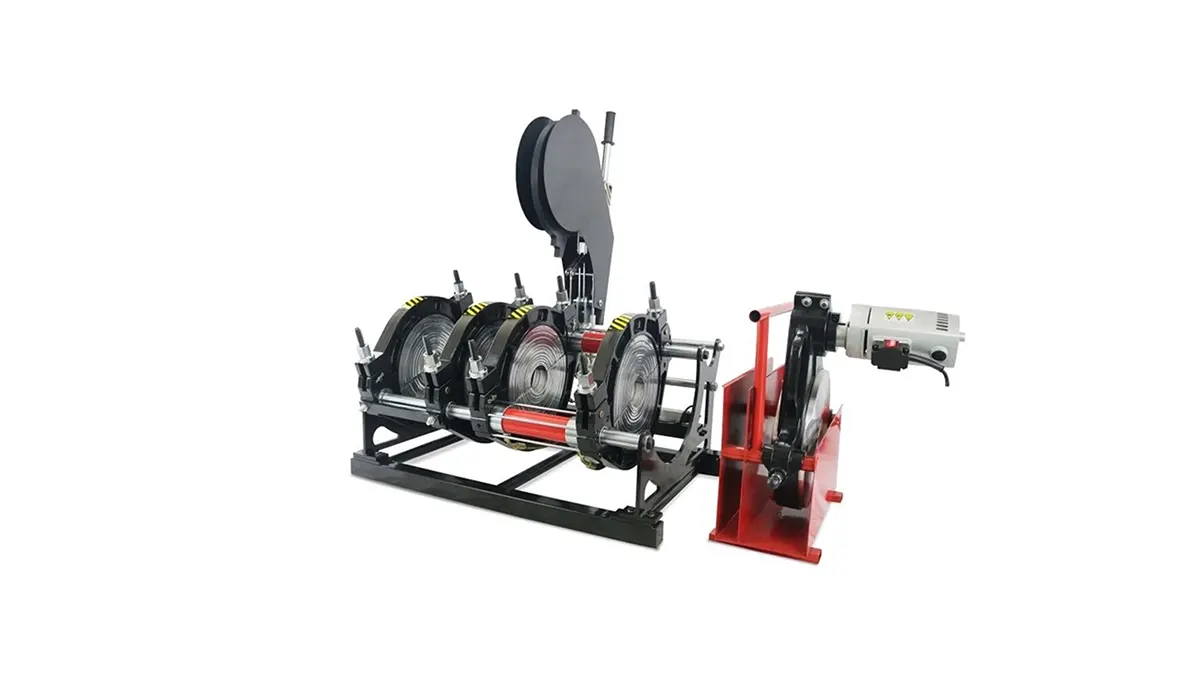
Step-by-Step Operational Guide
Mastering the operation of a butt fusion machine requires strict adherence to the PPI butt fusion procedure. Skipping steps or rushing the process can lead to cold joints or oxidation that compromise pipeline safety. Here is the standard sequence:
1. Preparation and Cleaning
Inspect the pipe ends for damage. Clean the pipe interior and exterior thoroughly. The fusion area must be free of dirt, grease, and moisture. Install the appropriate reducer inserts into the clamps to match the pipe diameter.
2. Clamping and Facing
Secure the pipes in the machine frame, leaving a small gap for facing. Engage the trimmer and bring the pipe ends together under steady pressure. Continue facing until a continuous ribbon of material is removed from both ends, confirming full contact.
3. Heating Phase
Check the heating plate temperature (typically around 400°F to 450°F / 200°C to 230°C). Place the plate between the faced pipe ends. Apply the specified initial bead-up pressure until a uniform melt bead forms around the circumference, then reduce to the soak pressure as outlined in ASTM F2620 heat fusion guidelines.
4. Switch and Fusing
This is the critical moment. Quickly remove the heating plate and inspect the melt surfaces (no contamination, no cavities). Immediately close the carriage and build up to the full fusion pressure. Hold this pressure constant during the cooling phase.
5. Cooling Under Pressure
Do not remove the pipes before the specified cooling time has elapsed. Releasing pressure too early will weaken the joint. Monitor the bead geometry; a uniform double rollback bead indicates a successful weld.
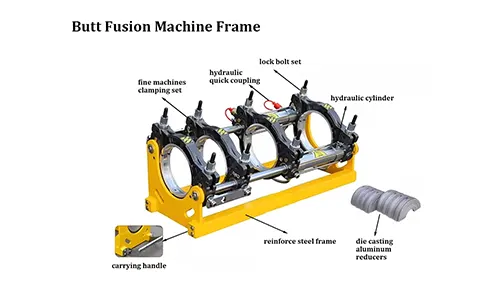
Comparing Manual vs. Hydraulic vs. Automatic
Your choice between a manual and automated system determines your job site efficiency. While a manual machine is cost-effective for small-scale irrigation, large-diameter municipal projects benefit significantly from hydraulic stability. To summarize the differences:
| Feature | Manual Machine | Hydraulic/CNC Machine |
|---|---|---|
| Force Application | Operator-dependent lever | Programmable hydraulic force |
| Data Logging | Manual chart recording | Automatic USB/Cloud data storage |
| Pipe Range | Up to 315mm typically | Up to 2500mm or larger |
Essential Maintenance and Safety Protocols
Regular maintenance of your fusion tooling is non-negotiable for passing field audits. The heating plate must be checked daily with a pyrometer to ensure temperature uniformity. The trimmer blades should be sharpened or replaced to prevent damage to the pipe skin. Always adhere to the safety requirements found in the PE fusion operator requirements.
- Always wear thermal-resistant gloves when handling the heating plate.
- Ensure the machine frame is grounded if using an electric hydraulic pump.
- Keep the non-stick coating on the plate free from scratches and plastic residue.
- Calibrate pressure gauges annually to maintain fusion pressure accuracy.
Why Trust JQ-Fusion for Your Pipeline Needs?
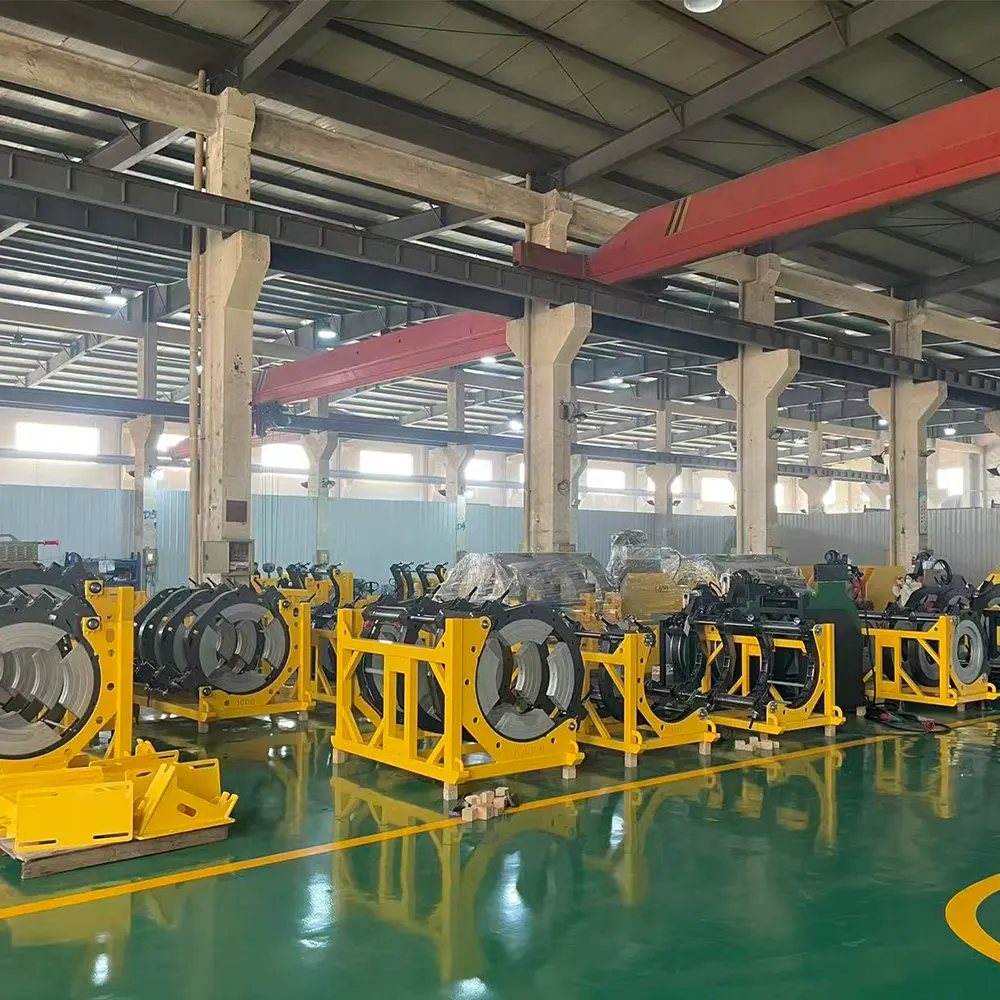
Selecting a reliable manufacturing partner is just as important as choosing the right machine. JQ-Fusion stands out as a professional manufacturer dedicated solely to high-performance HDPE pipe welding solutions. Unlike general equipment suppliers, JQ-Fusion offers deep technical expertise, from selecting the correct hydraulic butt fusion machine to providing ongoing after-sales guidance. Their extensive in-stock inventory guarantees that your urgent project deadlines are met without the typical manufacturing lead time delays.
Key Specifications to Check in a Datasheet
When reviewing catalogs, focus on the technical specifications that directly affect the welding integrity. The table below highlights critical parameters you should verify before issuing a purchase order for a pipeline construction project:
| Parameter | Why It Matters |
|---|---|
| Operating Voltage | Must match on-site generators or grid power without fluctuation. |
| Clamping Range | Confirm the minimum and maximum OD capacity, including SDR variations. |
| Trimmer Torque | Insufficient torque leads to rough facing on thick-walled pressure pipes. |
| Certification | Look for compliance with ISO 4427 PE water pipes and gas distribution codes. |
Final Thoughts on Machine Selection
Investing in a high-quality butt fusion machine for pipeline construction is an investment in the lifespan of your entire network. By thoroughly evaluating the machine’s clamp rigidity, heating stability, and compliance with the PPI technical guidance, you can avoid costly repairs and system failures in the future. Remember to always align your equipment choice with the specific SDR and material grade of the pipes you are joining. A properly fused polyethylene pipeline is a seamless conduit that will serve infrastructure reliably for decades, provided the fusion is done right the first time.



