
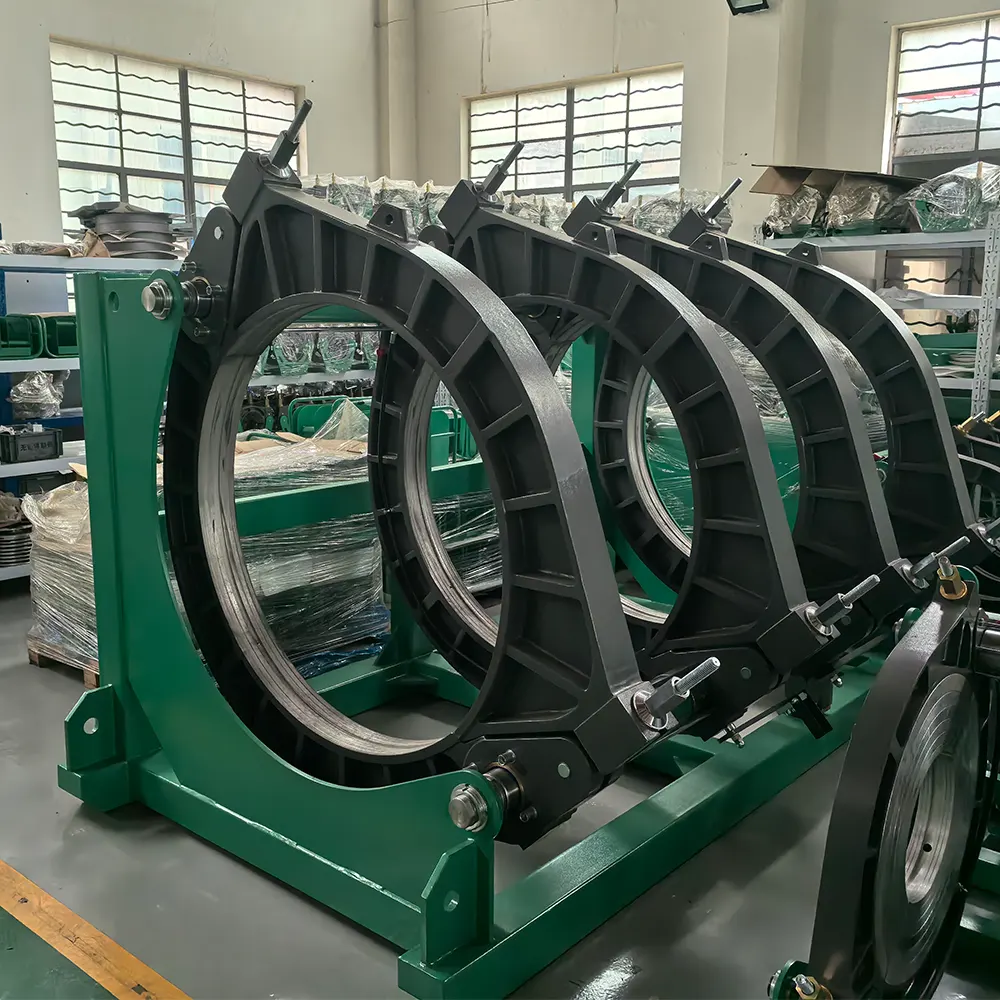
PE80 pipe butt fusion is the most widely adopted joining method for medium-density polyethylene piping systems in gas distribution and water supply networks worldwide. This guide covers every aspect — from material understanding to field execution.
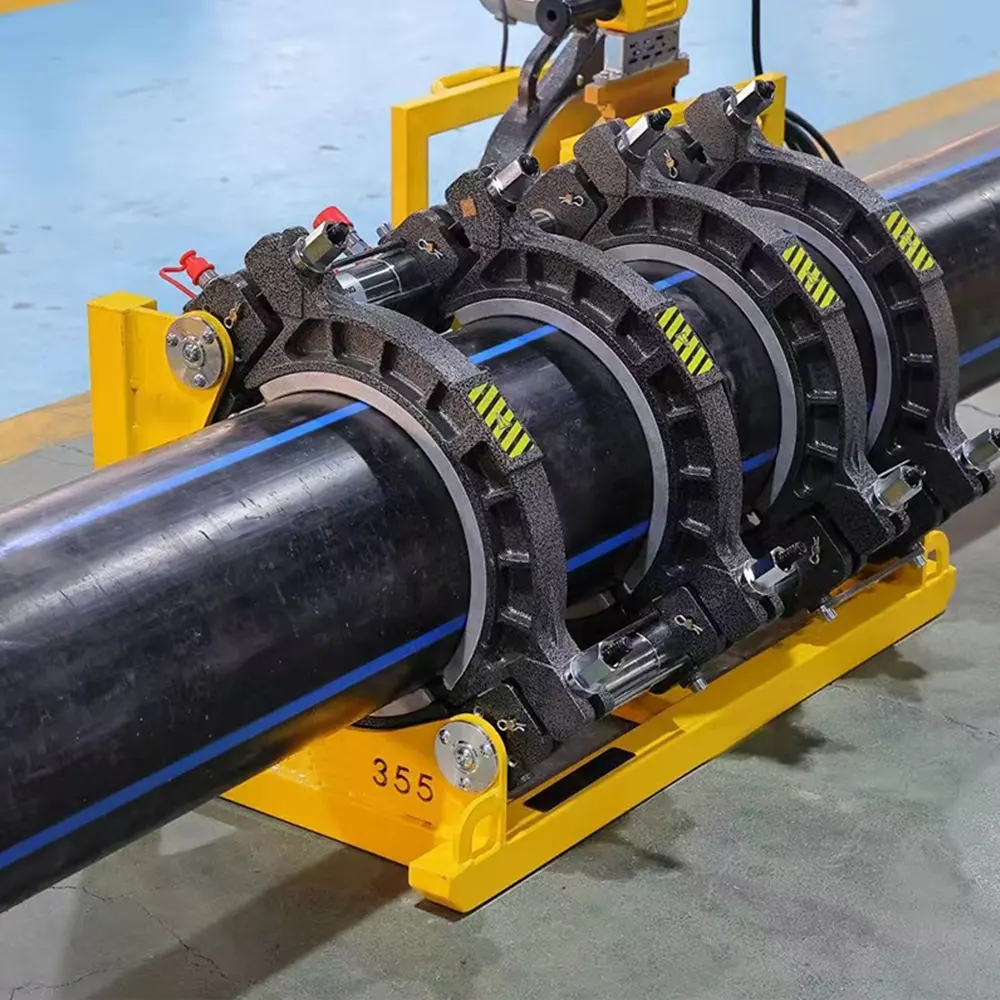
Understanding the PE80 Material
PE80 is a medium-density polyethylene grade with a minimum required strength (MRS) of 8.0 MPa. It offers an excellent balance of flexibility, chemical resistance, and long-term durability. Compared to PE100, PE80 pipes have a slightly thicker wall for the same pressure rating, making them a proven choice for low to medium pressure applications. When preparing for PE80 pipe butt fusion, understanding the material’s melt flow characteristics and oxidation induction time is essential for parameter selection.
Essential Butt Fusion Equipment
Proper equipment is the foundation of every successful butt fusion welding machines joint. For PE80 pipes, the basic setup includes the fusion machine frame, a facing tool (trimmer), a heating plate with controlled temperature, and a hydraulic power unit for larger diameters.
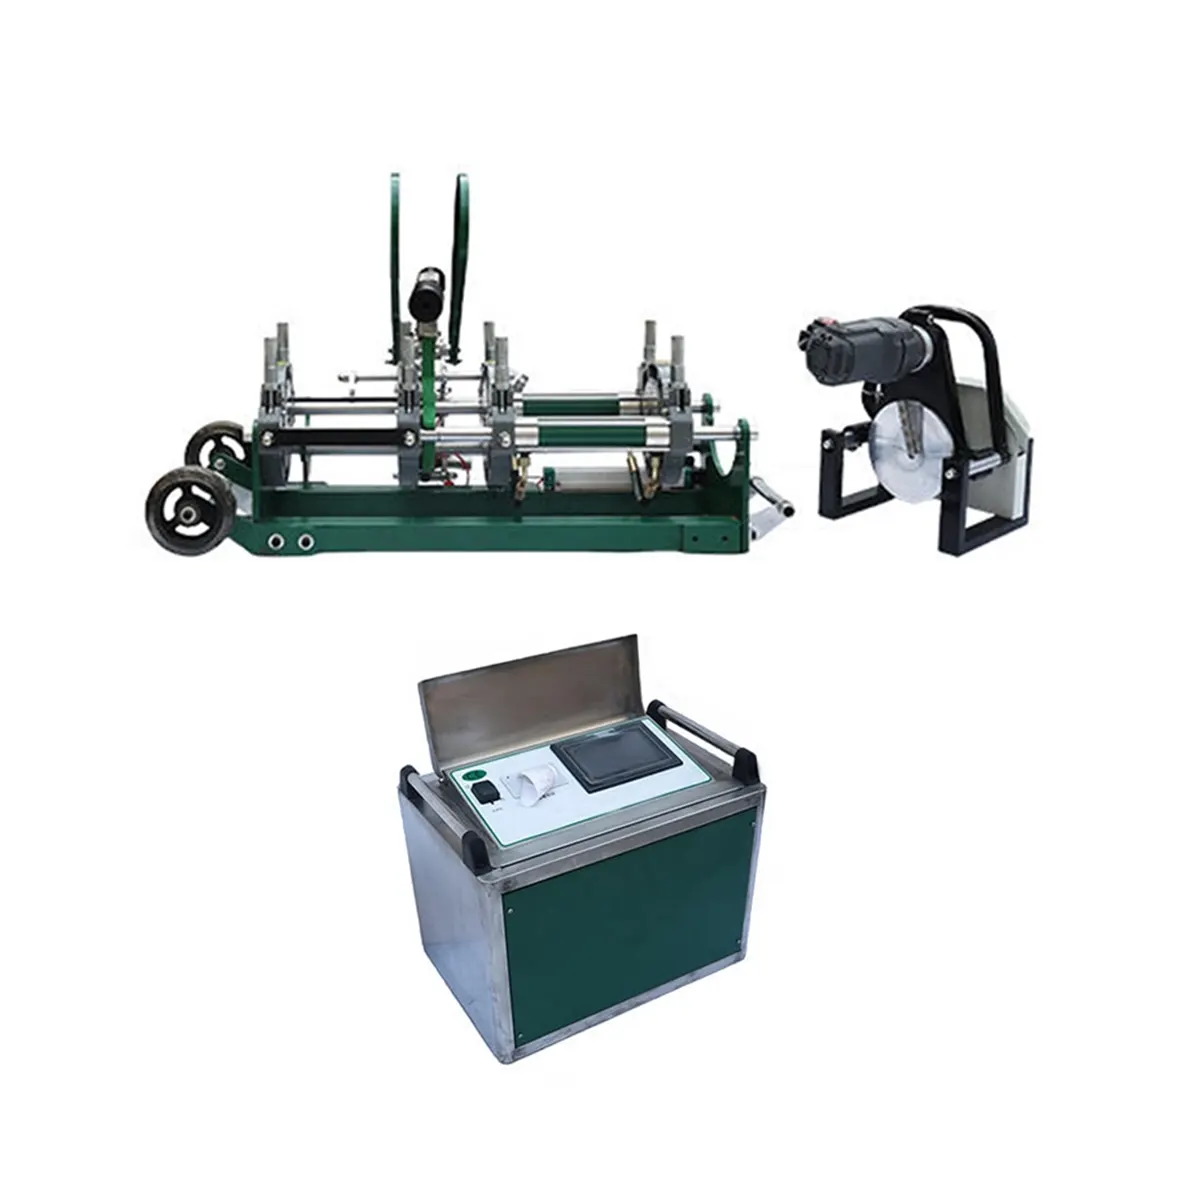
Automatic Butt Fusion Machine
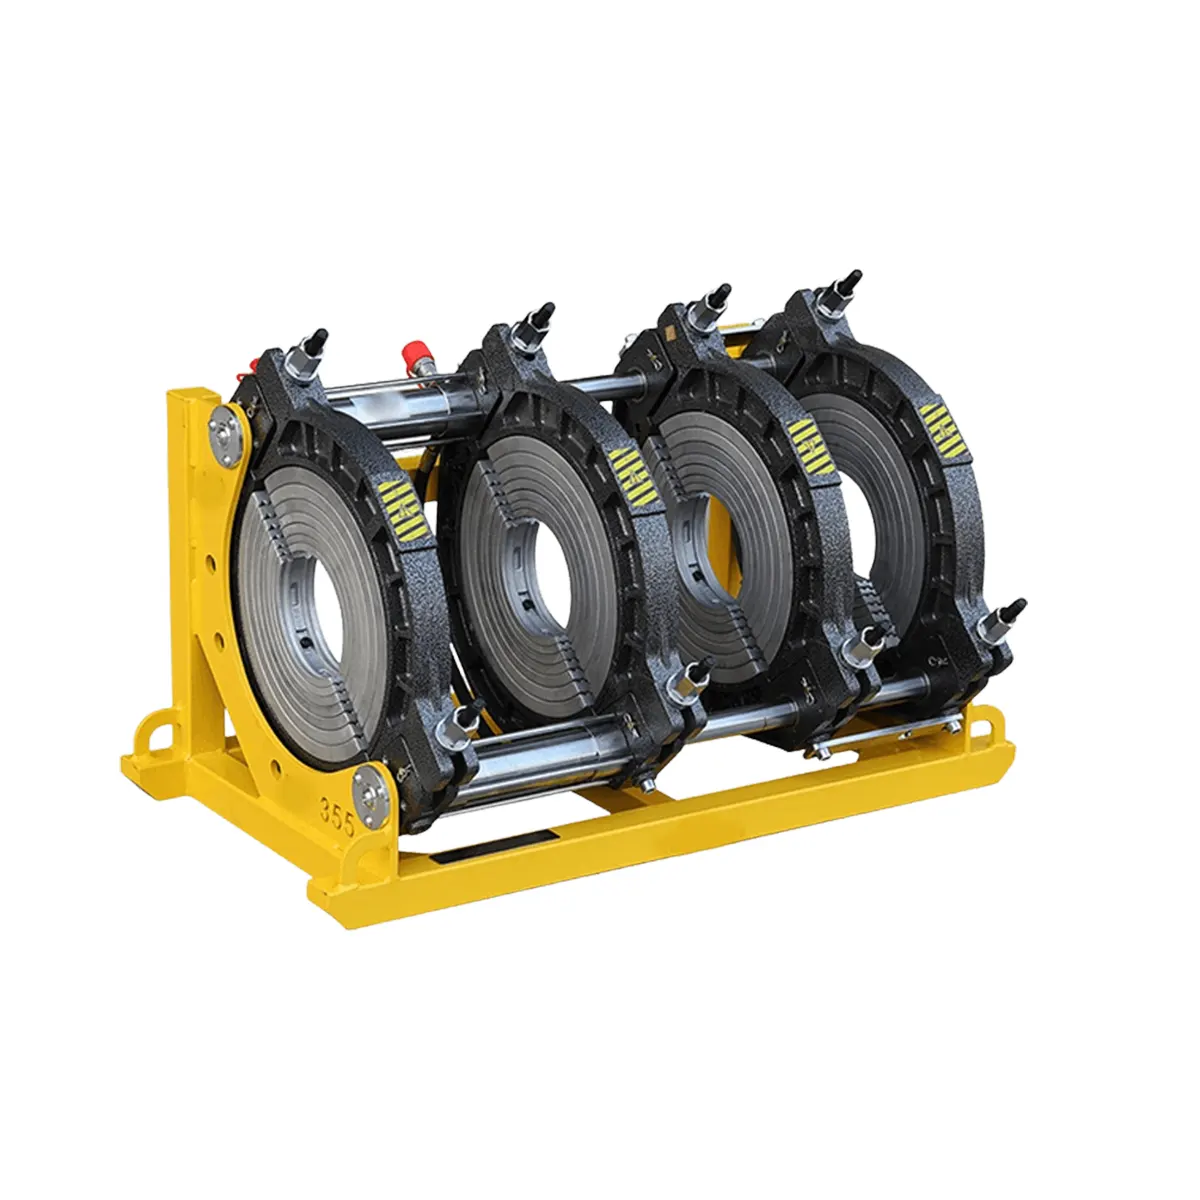
Hydraulic Powered Unit for Large Diameters
Heating Plate Requirements
The heating plate must maintain a constant surface temperature between 200°C and 230°C (typically 210°C for PE80). The plate surface should be clean, non-stick coated, and checked regularly with a calibrated digital pyrometer. Uneven heat distribution leads directly to inconsistent melt bead formation and weak fusion joints.
Clamping and Alignment System
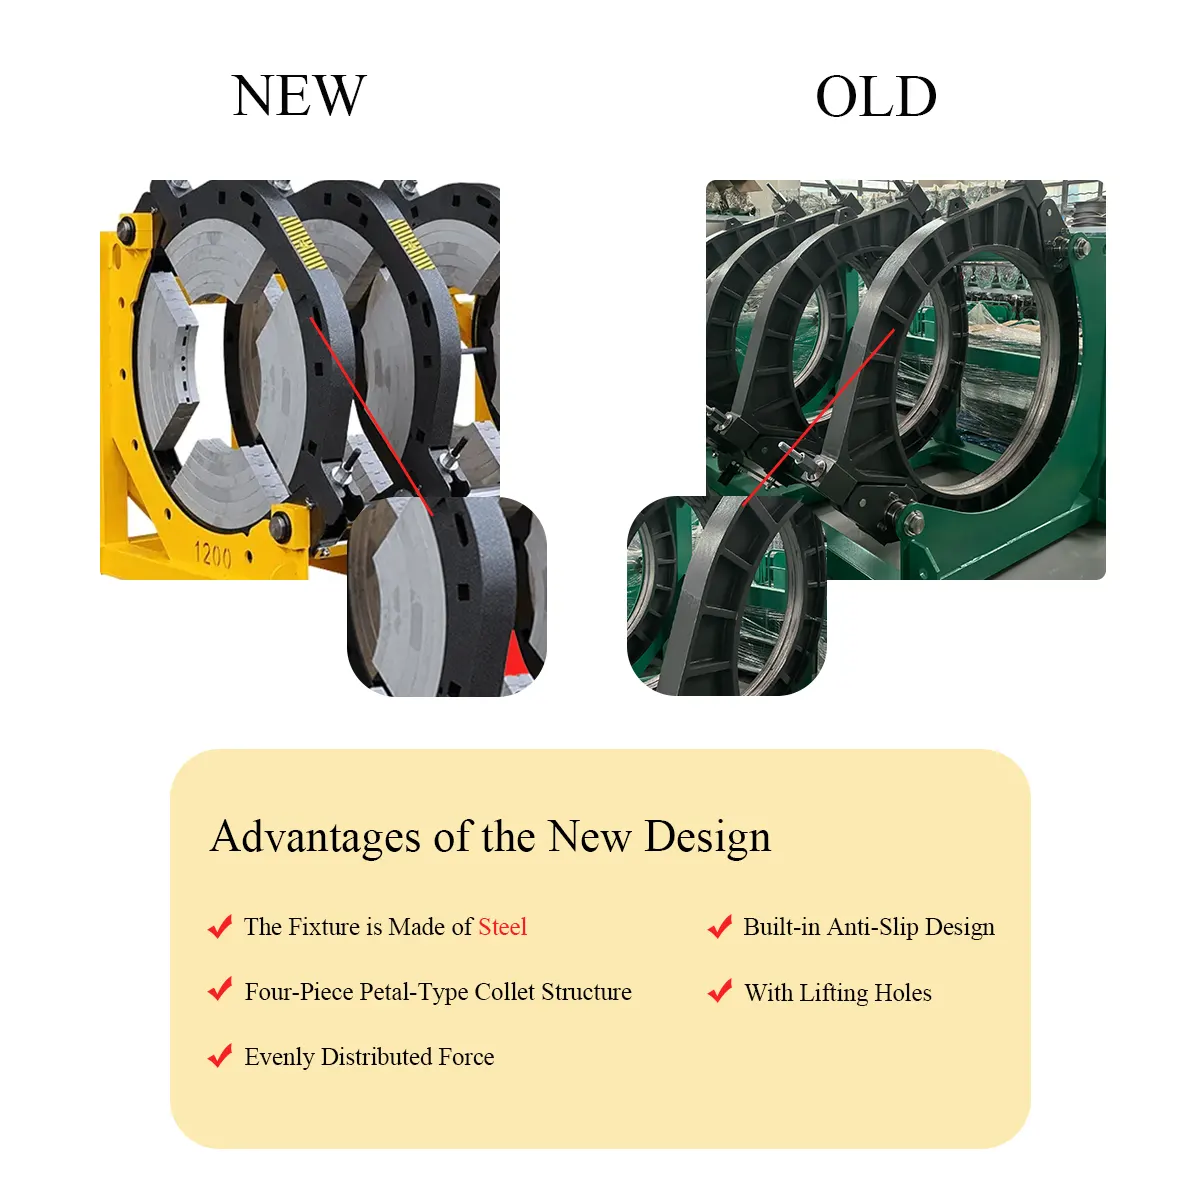
The machine clamps must hold pipes firmly without causing deformation. For PE80 pipes, the alignment tolerance between pipe ends should be less than 10% of the wall thickness. Proper alignment prevents high-low mismatch, a common cause of joint failure in buried pipelines. On Hydraulic Butt Fusion Welding Machine systems, the moveable jaw design significantly improves alignment accuracy for heavy pipe sections.
Step-by-Step Fusion Procedure
The ISO 21307 butt fusion procedures define a single low-pressure fusion protocol ideal for PE80 materials. Following the cycle strictly is non-negotiable for pipeline integrity. Independent standards like PPI TN-51 also provide detailed technical guidance on the process structure.
| Fusion Stage | Parameter | PE80 Typical Value |
|---|---|---|
| Bead-Up Phase | Interfacial Pressure | 0.15 MPa (21.7 psi) |
| Heat Soak Phase | Drag Pressure | < 0.01 MPa (minimal drag) |
| Heater Plate Removal | Maximum Dwell Time | As short as possible (3-5 seconds) |
| Fusion Joining | Build-Up Pressure | 0.15 MPa (steady increase) |
| Cooling Phase | Time Under Pressure | Based on wall thickness (see DVS/ISO tables) |
1. Pipe Preparation and Cleaning
Clean both pipe ends thoroughly with a lint-free wipe and isopropyl alcohol. Inspect for deep scratches, gouges, or UV degradation. Cut pipe ends square to the pipe axis. Any contamination — dirt, moisture, oil — will become permanently embedded in the fusion interface and cause premature failure.
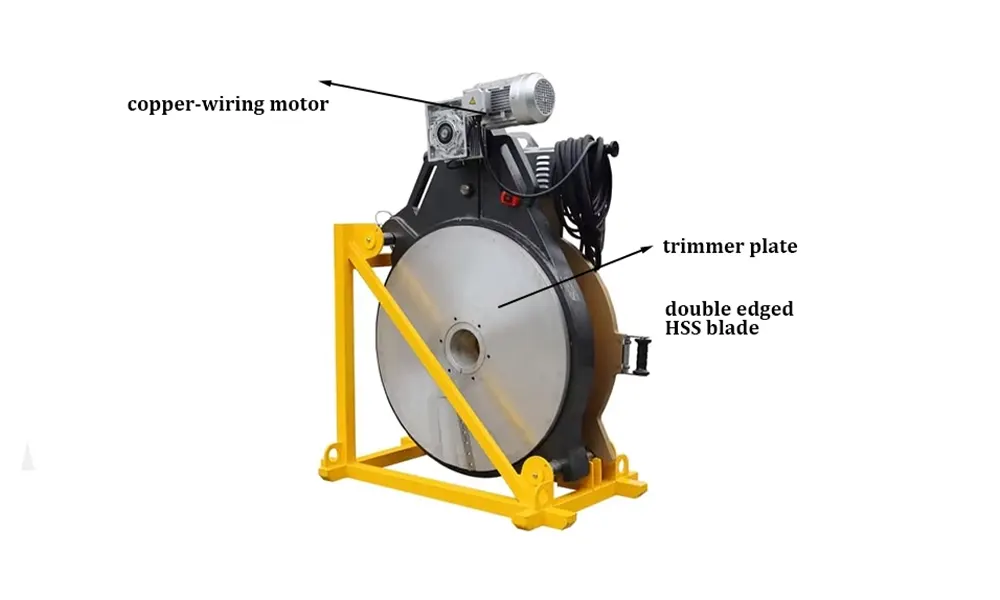
2. Facing Operation
Face the pipe ends using the machine’s rotating trimmer until a continuous thin shaving appears from both sides without gaps. The faced surfaces must be flat, parallel, and free from chatter marks. Do not touch the faced ends after trimming — even skin oils compromise fusion quality.
3. Heating Stage Management
Bring the heating plate into contact with the pipe ends at the specified bead-up pressure. Watch for a uniform melt bead to form around the entire circumference. Once the bead reaches the required height (typically 1.0 mm minimum for smaller diameters, scaling up with wall thickness), reduce pressure to the drag setting and begin the heat soak timer.
4. Heater Removal and Fusion Join
This transition must be swift and smooth. Open the carriage, remove the heater plate without scraping the melt surfaces, and close the carriage immediately. Apply the fusion pressure steadily — a double melt bead pattern should form symmetrically on both sides of the joint. The bead size and shape are your first visual quality indicators.
Quality Control and Inspection
Every PE80 pipe butt fusion joint should be visually inspected. The external bead should exhibit a symmetrical double-rollback with smooth surfaces, free from porosity, discoloration, or cracks. A destructive bend-back test or a coupon test according to relevant standards provides validation for procedure qualification.
- Bead Appearance: Twin beads of equal size, rounded and smooth, with no signs of contamination.
- Misalignment Check: Maximum offset between pipe surfaces must not exceed 10% of the wall thickness.
- Bead Width Measurement: Record bead width at multiple points around the circumference for consistency.
- Data Logging: Modern automatic machines record pressure, temperature, and time curves — review these before accepting the joint.
Common Defects and Troubleshooting
| Defect | Likely Cause | Solution |
|---|---|---|
| Small or uneven bead | Insufficient heat soak time or low temperature | Verify heater surface temperature; increase heat soak duration |
| Porous or discolored bead | Moisture contamination or overheating | Dry pipe ends thoroughly; check heater thermostat accuracy |
| High-low mismatch | Pipe ovality or clamp misalignment | Use alignment clamps; re-round pipe ends if necessary |
| Incomplete fusion interface | Oxidized melt surface (slow plate removal) | Reduce dwell time; ensure clean heater plate surface |
Environmental Conditions and Their Impact
PE80 butt fusion is sensitive to ambient conditions. Wind, rain, dust, and extreme cold all affect the fusion process. Fusion shelters or tents are mandatory for field work in adverse weather. Below 5°C, pre-heating the pipe ends or adjusting heat soak times becomes necessary. In hot, sunny climates, protect pipe ends from direct solar heating to prevent uneven temperature profiles before fusion.
Applications of PE80 Butt Fusion Joints
- Gas Distribution Networks: PE80 remains a standard material for natural gas and LPG distribution lines up to 4 bar operating pressure. Butt fusion provides the fully restrained, leak-tight joints these systems demand.
- Water Supply and Irrigation: Municipal water mains and agricultural irrigation systems benefit from PE80’s corrosion resistance and the monolithic joint integrity created by proper fusion.
- Industrial Slurry and Chemical Lines: PE80’s chemical resistance combined with butt fusion’s smooth internal bore makes these piping systems ideal for mining slurries and chemical transfer applications.
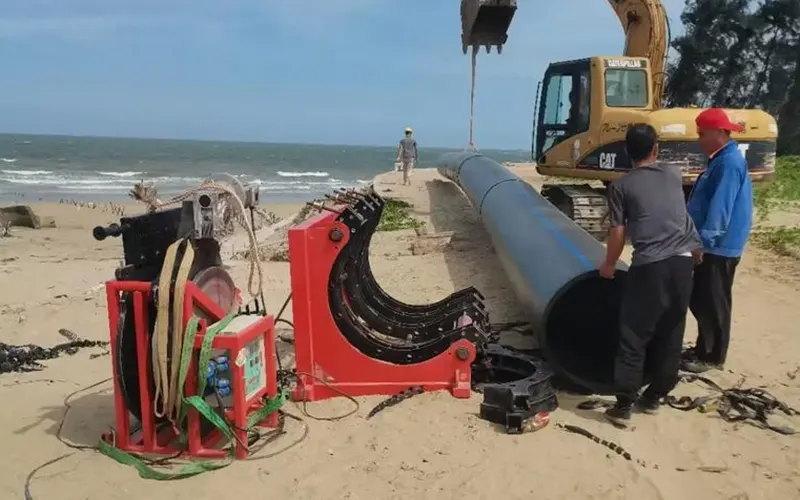
- Marine Outfall and Intake Lines: Long strings of PE80 pipe can be butt fused on shore and floated into position, taking advantage of the material’s flexibility and the joint’s full strength.
Choosing the Right Machine for PE80 Projects
Machine selection depends on the diameter range and project conditions. For small diameters up to 160 mm, Manual Butt Fusion Welding Machine units provide a cost-effective solution with hand-operated clamping. For mid-range diameters (200 mm to 630 mm), hydraulic machines offer the consistent pressure control needed for successful PE80 fusion. Projects involving larger diameters or high production rates benefit from CNC Automatic Butt Fusion Welding Machines that log every joint parameter for traceability.
Companies like JQ-Fusion supply a comprehensive range of fusion equipment including hydraulic, automatic, and manual machines suitable for PE80 piping projects of any scale. Equipment designed to meet international standards ensures that your fusion procedures remain compliant and repeatable across all project phases.
Operator Training and Qualification
Even the best PE80 pipe butt fusion equipment cannot compensate for an untrained operator. Operators should be qualified according to national standards such as those referenced by ISO 12176-3 or the Plastics Pipe Institute guidelines. Regular requalification and procedure demonstrations on destructively tested samples are industry best practices.
Data Recording and Traceability
Modern automatic machines generate detailed fusion logs showing temperature, pressure, and time data for every joint. For manual and hydraulic setups, operators should maintain a written fusion record sheet noting joint number, date, ambient conditions, machine ID, and operator name. Traceability is increasingly required by utility owners and regulatory agencies for critical PE80 infrastructure.
Key Takeaways for Successful PE80 Fusion
- Always verify the heater plate surface temperature with a calibrated pyrometer before starting work.
- Cleanliness is paramount — protect faced pipe ends from any contamination.
- Follow the single low-pressure fusion procedure parameters precisely for PE80 grade material.
- Inspect every joint visually and document the bead appearance before lowering into the trench.
- Protect the fusion work area from adverse weather with temporary shelters.
- Use equipment sized correctly for your pipe diameter range — undersized machines cause alignment problems.
For complex projects or technical inquiries regarding PE80 pipe butt fusion equipment selection, consult with manufacturers who can offer guidance based on your specific application requirements. The right combination of material knowledge, procedural discipline, and reliable equipment ensures fusion joints that last for the design life of the pipeline system.



