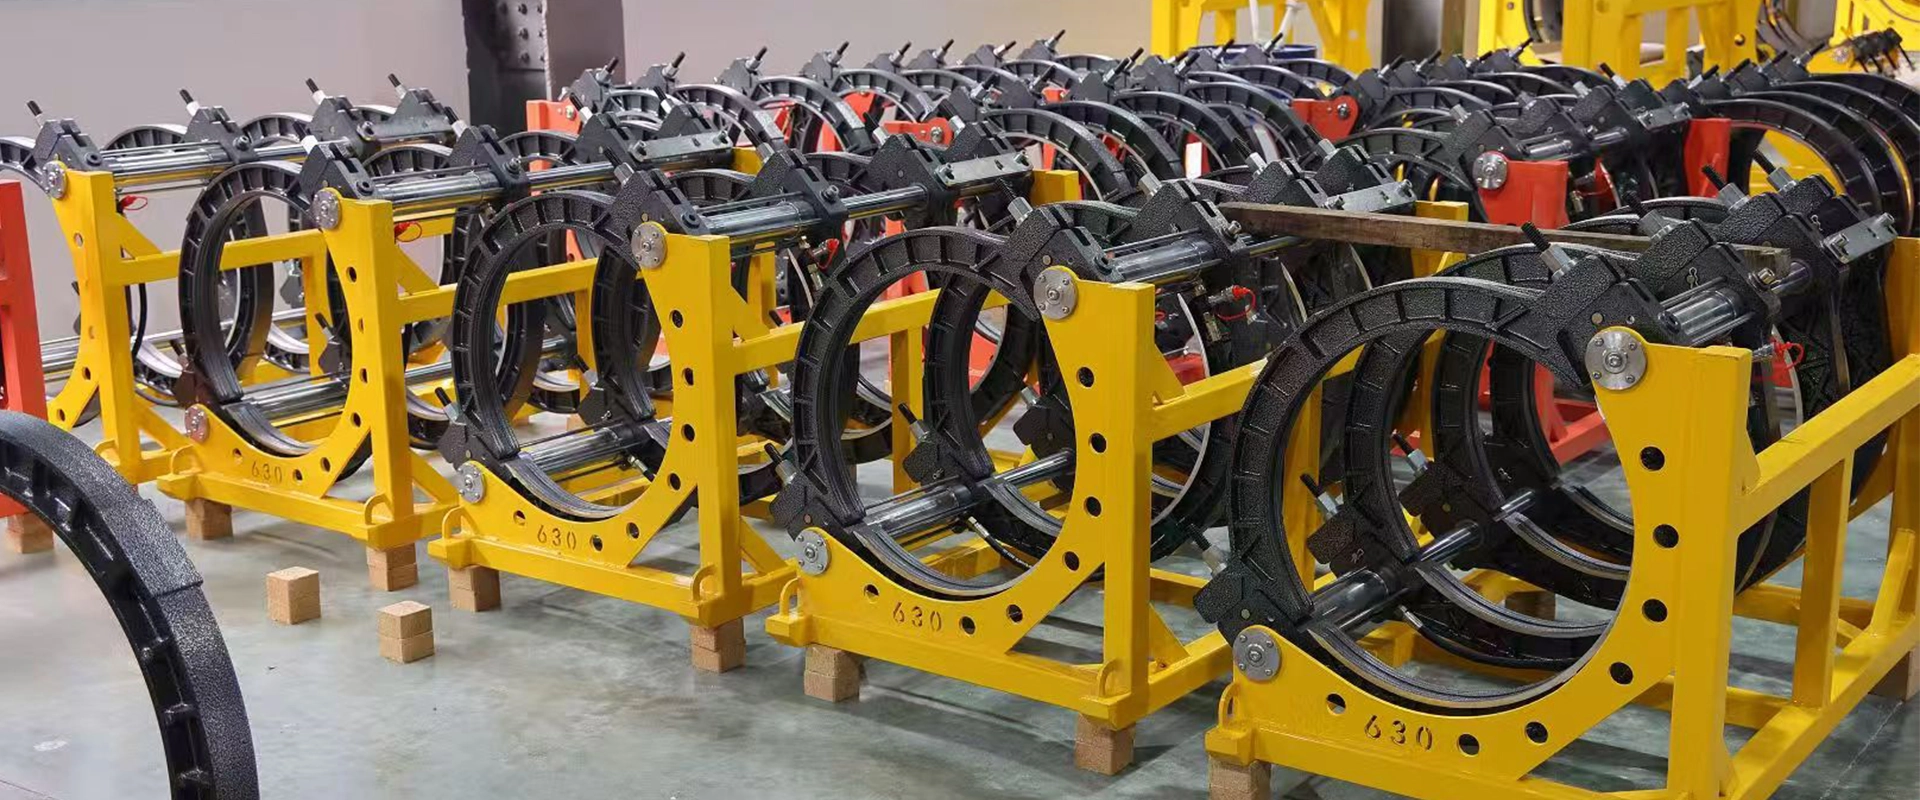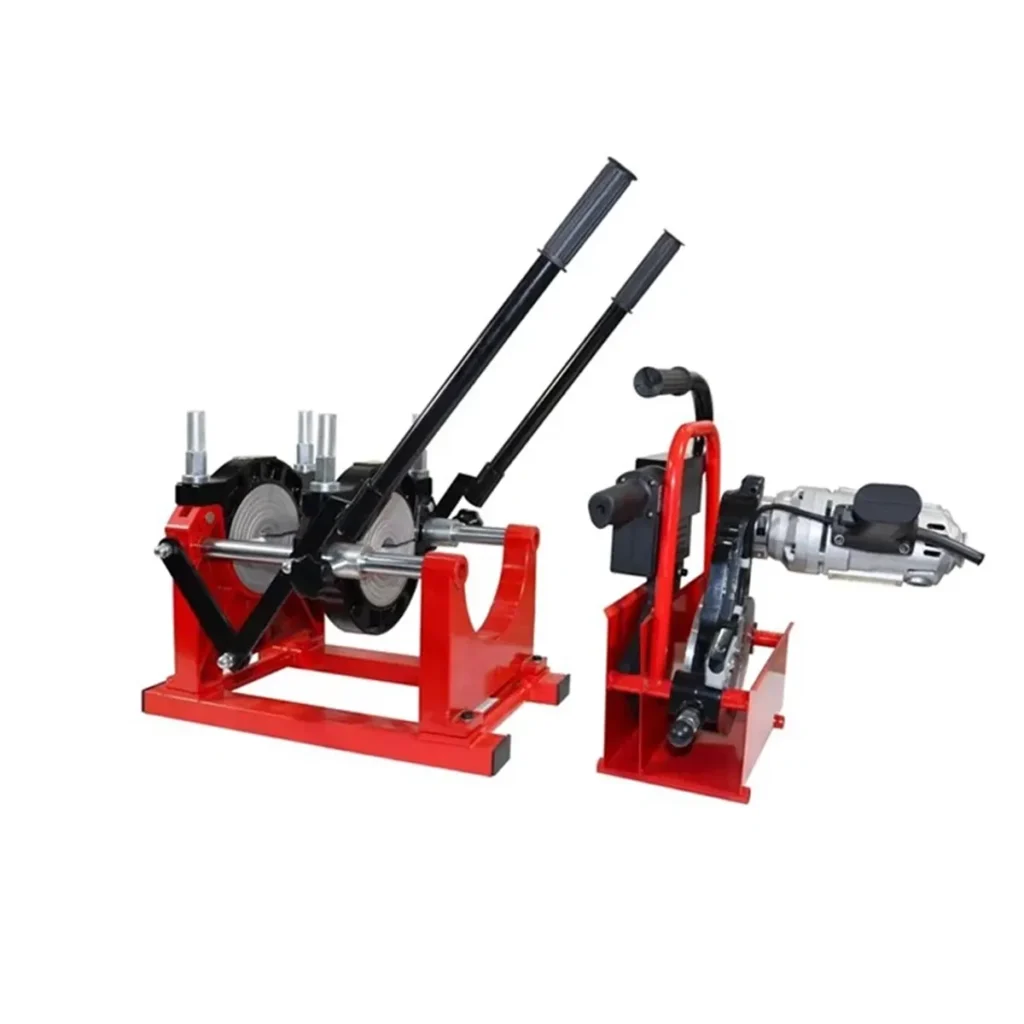
Even the most robust plastic pipe welding machine can encounter operational hiccups. Effective troubleshooting is critical not only for minimizing downtime on the job site but also for ensuring joint integrity according to standards like ISO 21307 butt fusion procedures. Whether you are working with a manual rig or a fully automatic system, identifying the root cause of a bad fusion is the first step to fixing it. This guide walks you through the most frequent issues, their underlying causes, and the step-by-step solutions to get your butt fusion equipment back on track.
1. Uneven or Incomplete Bead Formation
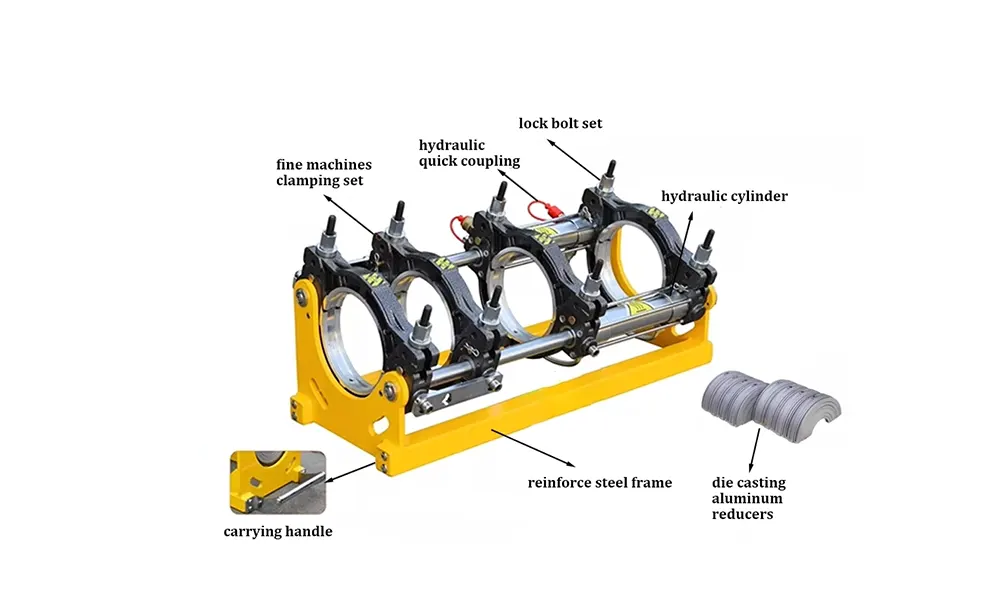
The appearance of the melt bead is the most immediate visual indicator of a successful weld. A uniform, symmetrical bead roll indicates correct pressure and temperature parameters were met. If your bead is irregular, the joint is structurally compromised.
| Symptom | Potential Cause | Solution |
|---|---|---|
| Small, flat bead on one side | Misaligned pipe ends or clamp slippage | Re-adjust clamps; ensure both pipe ends are perfectly cylindrical and aligned before clamping. |
| Excessively large, drooping bead | Overheating or excessive fusion pressure | Verify the heating plate temperature with a pyrometer and reduce the drag/fusion pressure to match the pipe material specifications. |
| Brittle, shiny, or non-continuous bead | Contamination (dirt, water) or cold weld | Thoroughly clean the pipe surface and manual trimmer blades; ensure the heating temperature is within the 200-220°C range. |
2. Heating Plate Temperature Issues
The heating plate is the heart of your plastic pipe welding machine. Inconsistent surface temperature leads directly to poor intermolecular diffusion. This is a common troubleshooting point for operators working with hydraulic systems.
- Temperature Too Low: If the plate doesn’t reach the set point, check the continuity of the heating element with a multimeter. A burned-out coil will result in a “cold spot.” Immediately replace the defective element.
- Temperature Overshoot: If the temperature swings wildly above the set limit, the thermostat or internal relay is likely faulty. This can oxidize the PE material instantly. Replace the temperature controller board.
- Surface Condition: Burnt polymer residue acts as an insulator. Never scrape the non-stick coating with metal tools. Use a clean, lint-free cloth while the plate is hot to wipe away residue.
3. Hydraulic System Malfunctions (Hydraulic Machines)
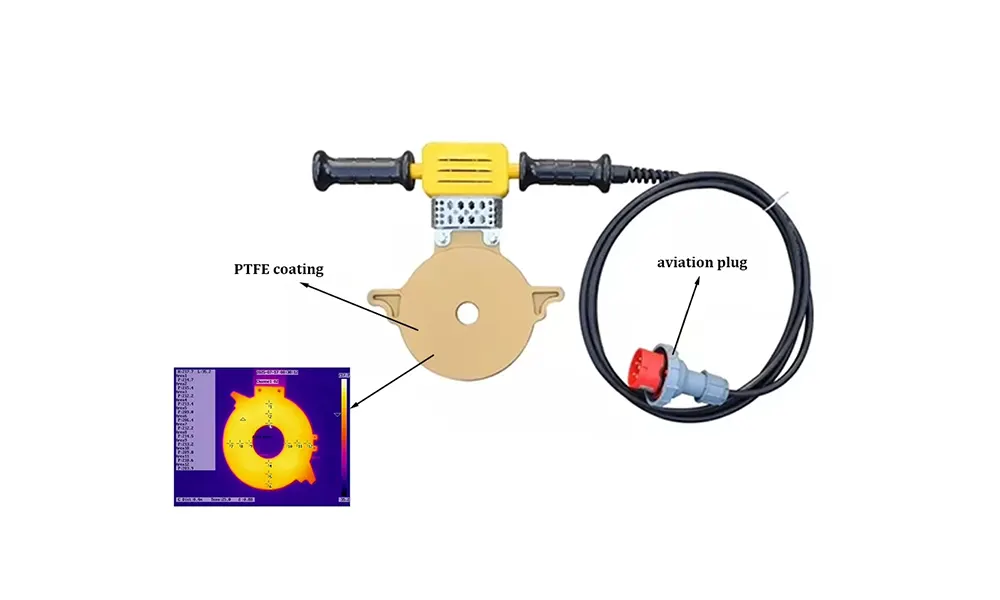
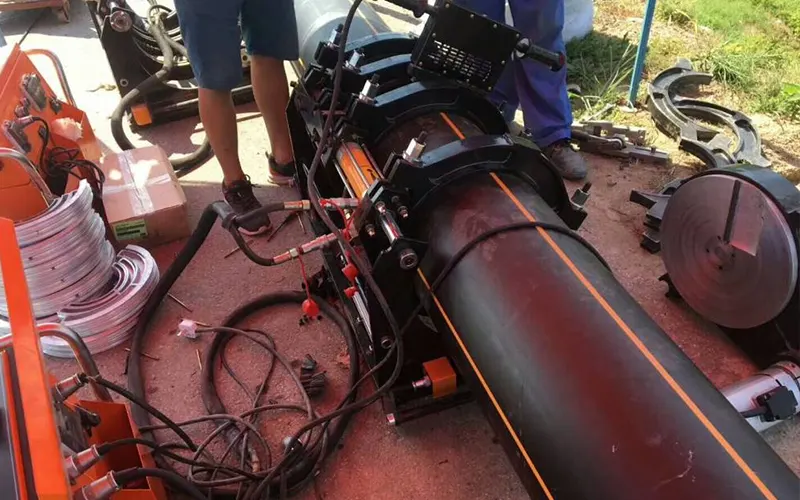
For large-diameter projects using a hydraulic plastic pipe welding machine, stalling or jerky movement is a common headache. This involves the power pack and cylinders.
3.1 No Pressure Build-Up
If the machine cannot reach the required fusion pressure (as calculated by the DVS/ISO standards), inspect the emergency stop button first—it’s often accidentally engaged. Next, check the hydraulic fluid level. Low fluid introduces air into the system, causing spongy movement. Finally, check the pressure relief valve; vibration can cause it to loosen and bleed off pressure.
3.2 Jerky Cylinder Movement
Stuttering movement during the critical cooling phase usually indicates air in the hydraulic circuit. You must bleed the cylinders by running them full-cycle without load several times. A blocked suction filter in the hydraulic tank can also cause cavitation, damaging the pump.
4. Trimmer (Facing Tool) Problems
Proper facing is non-negotiable. The ends must be parallel and free of oxidized material. Problems with the facing tool create a gap that prevents even pressure distribution. Always refer to the PE butt fusion equipment standard for facing requirements.
| Issue | Diagnosis | Repair Action |
|---|---|---|
| Uneven shaving thickness | Dull or chipped blades | Replace both blades simultaneously. Ensure they are secured tightly with no vibration. |
| Pipe ends not square (gap check fails) | Loose trimmer bearings or bent shaft | Replace the bearing assembly. Never drop the trimmer onto hard surfaces. |
| Motor hums but blades don’t spin | Sheared drive key or capacitor failure | Check the starting capacitor in single-phase motors; replace the mechanical key on the gear shaft. |
5. Electrical and Control System Faults (CNC Automatic Machines)
Advanced plastic pipe welding machine models with CNC automatic controls might report error codes or fail to initiate the cycle. These logic-controlled systems are precise but sensitive to input errors.
- Faulty Limit Switches: Automatic stages won’t advance if the control doesn’t sense the part is “home.” Test micro-switches for continuity. Dust and plastic shavings often block the switch’s physical actuator.
- Data Logging Errors: If the machine refuses to start the fusion cycle, verify that the mandatory input fields (pipe diameter, SDR, drag pressure) are not set to zero. Inconsistent data entry is the most frequent “error” in automated operations.
- Emergency Stop Loop: A broken wire in the E-Stop loop will kill all outputs. If removing the lock is an option, bypass the switches temporarily with a jumper to identify the faulty contact, but never operate permanently without them.
6. Clamping and Alignment Challenges
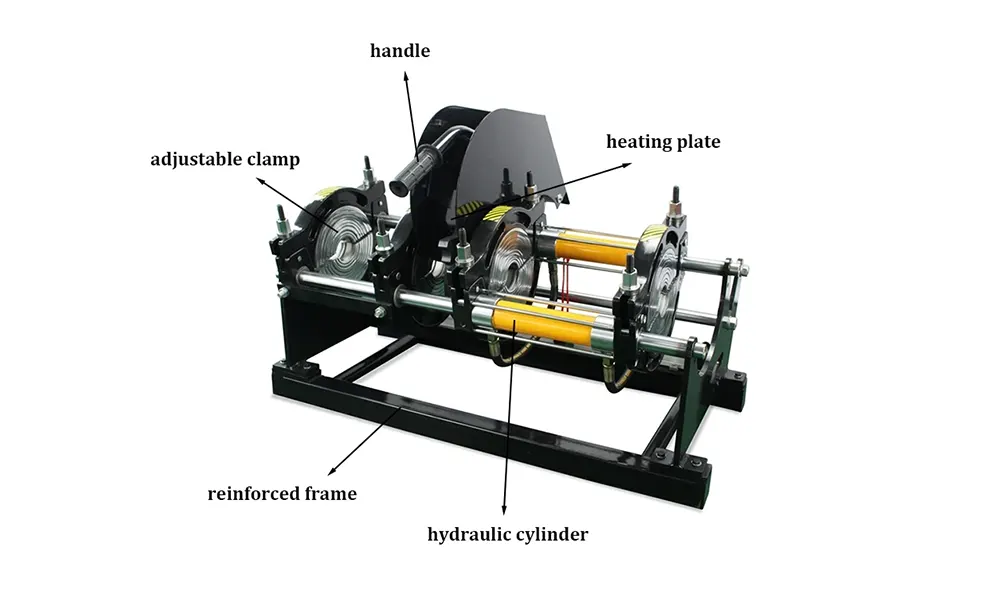
High axial forces during fusion can cause the pipe to slip, resulting in an immediate failure. This is particularly problematic in smaller plastic pipe welding machine frames with manual clamps.
Check the jaw inserts: Worn-out inserts will not grip the pipe effectively. Clean any oil or grease from the pipe surface and the jaws. For ovalized pipes (common in large coils), use re-rounding clamps as an accessory. The number one rule is never to tighten a clamp against a round pipe out of alignment; it will deform the frame.
In cases where persistent slippage or frame deformation occurs, evaluating the build quality of the equipment is crucial. At JQ-Fusion, our philosophy centers on rigid, high-tensile steel frames that prevent the flex often seen in lighter machines, ensuring your alignment stays true from setup to cooling. You can explore our support resources for detailed frame adjustment guides.
Preventive Maintenance Checklist
Prevention is better than a cure, especially in the field. Integrate these checks into your daily routine to avoid needing extensive plastic pipe welding machine troubleshooting:
- Daily: Clean PTFE heating plate surfaces and check blade sharpness.
- Weekly: Grease all nipples on the slide rails and ball screws (use lithium-based grease).
- Monthly: Test actual temperature vs. displayed temperature with a calibrated probe.
- Quarterly: Change hydraulic oil filter and check for water contamination in the fluid.
For in-depth guidance on fusion operator qualifications and safe practices, we recommend reviewing the ASTM F2620 heat fusion standard before starting any critical project.