
Selecting the right HDPE pipe welding machine is critical for ensuring pipeline integrity in water, gas, and industrial applications. A poorly chosen machine leads to weak joints, project delays, and increased costs. This HDPE pipe welding machine selection guide provides a structured approach to matching equipment with your specific pipe diameter, wall thickness, and job site conditions, helping you achieve consistent, high-quality fusion welds every time.
1. Understand Your Application and Pipe Specifications
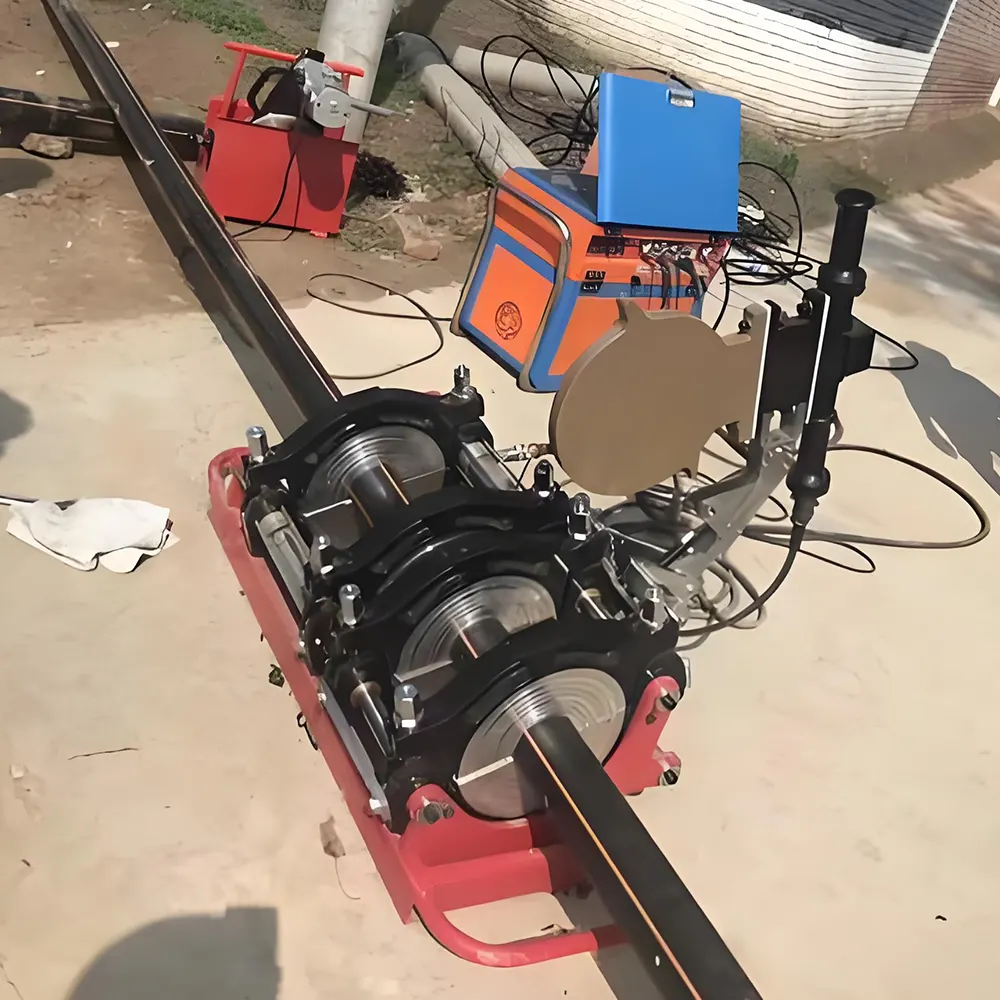
Defining your project requirements is the first step in the machine selection process. The diameter range and wall thickness of the HDPE pipes you work with directly determine the machine category and clamping force needed. A contractor upgrading municipal water mains has vastly different needs than a technician installing gas distribution lines. You must also consider the working environment—confined trenches, open fields, or high-altitude locations all influence the choice of manual, hydraulic, or automatic systems.
Pipe Size and Pressure Requirements
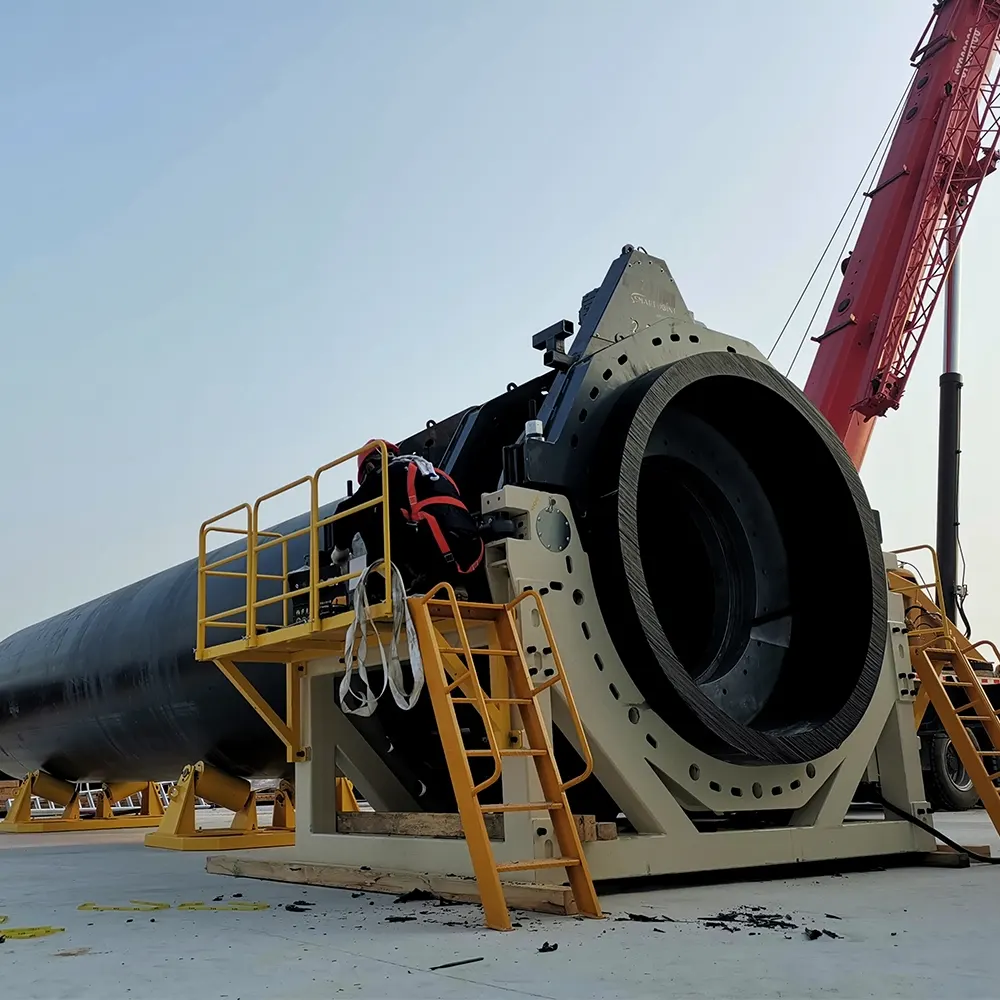
The machine’s clamping range must cover both the minimum and maximum outside diameters of your pipes. Using an undersized machine for large diameter HDPE welding applications generates excessive lateral movement. Conversely, oversized equipment on small pipes wastes resources and reduces maneuverability. Always verify the machine’s pressure rating (SDR) compatibility to ensure the fusion joint meets system design requirements.
2. Compare Machine Types: Manual, Hydraulic, and CNC
HDPE butt fusion welding machines are broadly categorized by their operation method, each offering distinct advantages for different project scales. Understanding these core differences is essential for balancing performance, labor costs, and initial investment.
| Machine Type | Operation Principle | Typical Diameter Range | Key Advantages |
|---|---|---|---|
| Manual Butt Fusion | Hand-lever clamping and movement | 63mm – 315mm | High portability, simple maintenance, low cost for small-scale projects |
| Hydraulic Butt Fusion | Hydraulic power unit for clamping and carriage movement | 160mm – 2500mm | Precise pressure control, consistent weld parameters, reduces operator fatigue |
| CNC Automatic | Programmable logic controller with touchscreen interface | 160mm – 630mm | Data logging, automatic parameter calculation, minimal human error, ISO 21307 butt fusion procedures compliance |
3. Evaluate Clamping and Frame Design
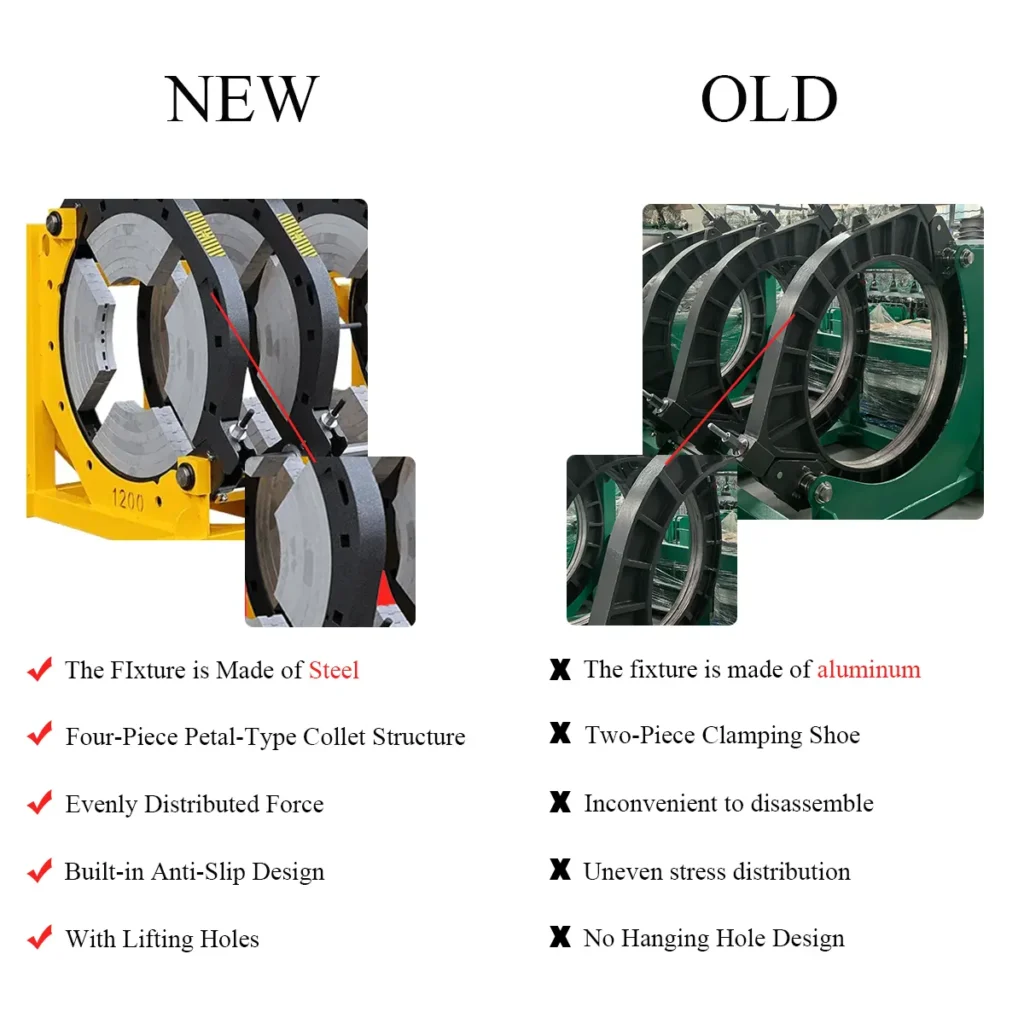
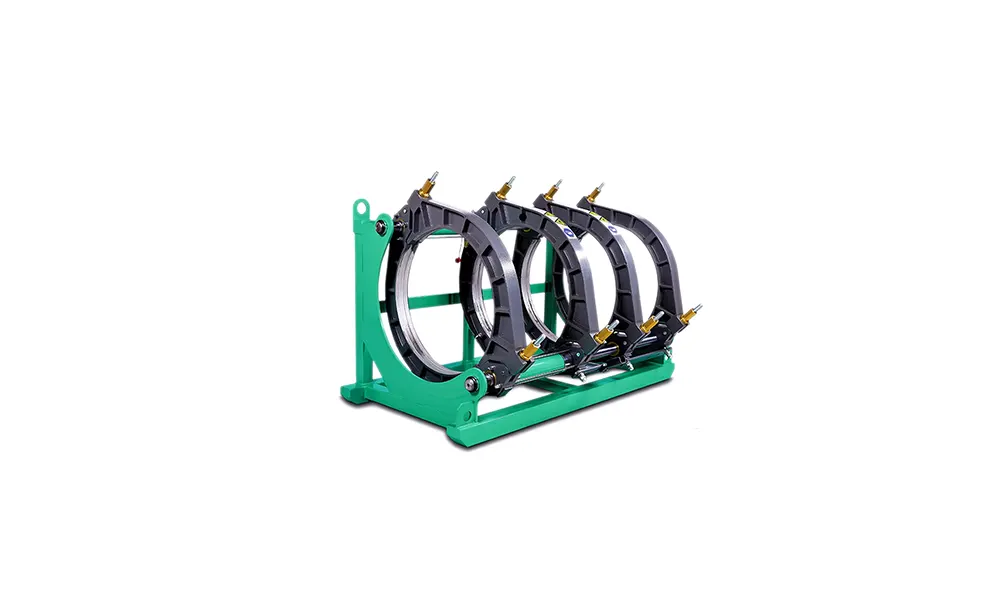
The frame and clamping mechanism determine machine rigidity and alignment precision. A robust frame constructed from high-strength steel prevents flexing under load, maintaining perfect axial alignment between pipe ends. Removable aluminum clamps or inserts simplify adaptation to different pipe diameters, reducing tooling costs. Pay close attention to the clamp insert configuration—whether they are full-circle or segmented inserts—as this affects grip uniformity and the ability to handle out-of-round pipes.
4. Heating Plate and Trimmer Quality
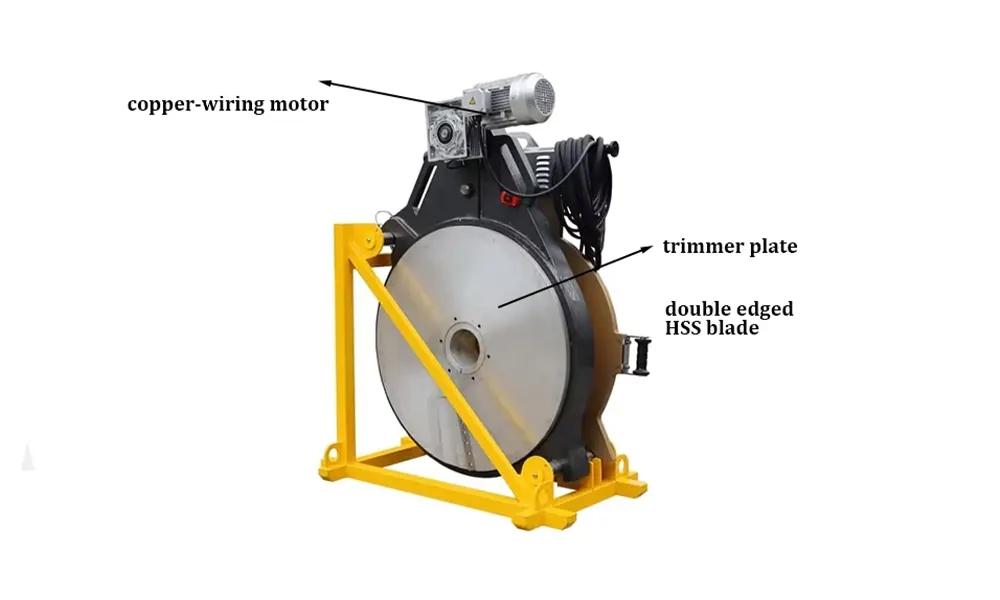
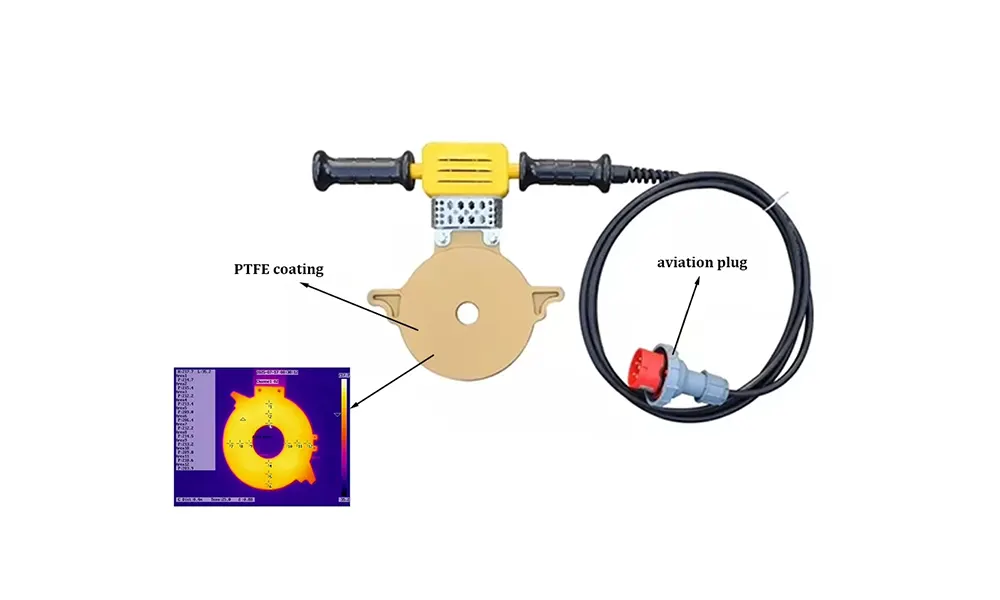
Uniform heating and clean facing are non-negotiable for strong HDPE fusion joints. The heating plate must feature a precision-machined surface with non-stick PTFE coating and minimal temperature variation across its face—typically within ±5°C. Digital temperature controllers are preferred over analog dials for automatic butt fusion machines to ensure repeatability. The trimmer tool should produce smooth, continuous shavings from both pipe ends simultaneously, confirming proper facing without chips or gouges.
5. Standards Compliance and Data Recording
Modern pipeline projects increasingly demand adherence to international PE butt fusion equipment standard specifications and traceability requirements. Verify that the machine configuration can comply with relevant standards for your region—this includes safety features, pressure gauge accuracy, and data output capability. For critical infrastructure such as gas distribution or nuclear cooling loops, CNC machines with automatic data logging provide an auditable trail of every welding cycle, proving joint quality to inspectors.
- ISO 12176-1 — Covers general requirements for butt fusion equipment used with polyethylene piping systems.
- ASTM F2620 — Standard practice for heat fusion joining of polyethylene pipe and fittings, widely referenced in North America.
- ISO 21307 — Defines butt fusion jointing procedures recognized globally for consistent fusion quality.
- DVS 2207-1 — German Welding Society directives, often specified for European gas and water pipeline projects.
6. Portability and Power Supply Considerations
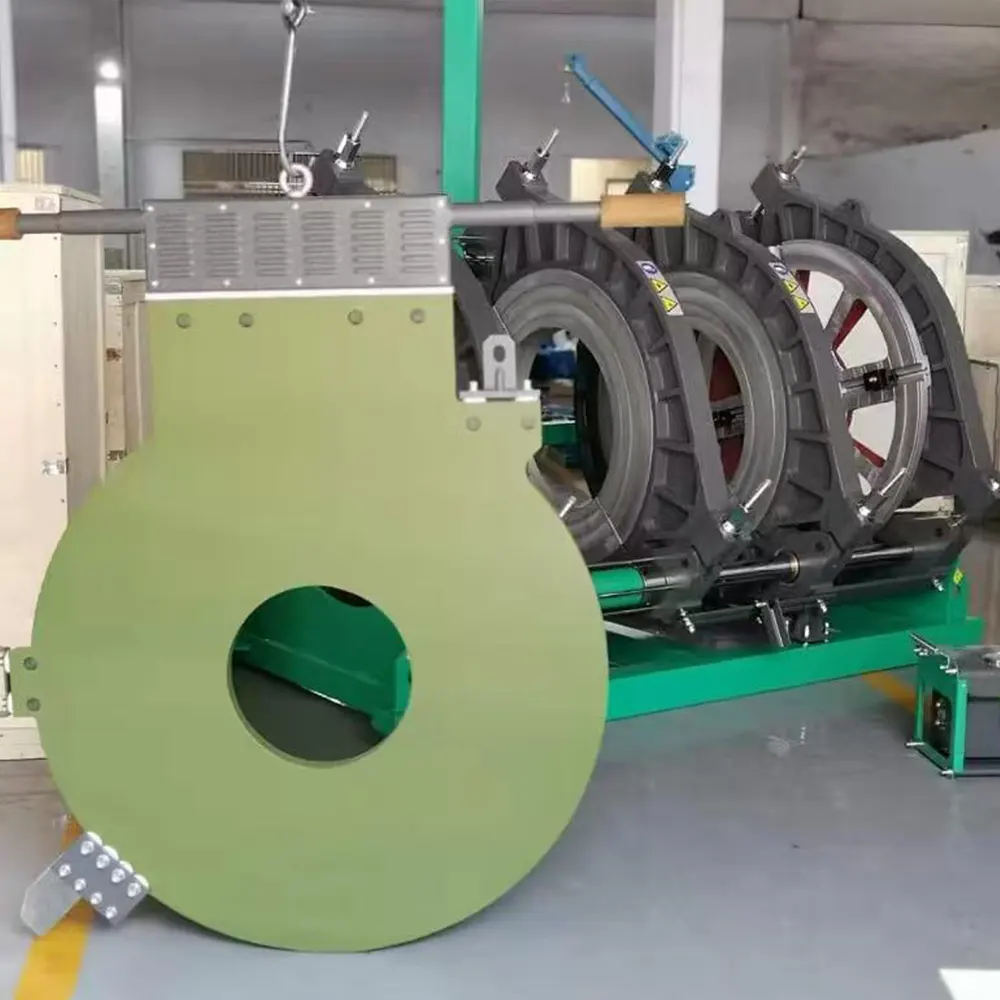
Job site mobility requirements significantly influence machine selection. Compact manual machines are ideal for repair crews moving between multiple locations daily. Hydraulic machines with detachable power units or integrated generators provide self-sufficient operation in remote areas without grid power. Consider the total assembled weight, wheel kit availability, and whether the machine can be broken down into components light enough for two-person carry regulations.
When evaluating hydraulic stations, check for dual-voltage compatibility (e.g., 230V/400V) and motor phase protection. Diesel-powered hydraulic packs extend operational range but add maintenance complexity. Military and remote industrial projects often opt for custom hydraulic power configurations matched to available site power sources.
7. After-Sales Support and Spare Parts Availability
Downtime on a pipeline fusion project costs thousands per hour in labor and equipment standby. Before committing to a machine brand, assess the manufacturer’s spare parts network in your region. Key wear items include heater cartridges, PTFE plates, clamp insert liners, and hydraulic hoses. A responsive support channel with technical troubleshooting guidance significantly reduces mean time to repair. JQ-Fusion maintains a comprehensive inventory of critical spare parts and provides lifetime technical assistance for all distributed equipment.
8. Budget and Total Cost of Ownership
While purchase price matters, the total cost of ownership calculation reveals the true investment. A cheaper machine with poor build quality leads to irregular joints, higher scrap rates, and frequent component replacements. Evaluate warranty terms, recommended service intervals, and the expected lifespan of critical components. Hydraulic machines generally command higher upfront costs but deliver faster cycle times and more consistent quality across large diameter installations. For projects requiring documented fusion traceability and minimal rework, CNC automatic machines often demonstrate the lowest long-term cost per joint.
Investment Considerations
- Initial purchase cost — weighted against project budget and expected machine utilization rate.
- Consumable parts frequency — heating plates, trimmer blades, and clamp inserts require periodic replacement.
- Calibration and certification — annual verification of temperature and pressure gauges per project specifications.
- Operator training requirements — simpler manual machines versus programmable CNC interfaces that need skilled technicians.



