
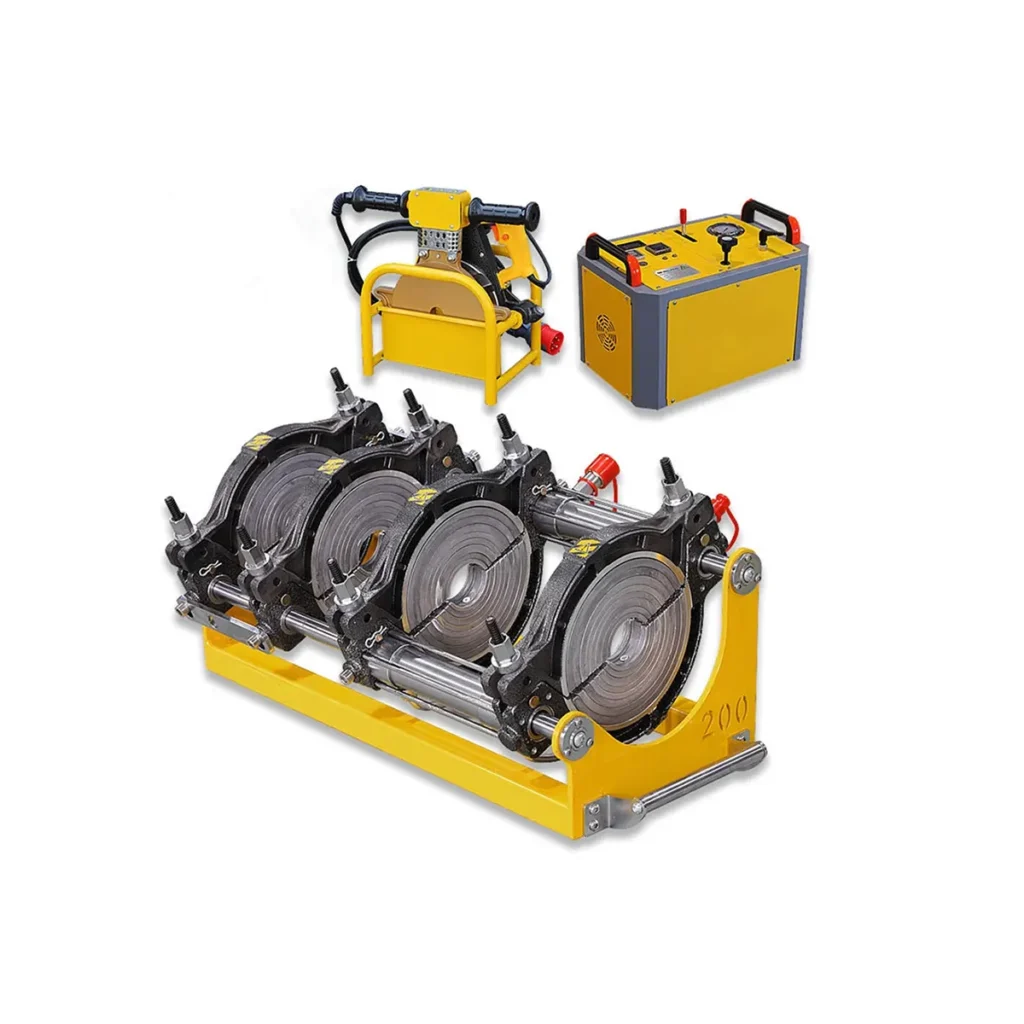
PE gas pipe welding demands strict safety protocols to protect operators, ensure leak-free joints, and maintain efficient on-site progress. This guide covers practical safety steps and best practices for operating PE (HDPE) gas pipe butt fusion machines so you can achieve secure, compliant, and consistent welds.
Understand the Hazards Before You Start
Common risks with PE gas pipe welding include burns from heated plates, high-pressure equipment failures, inhalation of fumes during trimming or extrusion, and joint failures due to contamination or incorrect parameters. Recognizing these hazards up front helps you plan controls and avoid costly rework or unsafe conditions.
Key Hazard Areas
– Hot plate and heater contact
– Hydraulic leaks or sudden movement of clamps
– Poorly prepared pipe ends causing voids or weak joints
– Electric/electronic faults on automatic machines
– Confined-site ventilation and gas exposure
Personal Protective Equipment (PPE) and Site Setup
PPE is the first line of defense. Ensure every operator and assistant uses appropriate gear and that the work area is organized for safe, efficient fusion operations.
Recommended PPE
– Heat-resistant gloves and protective sleeves
– Safety glasses with side protection or welding goggles
– Flame-retardant workwear and steel-toe boots
– Hearing protection when using hydraulic or noisy equipment
– Respiratory protection if ventilation is inadequate during trimming
Site Preparation Tips
– Choose a level, stable surface and keep the immediate area clear of flammable materials.
– Provide good lighting and mark an exclusion zone around heated components.
– Ensure safe access for emergency exits and equipment removal.
Pre-Operation Machine Inspection (Checklist)
Performing a standard inspection before each shift reduces failures. Use the table below as a quick reference checklist for hydraulic, manual, and automatic butt fusion machines.
| Item | What to Check |
|---|---|
| Hydraulics & Hoses | Leaks, pressure stability, fittings torque |
| Heater Plate | Surface cleanliness, temperature control, cable integrity |
| Clamps & Alignment | Jaw wear, pipe centering, alignment pins |
| Electronic Controls | Power supply, emergency stop, sensor calibration |
| Accessories | Trimmer blades, scrapers, calibration gauges |
Step-by-Step Safe Operating Procedure
Follow a repeatable workflow to achieve consistent welds and reduce risk:
1. Preparation
– Verify pipe material (PE100/PE80) and wall thickness. Confirm welding parameters from approved procedure specifications (pressure, heating time, cooling time).
– Clean and square-cut pipe ends using a trimmer. Remove contaminants and chamfer only if specified by procedure.
2. Alignment & Clamping
– Center pipes precisely in clamps. Use alignment pins or fixtures for larger diameters. Tighten evenly to avoid eccentricity. Misalignment is a leading cause of poor-quality joints.
3. Heating & Fusion
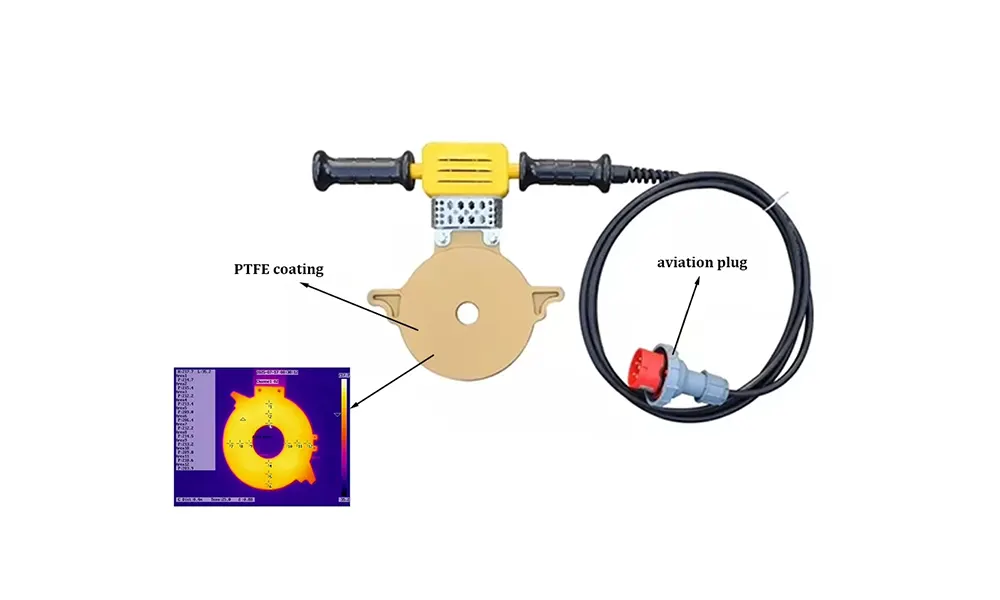
– Bring the heating plate to the recommended temperature and avoid touching the hot surface. Use controlled approach and apply pressure per procedure. Monitor time and force using machine readouts or calibrated gauges.
4. Joining & Cooling
– After removing the heater, apply the specified consolidation force and hold for the full cooling time. Avoid disturbing the joint until it cools to ambient temperature to prevent stress or voids.
Welding Parameters and Controls
Correct parameters are non-negotiable for gas mains. Record and verify these values for every weld:
- Heating temperature (°C)
- Heating time (s or min)
- Approach pressure and fusion pressure (kN or bar)
- Cooling/holding time
Use machine log functions or a paper weld log to capture operator, date, pipe IDs, and parameter readouts for traceability.
Common Parameter Mistakes
– Overheating (too high temperature or too long) weakens polymer structure.
– Insufficient pressure during consolidation causes incomplete fusion.
– Short cooling times lead to shrinkage and micro-voids.
Monitoring, Quality Control & Non-Destructive Checks
Visual inspection of bead profile and joint symmetry is essential. For gas work, employ additional checks:
- Visual bead inspection and caliper measurements
- Electrofusion or mechanical joint pressure testing where required
- Record retention and tagging of welded sections
Maintenance & Troubleshooting Table
| Symptom | Likely Cause | Action |
|---|---|---|
| Uneven bead | Misalignment or uneven pressure | Re-align clamps, repeat weld following procedure |
| Heater stops heating | Thermostat or wiring fault | Isolate power, inspect cable & control board, replace faulty parts |
| Hydraulic pressure drop | Leak or pump wear | Check hoses, seals, service pump and fluid |
Emergency Procedures & Safe Shutdown
Define and drill emergency actions: stop weld, isolate power/hydraulics, cool hot surfaces safely, and evacuate if a gas release is suspected. Keep fire extinguishers and first-aid kits accessible and train staff on burn care.
Training, Documentation & Operator Competence
Only trained and certified operators should weld gas mains. Maintain current procedure documents, weld logs, and machine calibration records. Periodic skill refreshers and documented competence checks improve on-site safety and joint reliability.
Final Notes
For industrial-grade butt fusion machines, reliable manufacturing and technical support matter. JQ-Fusion supplies a broad range of manual, hydraulic, and automatic HDPE welding machines and can provide specifications and spares to help you maintain safe, efficient operations. Visit JQ-Fusion for product details and technical resources.



