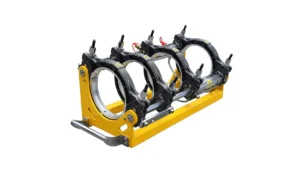
Precision Hydraulic Butt Fusion Machine for High-Integrity Pipe Joints
Engineered for uncompromising pipeline safety in water distribution, gas networks, mining slurries, and industrial conduits. Deliver continuous, zero-leak joint efficiency compliant with international standards.
The Mechanics of High-Integrity Butt Fusion
A hydraulic butt fusion machine is the foundational benchmark for joining thermoplastic piping, specifically high-density polyethylene (HDPE), polypropylene (PP), and PVDF. By utilizing precisely controlled hydraulic cylinders, the equipment drives pipe ends against a PTFE-coated heating plate under exact pressures.
Hydraulic Pressure Clamping
High-tensile aluminum alloy clamps rigidly lock the pipe sections, securing true roundness and zero axial offset throughout high-pressure joining cycles.
Dual-Facet Planing Planer
Reversible high-speed electric facers trim pipe ends perpendicular to the centerline, clearing oxidative layers and creating smooth mating faces.
Digitally Regulated Heating
PTFE non-stick heating mirrors provide uniform surface temperature gradients across diameters, vital for homogeneous polymer chain interpenetration.
Executing Calibrated Fusion Protocols
Creating homogenous joints that exhibit 100% monolithic strength requires rigorous adherence to standardized parametric profiles, including ISO 21307 butt fusion procedures, ASTM F2620 heat fusion protocols, and technical guidelines outlined by the PPI butt fusion procedure (TR-33).
Every phase is calibrated according to the pipe diameter, wall thickness (SDR ratio), and specific resin chemistry. When executing welds with ISO 4427 PE water pipes or ASTM D2513 PE gas pipe, the hydraulic unit ensures exact drag compensation and hydraulic interface pressures.
Drag Pressure Compensation: The hydraulic power unit accurately measures mechanical sliding friction prior to facing, automatically superimposing dynamic line drag onto the programmed joint interface pressure.
| Fusion Phase | Key Parameter | Critical Control Target |
|---|---|---|
| 1. Bead-Up | High Pressure | Uniform roll-back bead formation on all circumference points. |
| 2. Heat Soak | Zero / Contact Pressure | Controlled thermal saturation without molten displacement. |
| 3. Plate Extraction | < 3 – 8 Seconds | Rapid plate withdrawal to minimize open melt pool oxidation. |
| 4. Fusion & Cooling | Calculated Interface P | Sustained pressure hold under ambient in-clamp cooling. |
Engineered Hydraulic Butt Fusion Series
Explore our high-performance line of hydraulic fusion welders designed for extreme trench environments, municipal networks, and heavy-wall industrial piping.
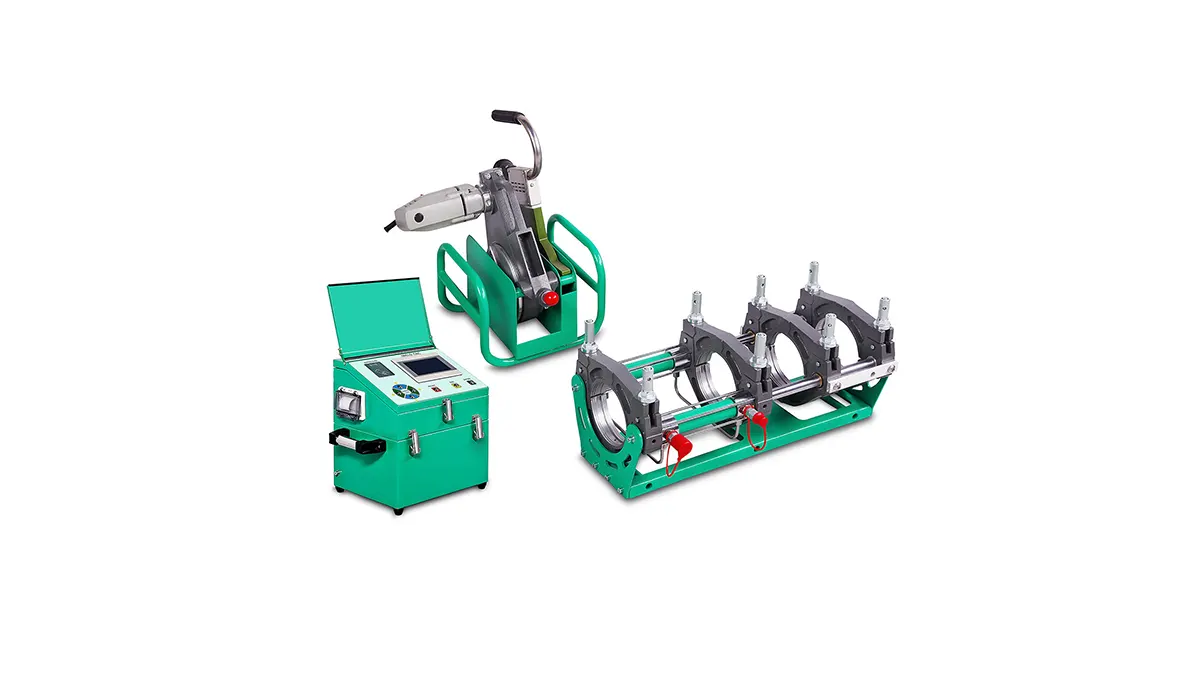
Hydraulic Butt Fusion Machine with Aluminum Clamps
Versatile field equipment featuring modular aluminum inserts, low start-up pressure hydraulics, and Teflon-coated digital hot plates.
View Specifications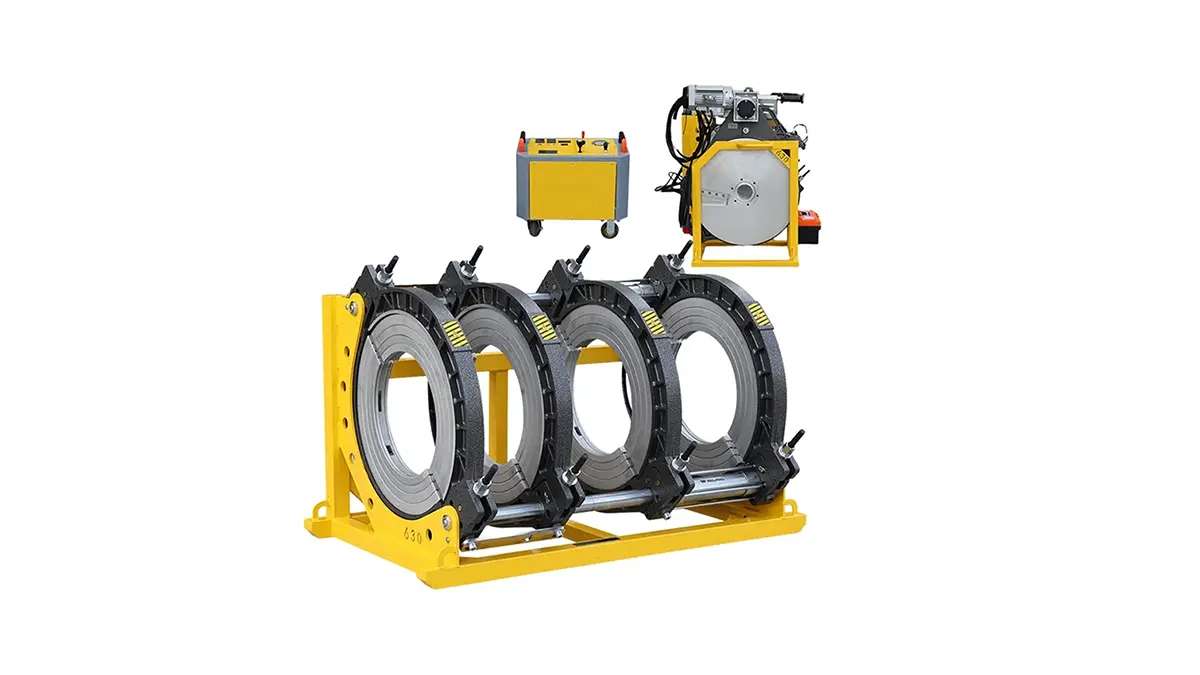
JQH630mm Hydraulic Butt Fusion Welding Machine
Designed for intermediate transmission mains from 315mm to 630mm. High structural rigidity resists bending under maximum fusion loads.
View Specifications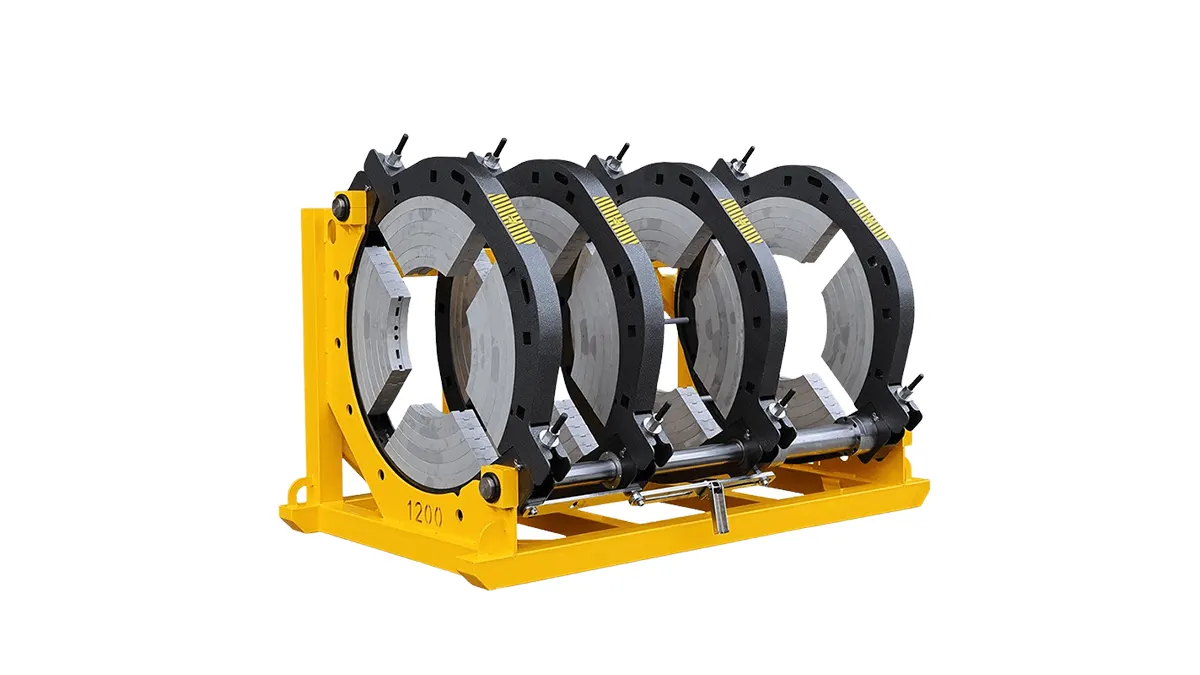
JQH1200mm Heavy-Duty Hydraulic Fusion Welder
Heavy-duty industrial machine engineered for large-diameter HDPE water intakes, mining tailings, and municipal sewage lines up to 1200mm.
View SpecificationsHydraulic vs. Alternative Fusion Methodologies
Selecting the appropriate fusion equipment depends on pipeline diameter, operating pressure ratings, and field site conditions.
| Technology Type | Applicable Pipe Range | Primary Advantages | Key Field Application | Compliance Standard |
|---|---|---|---|---|
| Hydraulic Butt Fusion | 90mm – 2250mm | Continuous high clamping force, uniform bead geometry, monolithic joint strength. | Long-distance water mains, gas transmission, mining pipelines. | ISO 21307, ASTM F2620 |
| CNC Automatic Fusion | 160mm – 630mm | Full data-logging, automated cycle execution, eliminated operator error. | High-risk combustible gas networks, chemical pipelines. | ISO 12176-1 / 4 |
| Manual Butt Fusion | 40mm – 250mm | Lightweight, highly portable, zero electrical hydraulic dependence. | Small-diameter drainage, low-pressure rural agriculture. | DVS 2207 |
| Electrofusion Units | 20mm – 630mm | Compact clearance fusion, ideal for tie-ins and repair saddle joints. | Urban gas service connections, congested trench repairs. | ISO 12176-2, ASTM F1290 |
About JQ-Fusion Manufacturing
JQ-Fusion is a professional manufacturer specializing in HDPE pipe welding machines, providing reliable butt fusion solutions for global infrastructure projects. With years of dedicated industry experience, we engineer high-capacity hydraulic butt fusion welding machines, CNC automatic systems, and multi-angle fitting fabricators covering diameters up to 2250mm.
From water transmission grids to demanding mining slurry circuits, our machinery delivers stable heating, precise alignment, and long-term durability across tough operational environments.
- Reliable Welding Performance: Consistent clamping pressure and uniform thermal heating plates.
- OEM / ODM Customization: Custom clamping sizes, corporate colors, and tailored power packs.
- Global Support & Large Stock: Immediate dispatch on high-demand units and worldwide spares supply.
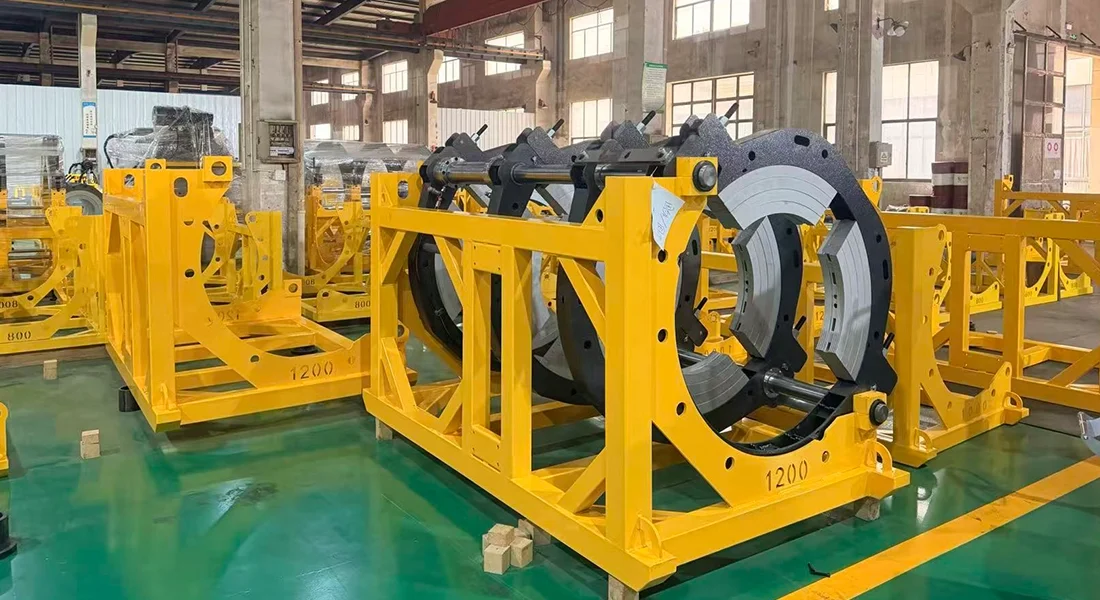
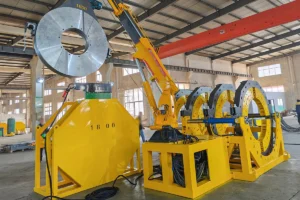
State-of-the-Art Inventory & Packaging
Explore our production and stocking facility, ensuring ready delivery of butt fusion machines and components.
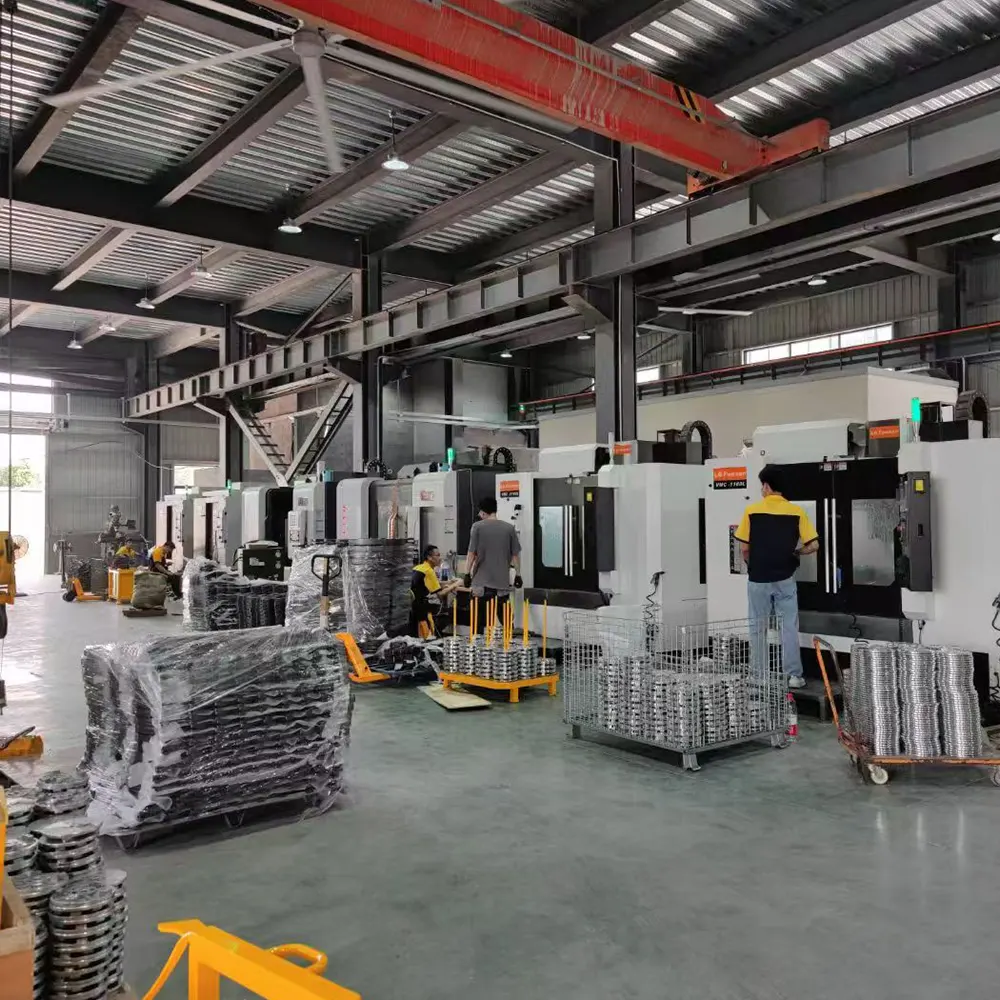
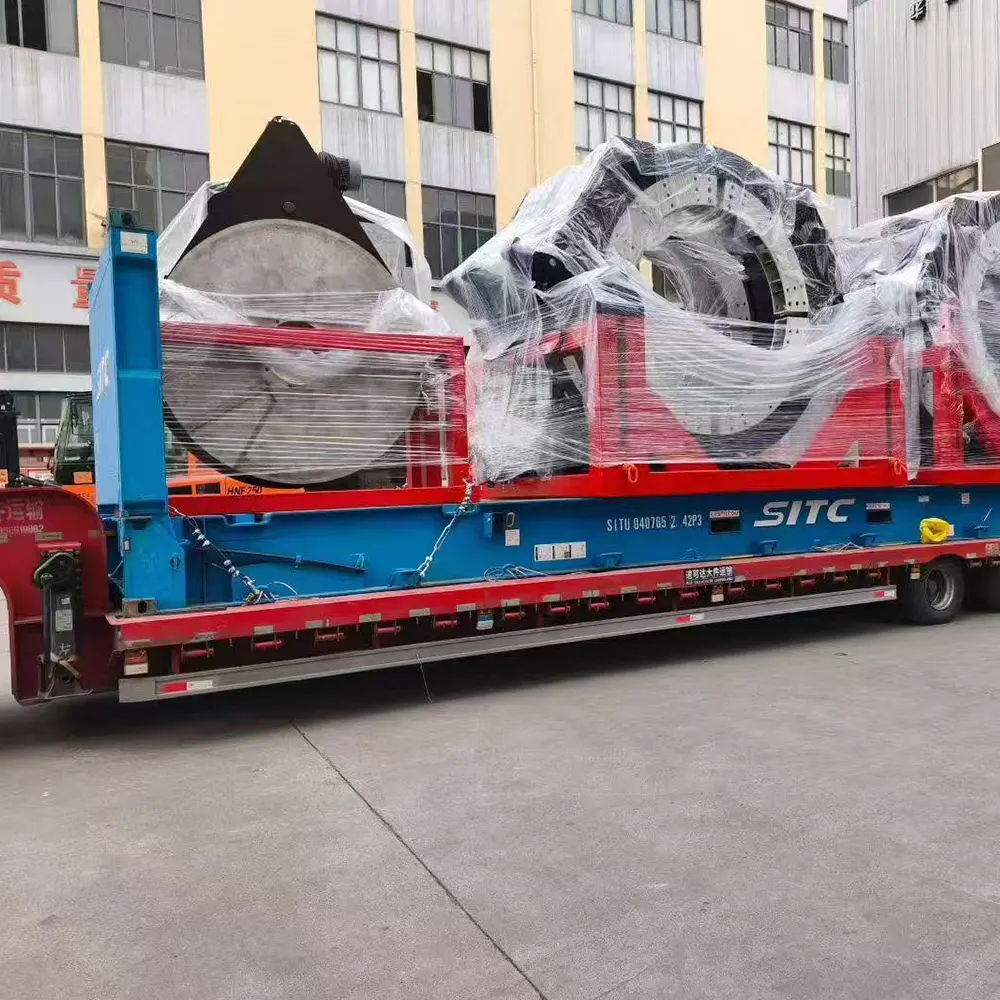
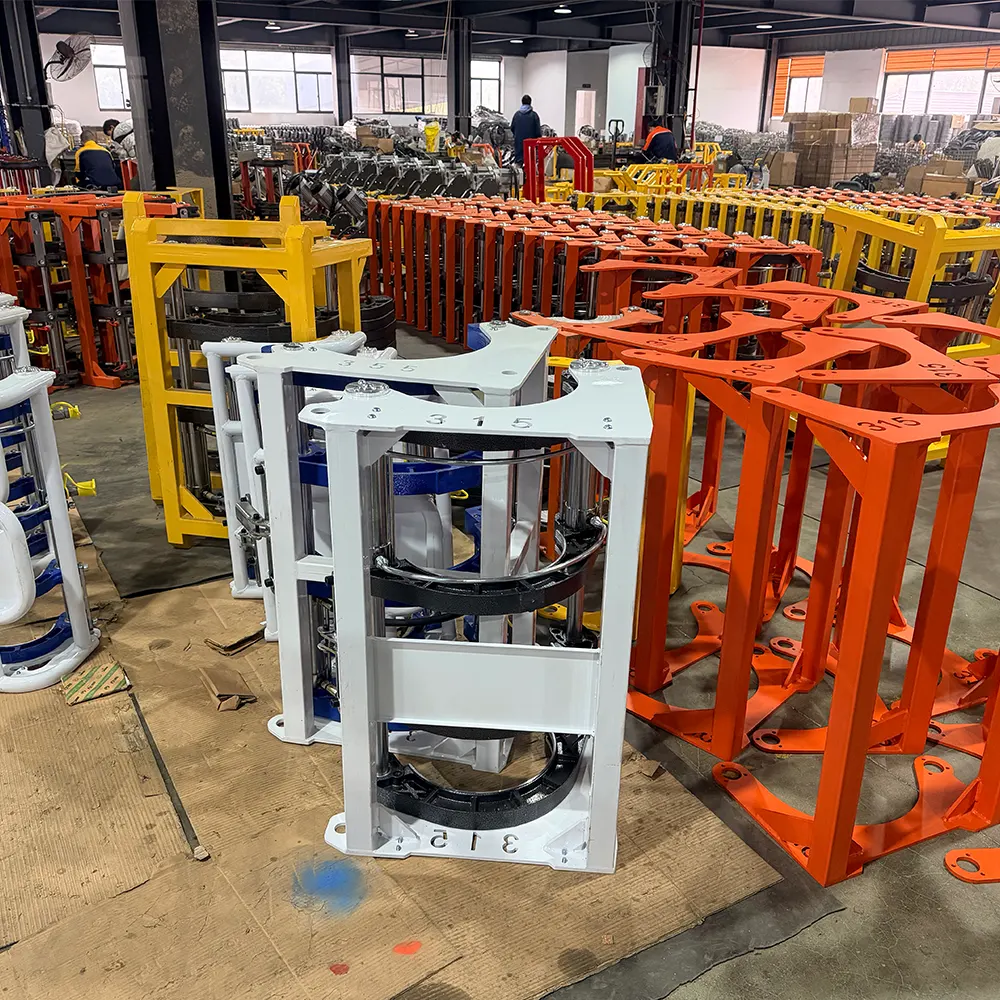
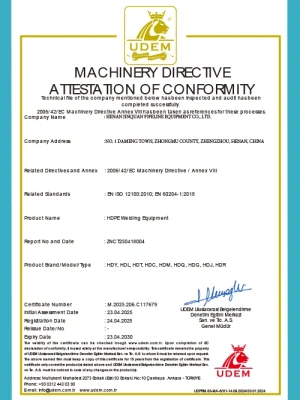
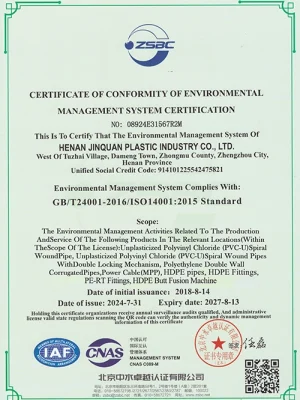
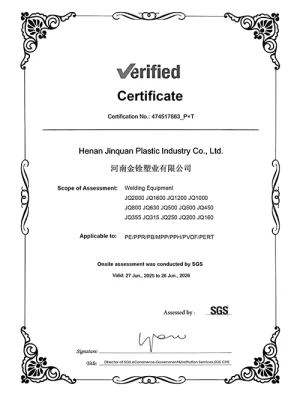
International Quality Certifications
Our manufacturing processes and equipment adhere strictly to international manufacturing standards, verified by CE, ISO 9001, and SGS testing audits.
Frequently Asked Questions
Find engineering answers regarding pipe jointing, hydraulic parameter calculations, and machinery operation.
How is hydraulic fusion pressure calculated?
Fusion pressure is calculated by multiplying the interfacial pressure requirement (from ISO 21307 or ASTM F2620) by the pipe’s cross-sectional area, then dividing by the total cylinder area of the hydraulic butt fusion machine, plus the measured drag pressure.
Can different PE wall thicknesses (SDRs) be welded together?
Butt fusion requires matching wall thicknesses to ensure equal thermal soak and melt flow. When joining differing SDR ratings, the heavier wall must be machined/chamfered internally or joined using compatible electrofusion fittings.
What causes butt fusion joint failures?
Common failure causes include inadequate pipe end planing (angular misalignment), particulate contamination on the heating plate, improper heat soak duration, or premature removal of hydraulic cooling pressure.
Do you provide custom clamp inserts for non-standard pipes?
Yes. JQ-Fusion offers bespoke OEM and ODM clamp configurations, specific IPS/DIPS inserts, and multi-voltage power packs tailored to regional field specifications.