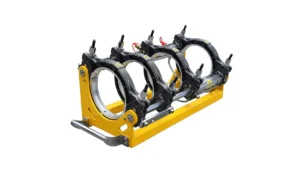
Engineering Indestructible Polyethylene Joint Homogeneity
Modern high-density polyethylene (HDPE 100 and PE4710) piping networks rely on molecular co-crystallization rather than mechanical coupling. Selecting top-tier HDPE pipe fusion equipment ensures zero-leakage, high-strain tolerance, and a 100+ year operational lifespan.
High-density polyethylene pipelines have reshaped global water conveyance, chemical processing, and natural gas infrastructure. However, the integrity of a pipeline is fundamentally governed by the metallurgical and thermal precision of its weld joints. According to guidelines set by the Plastics Pipe Institute (PPI TN-51), authentic butt fusion does not merely bond surfaces—it interlocks polymer chain molecules under controlled melt viscosity and hydraulic pressure.
Achieving this molecular uniformity demands certified PE butt fusion equipment standard hardware featuring micron-level clamp alignment, computerized dwell-time management, and uniform Teflon-coated heating plates.
Featured HDPE Pipe Fusion Equipment Categories
Explore specialized fusion apparatus tailored for trench-side welding, factory fabrication, large civil conduits, and tight-access service lines.
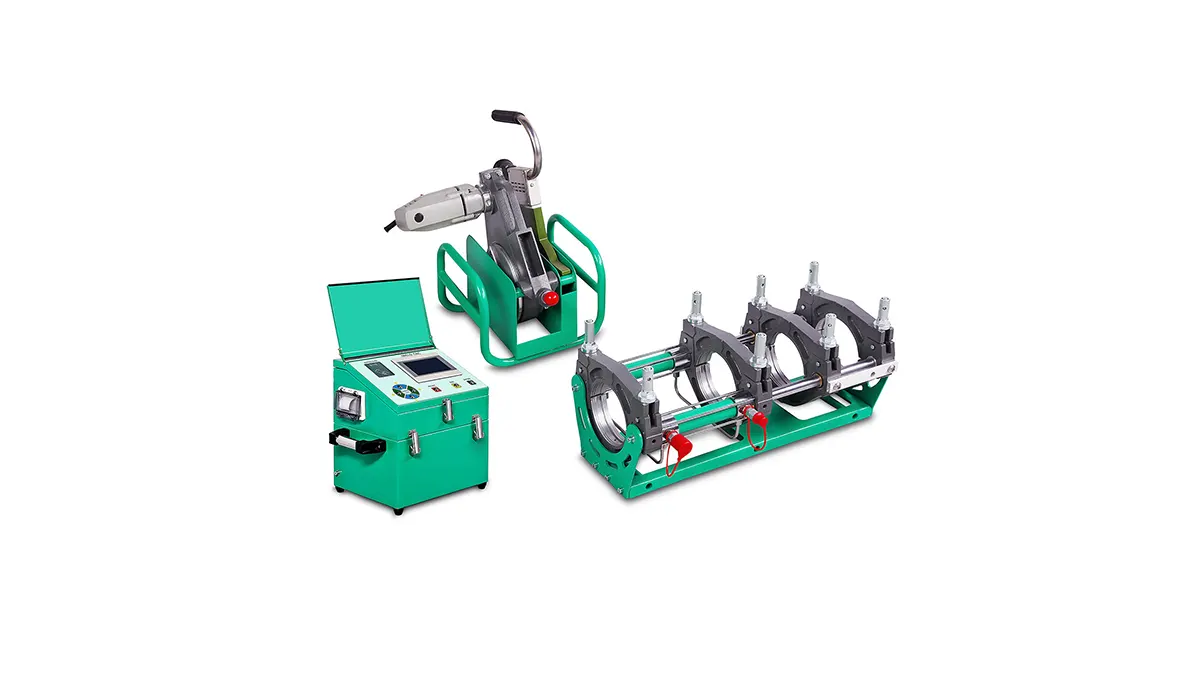
Hydraulic Butt Fusion Welders
Heavy-duty hydraulic power packs paired with lightweight alloy clamps for field pipelines ranging from 50mm up to 2250mm.
View Hydraulic Series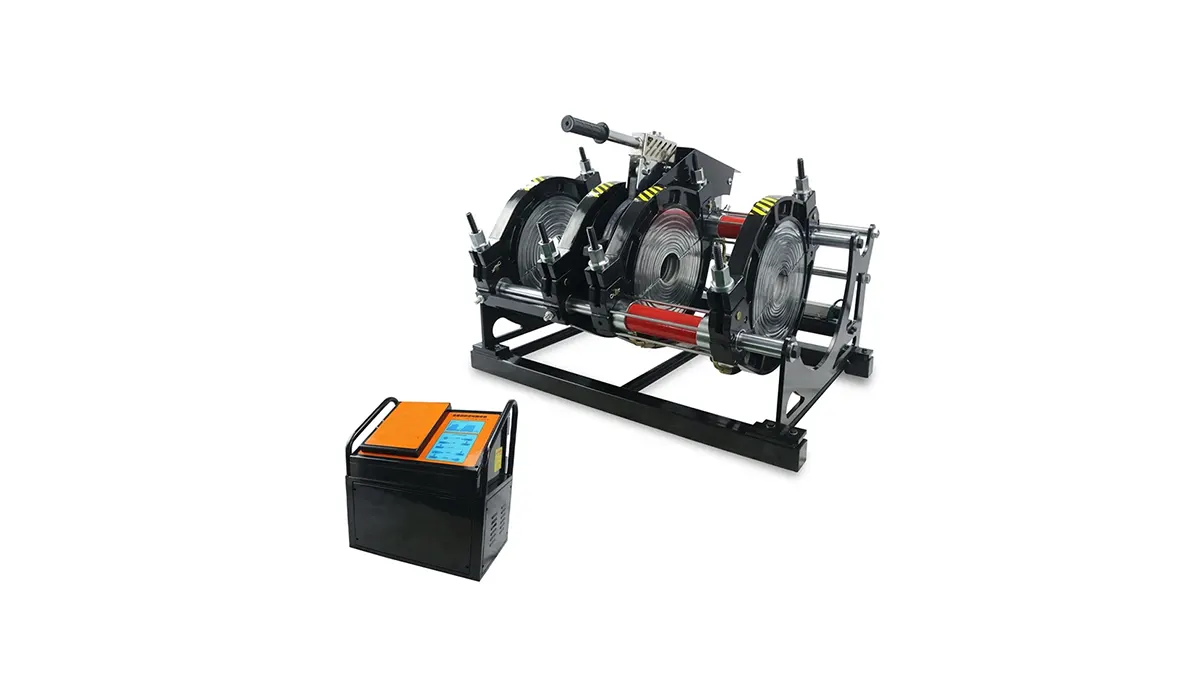
CNC Automatic Fusion Units
Fully automated PLC-driven cycle execution with integrated data-logging compliant with ISO 12176-4 QA protocols.
View CNC Models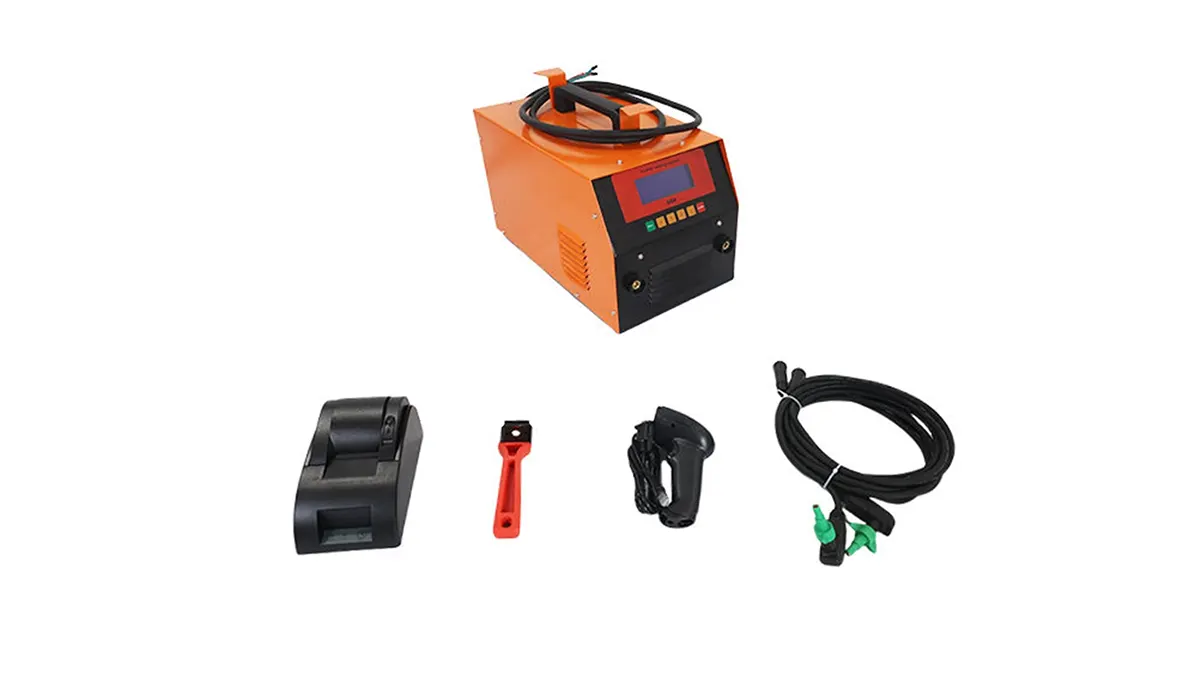
Smart Electrofusion Units
Barcode-scanning electrofusion control boxes delivering consistent output voltage for critical gas distribution tie-ins.
View Electrofusion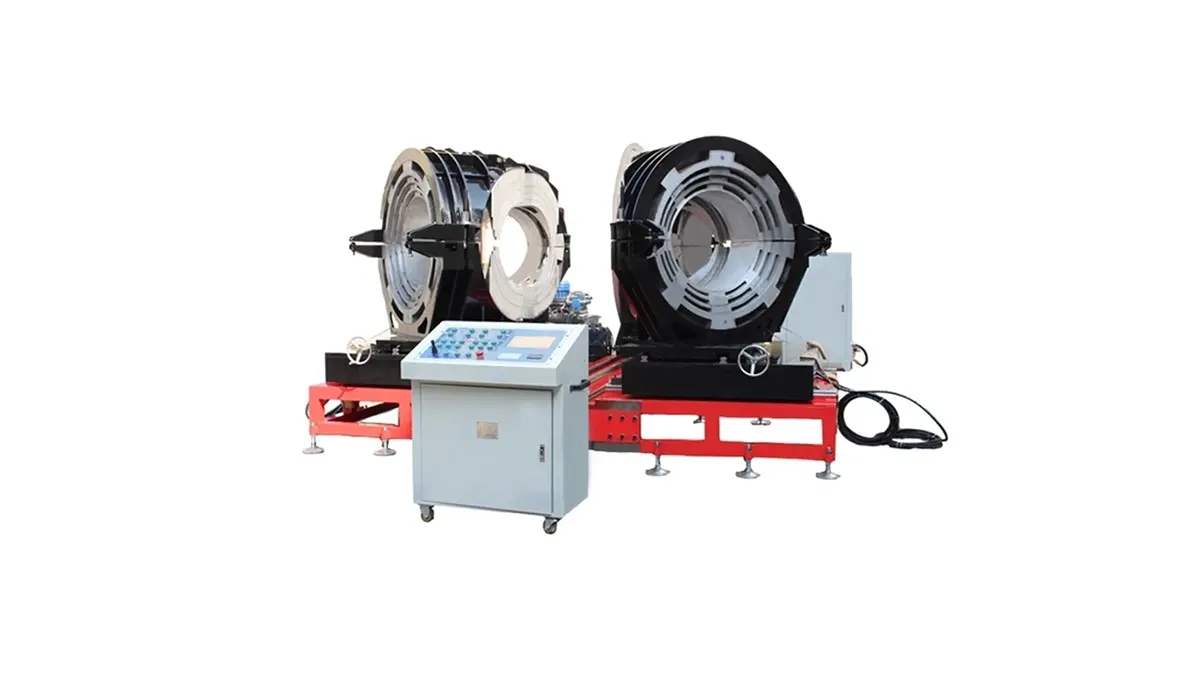
Workshop Fitting Machines
Engineered for multi-angle miter fabrication (elbows, tees, crosses) conforming to ASTM F2206 standards.
View Workshop UnitsStep-by-Step Butt Fusion Methodology & Parameter Control
Executing qualified joints according to PPI TR-33 generic butt fusion procedures requires strict adherence to four thermodynamic phases.
Facing & Alignment
Electric planer trues pipe ends square. Mismatch must not exceed 10% of pipe wall thickness to prevent localized stress risers under dynamic pressure.
Heat Soak & Bead Up
Controlled hydraulic contact establishes initial melt bead roll-back (204°C–232°C / 400°F–450°F), shifting to zero interfacial pressure during molecular heat soak.
Interfacial Fusion & Cool
Rapid heater plate withdrawal followed by immediate hydraulic ramp-up to calculated fusion interfacial pressure, held unyielding through natural ambient cooling.
Fusion Technology Comparison Matrix
| Technology Type | Primary Pipe Diameters | Operational Complexity | Field Trench Usability | Best Suited Application |
|---|---|---|---|---|
| Hydraulic Butt Fusion | 63mm to 2250mm (2″ – 88″) | Semi-Automated / Operator Monitored | High (Modular Chassis) | Water main distribution, mining tailings, municipal drainage |
| CNC Automatic Butt Fusion | 90mm to 1200mm (3″ – 48″) | Full PLC / Zero Human Interference | Moderate (Requires Stable GenSet) | High-pressure natural gas grids, industrial hazardous chemicals |
| Electrofusion (EF) | 20mm to 800mm (0.75″ – 32″) | Barcode Automatic Calibration | Extreme (Compact for Narrow Pits) | Gas service taps, trenchless pull-back tie-ins, emergency repair |
| Manual Butt Fusion | 40mm to 250mm (1.5″ – 10″) | Manual Lever / Screw Mechanism | High (Ultra Portable) | Low-pressure conduits, building drainage, irrigation |
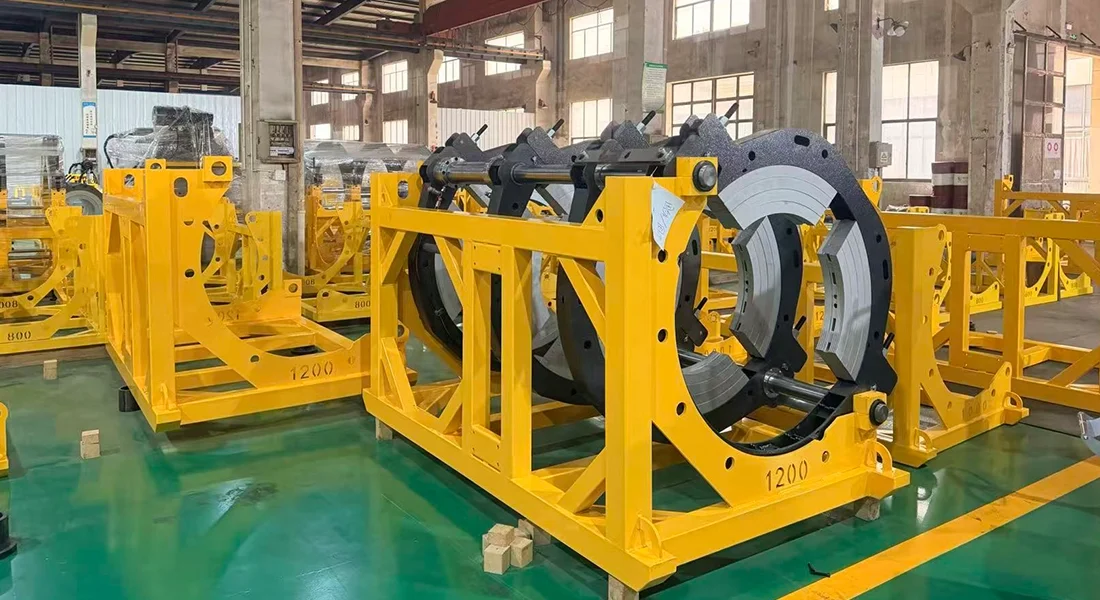
State-of-the-Art Factory Infrastructure & Large Stock Inventory
Supporting global contractors with rapid dispatch, comprehensive OEM/ODM customization, and rigorous multi-point quality assurance.
Certified Manufacturing
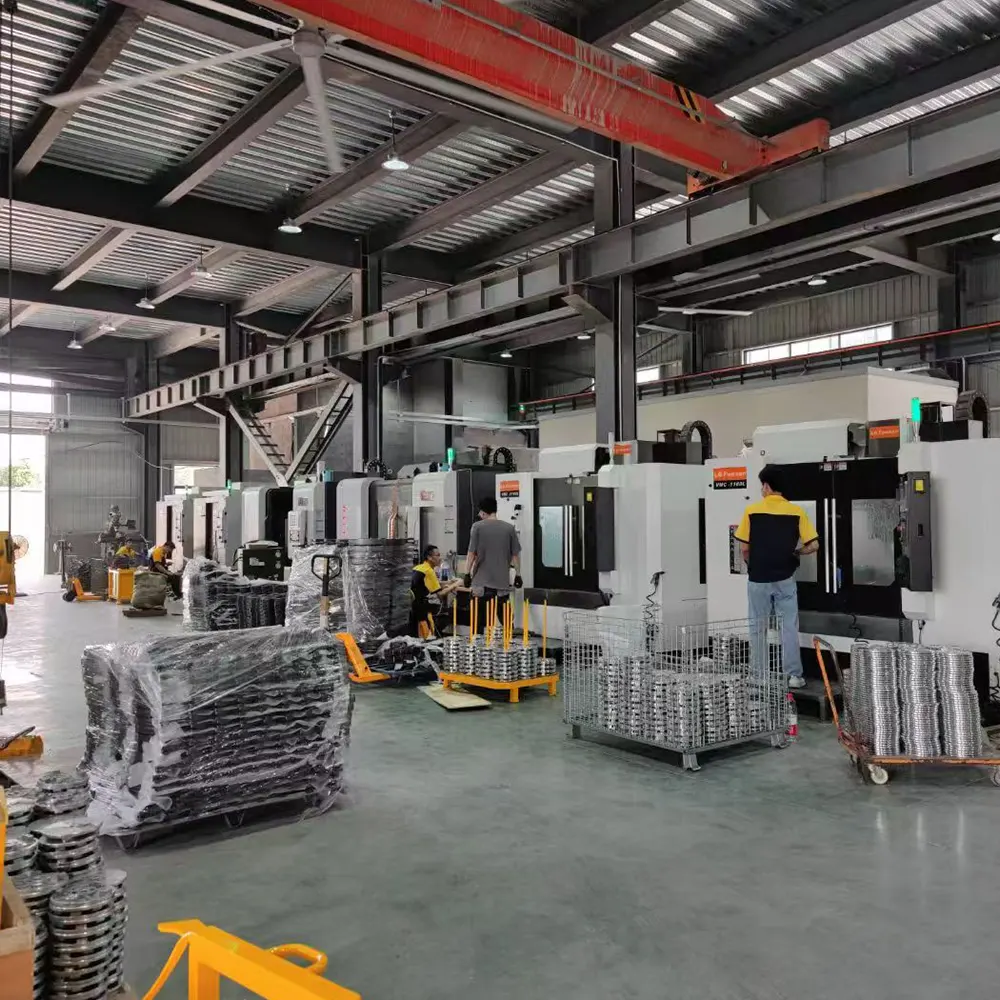
Every butt fusion unit passes strict clamp concentricity, digital pressure stability, and thermal distribution testing before crating.
Tailored Custom Solutions
Customized chassis colorways, client branding, high-altitude heating options, and dual-voltage power setups available.
Immediate Stock Dispatch
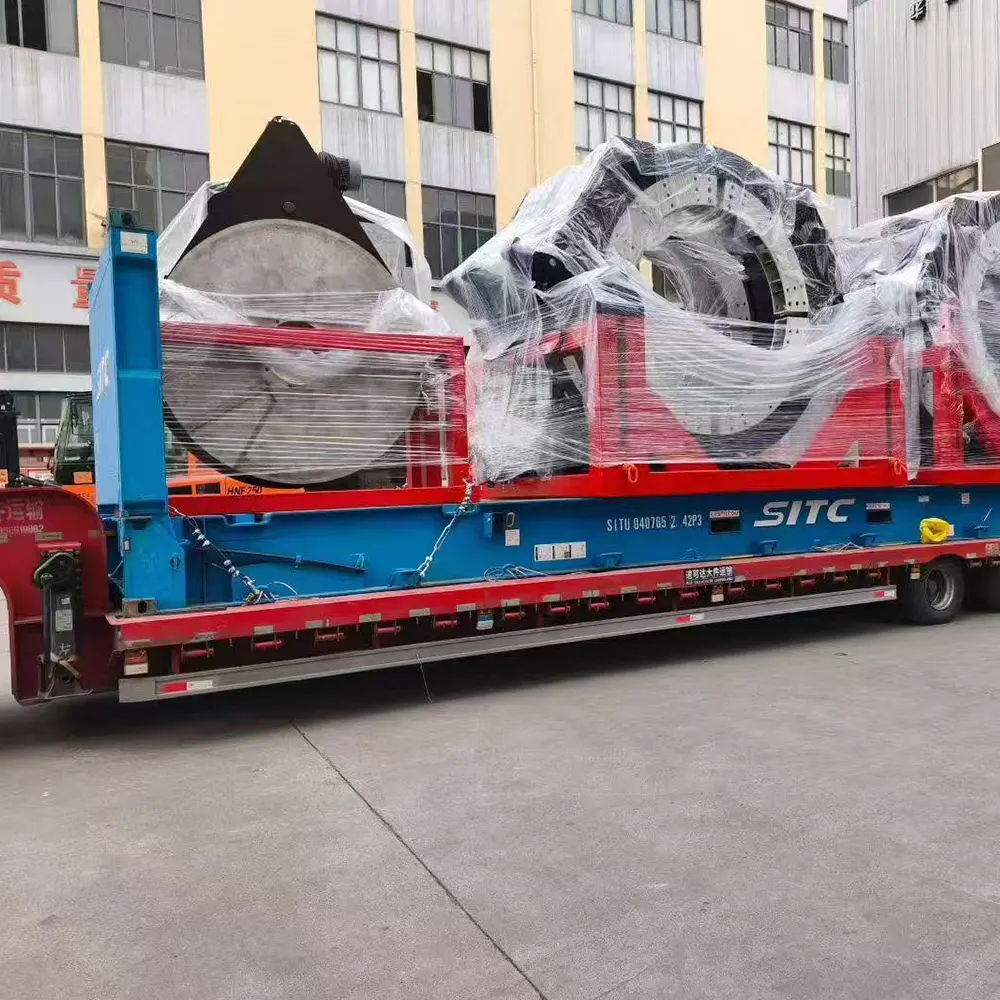
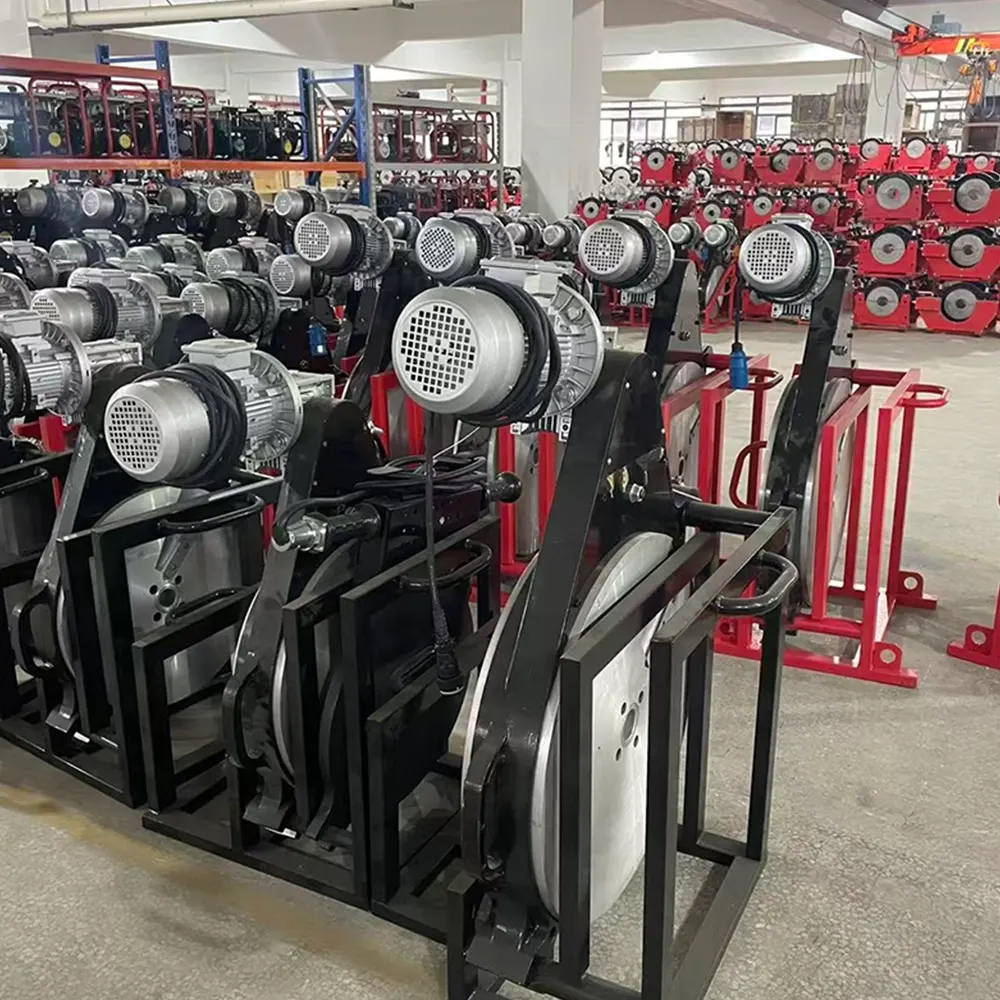
Massive inventory of manual and hydraulic models from 160mm to 1600mm stocked for immediate international sea/air freight.
Factory Warehouse & Readiness Overview
International Certifications & Rigorous Standards
Engineered in strict accordance with ISO 4427 water supply guidelines, ISO 4437 gas network rules, and global safety regulations.
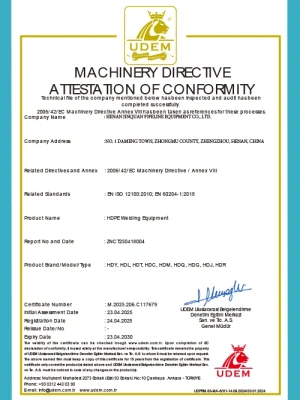
CE Safety Compliance
High & low voltage electrical directives and machinery hazard safety verified.
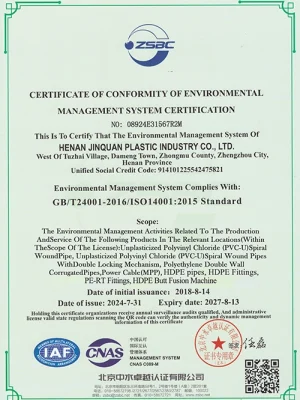
ISO 9001 Quality System
Comprehensive factory auditing covering component machining, assembly, and test logging.
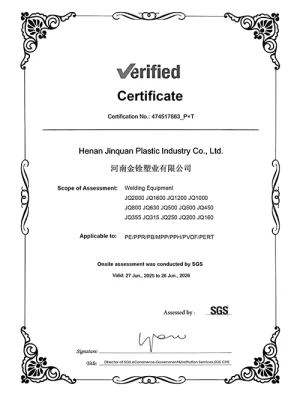
SGS Audited Partner
Third-party verified production facilities, export qualifications, and physical performance.
HDPE Pipe Fusion Equipment Engineering FAQs
Answers to frequently encountered engineering, pressure calibration, and machine selection questions.
What is drag pressure and why is it critical?
Drag pressure is the hydraulic force required to overcome friction and move the carriage holding the pipe. It must be added to the calculated theoretical fusion pressure; neglecting drag results in under-pressurized joints prone to slow crack growth.
Can different SDR wall thicknesses be butt-welded?
Direct butt fusion between different SDR classes (e.g., SDR 11 to SDR 17) is prohibited without specialized machining transitions, as unequal wall thicknesses lead to asymmetrical thermal mass and uneven bead morphology.
How does ambient temperature affect fusion parameters?
In sub-zero or high-wind environments, heating plates require wind-screens and extended soaking times under ASTM F2620. Cooling cycles must remain natural—never accelerate cooling with water or compressed air.
Why choose CNC automatic equipment over standard hydraulic?
CNC units automatically govern pressure ramp-up, open/close dwell times, and heater removal, capturing tamper-proof digital weld logs that meet pipeline operator and utility validation standards.
Partner with JQ-Fusion for Reliable Joint Solutions
Whether you require high-volume container shipments for regional distributorship or engineered hydraulic butt welders for high-profile civil pipeline execution, our engineering team is ready to assist with full technical data sheets, operation manuals, and distributor pricing.
Direct Engineering Support Email
[email protected]24/7 International Phone / WhatsApp
+86 15093385787Headquarters & Manufacturing Hub
Zhengzhou, Henan Province, China