Premier Hydraulic PE Pipe Welding Machine Manufacturer
Engineering advanced, high-tonnage thermoplastic fusion machinery. Engineered for continuous duty in extreme field environments, JQ-Fusion delivers high-precision hydraulic butt fusion welders for polyethylene (PE100, PE80, HDPE) and polypropylene pressure pipeline networks worldwide.
State-of-the-Art Hydraulic Butt Fusion Systems
In modern critical fluid handling infrastructure, the joint integrity of solid-wall Polyethylene (PE) pipelines determines overall system longevity. As a specialized hydraulic PE pipe welding machine manufacturer, JQ-Fusion designs and builds field-proven hydraulic systems engineered to execute standardized thermal butt fusion in accordance with ISO 21307 butt fusion procedures, ASTM F2620 heat fusion, and PPI butt fusion procedure protocols.
Unlike manual clamping equipment, our hydraulic butt fusion machines utilize an electro-hydraulic control unit that regulates interfacial pressure with exacting precision throughout every phase of the fusion cycle: initial bead-up, heat soak, quick plate changeover, fusing pressure build-up, and monitored cooling under pressure. This eliminates mechanical strain inconsistencies and operator variance, guaranteeing full molecular interlacing across pipe ends.
Mechanical & Hydraulic Core Capabilities
- Heavy-Duty Structural Chassis: Constructed from high-tensile structural steel alloy with reinforced slide bars to prevent axial deflection during heavy drag pull.
- Precision Hydraulic Power Pack: Equipped with an accumulative hydraulic manifold, fine pressure relief valve, and high-accuracy fluid gauge conforming to PE butt fusion equipment standard ISO 12176-1.
- Integrated Planer & Planing Tool: Reversible dual-edge HSS cutter blades with safety micro-switches to ensure perfectly planar, square pipe end geometries.
- Electronically Regulated Heating Plate: Coated with high-grade industrial PTFE, delivering uniform thermal distribution across ±3°C tolerance.
Industrial Hydraulic Fusion Machine Portfolio
Our comprehensive equipment line addresses all outer diameter (OD) requirements from compact trench utility installations to ultra-large mining trunklines. Browse our standardized butt fusion machine product series below.
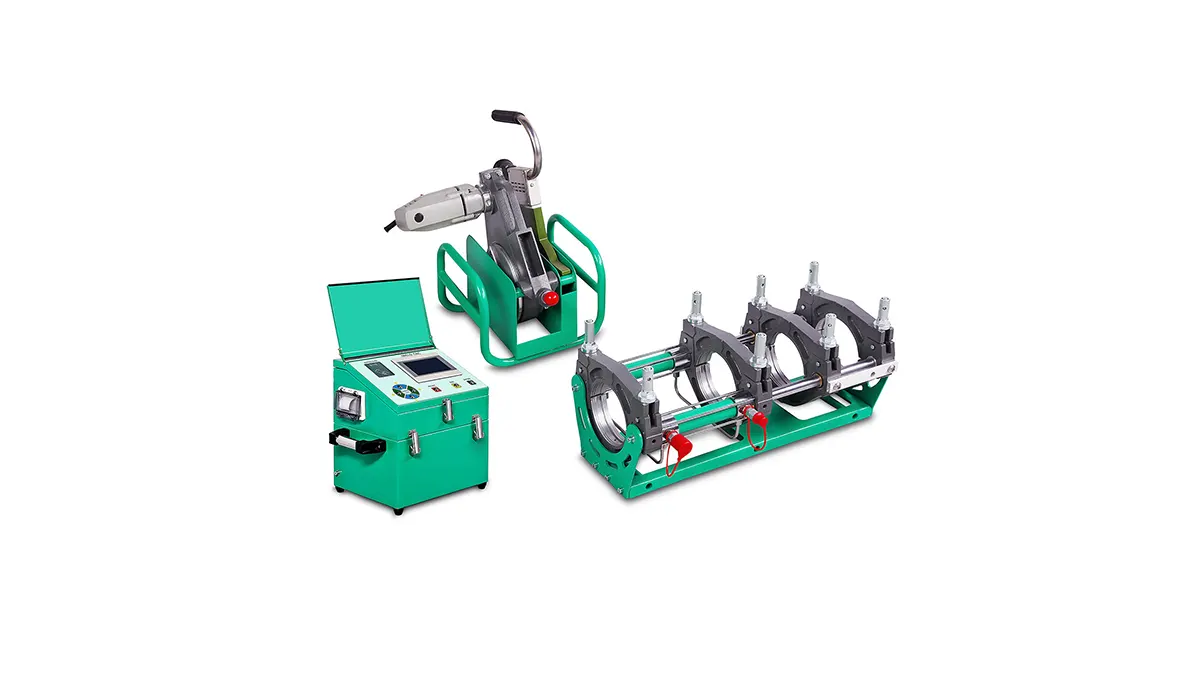
Hydraulic Welder with Aluminum Clamps
Ultra-lightweight die-cast aluminum clamp frames engineered for rapid field reconfiguration and high torsional strength.
View Specifications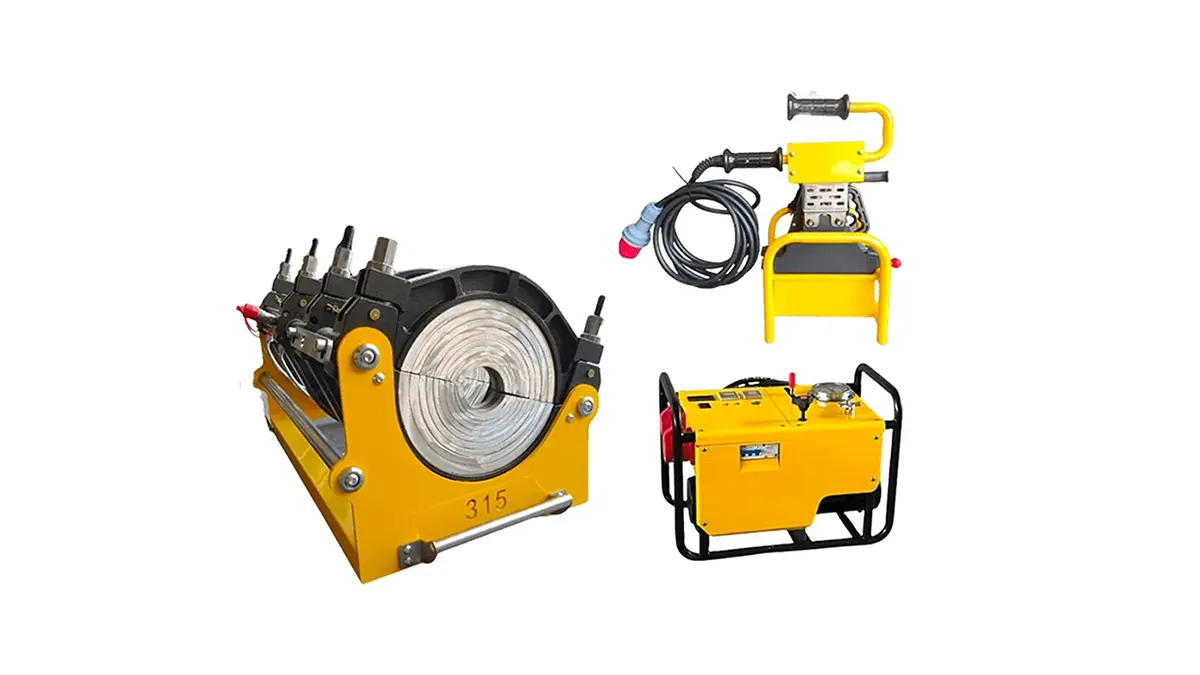
JQH315mm Hydraulic Fusion Machine
Designed for 90mm-315mm PE/PP pipes. Standard workhorse for regional water distribution and natural gas main lines.
View Specifications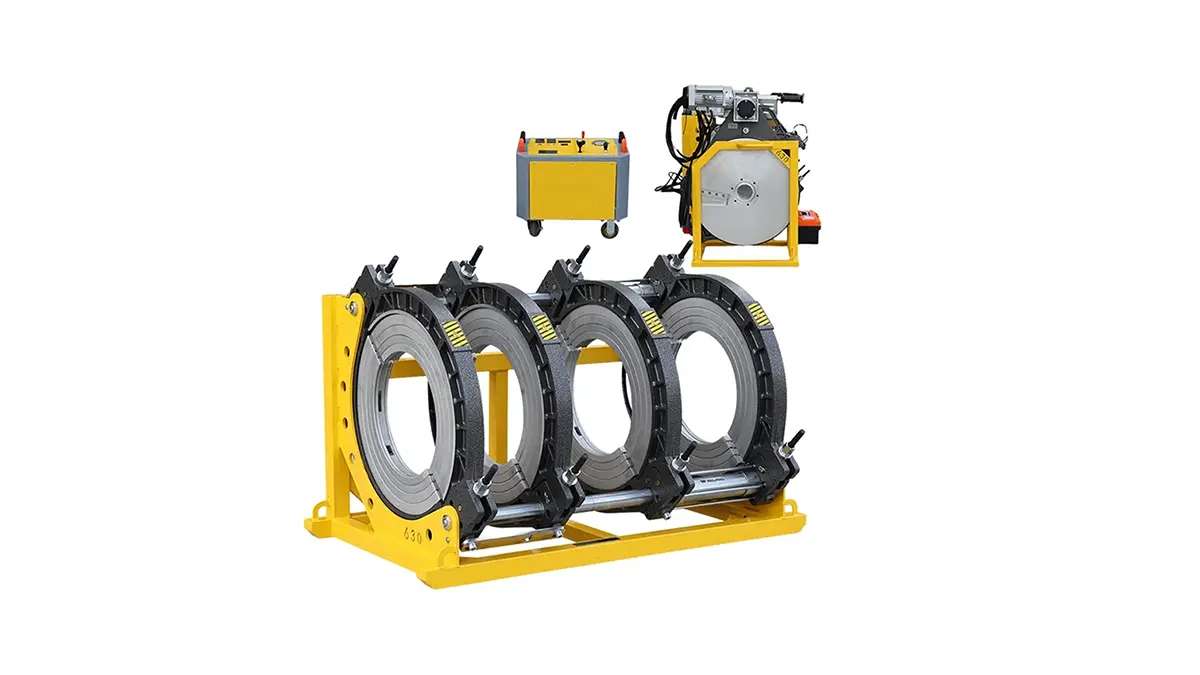
JQH630mm Hydraulic Butt Welder
Covers 315mm to 630mm pipeline segments. High-output hydraulic cylinders with pressure-maintenance accumulator.
View Specifications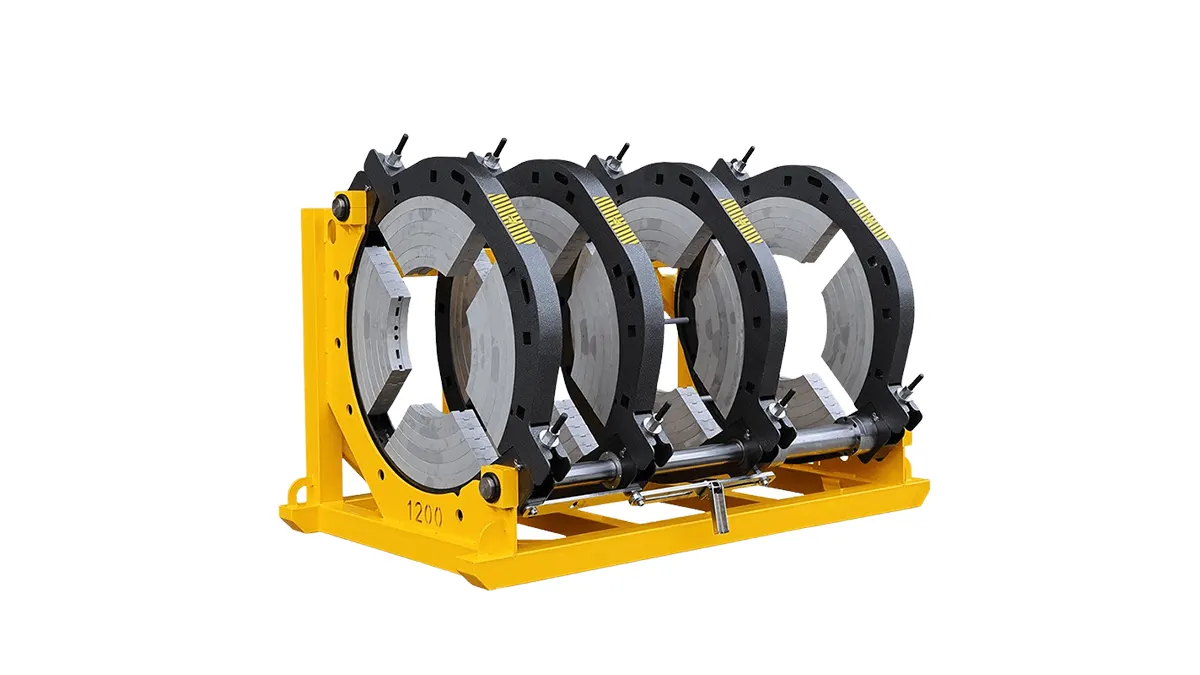
JQH1200mm Hydraulic Butt Welder
Built for 630mm to 1200mm heavy transmission lines, industrial outfalls, and thermal plant cooling intake piping.
View Specifications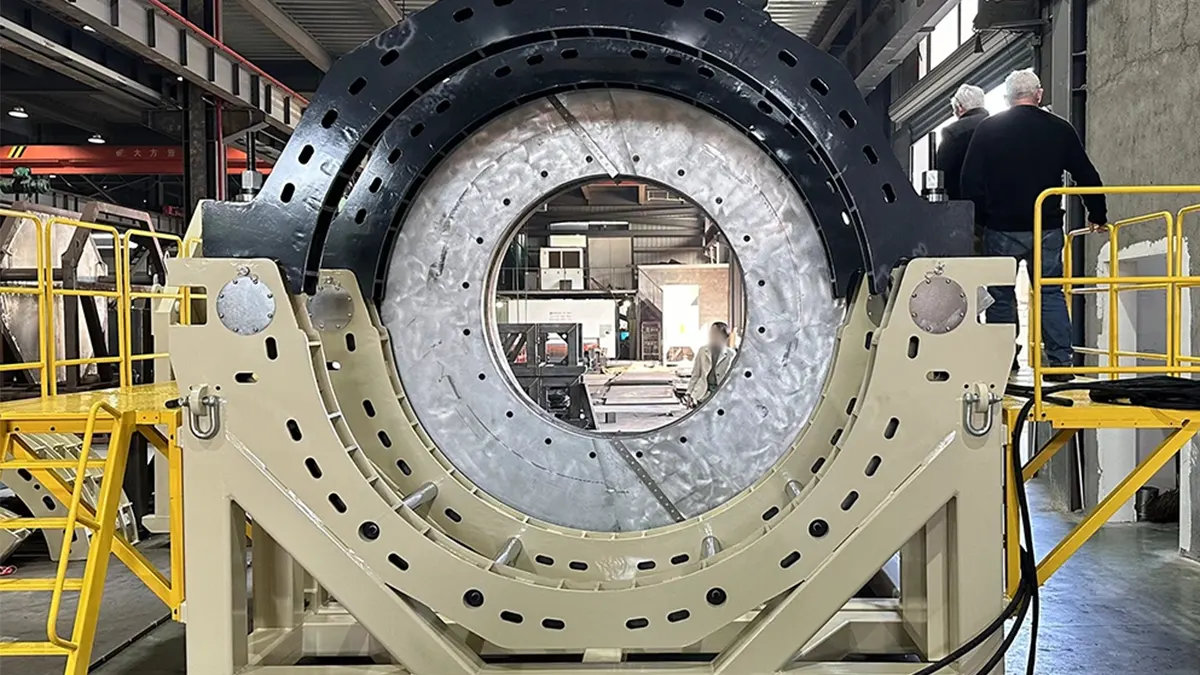
JQH2250mm Massive Bore Welder
Flagship hydraulic machine engineered for up to 2250mm diameter mega-projects, intake/outfall pipelines, and mining slurry.
View Specifications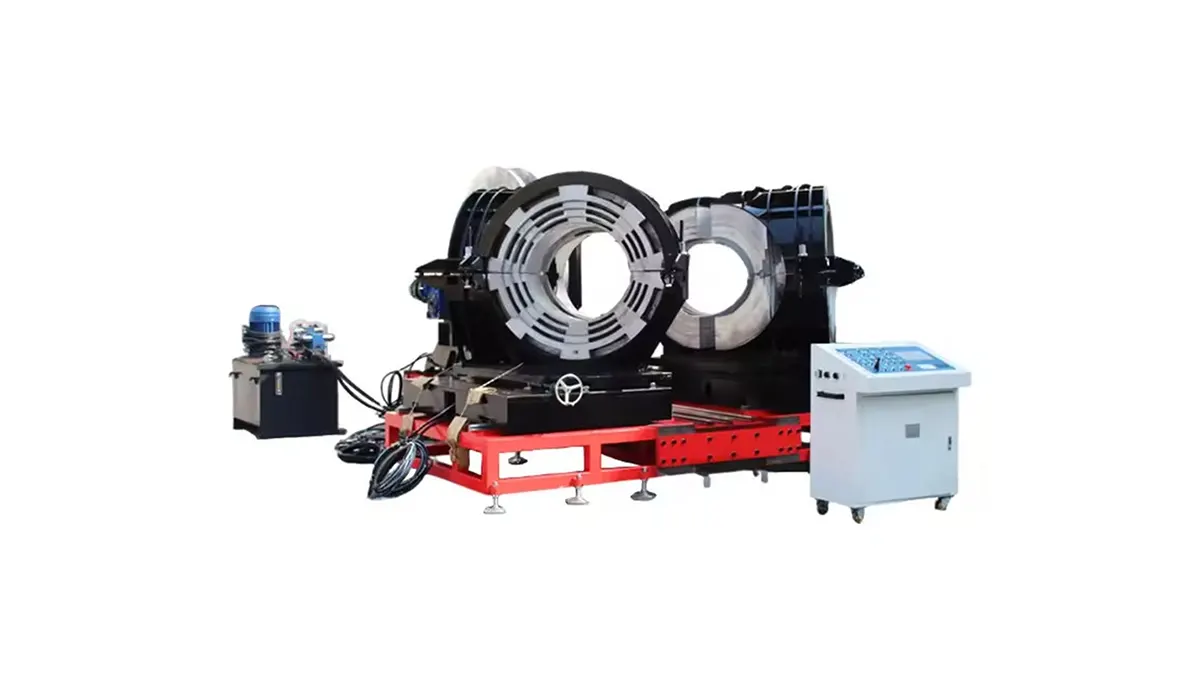
JQMA630 Multi-Angle Fitting Machine
Specialized workshop fitting machine for fabricating elbows, tees, crosses, and wyes according to butt-fused PE fittings standards.
View SpecificationsHydraulic Butt Fusion Machine Specifications
Explore the primary engineering data for JQ-Fusion standard hydraulic series. Each system can be equipped with custom clamping inserts, data loggers, or upgraded to full CNC automatic butt fusion welding machines.
| Model Series | Welding Range (OD mm) | Standard Inserts (mm) | Max. Hydraulic Pressure | Total Power (kW) | Operating Voltage | Applicable Materials |
|---|---|---|---|---|---|---|
| JQH160 | 63mm – 160mm | 63, 75, 90, 110, 125, 140, 160 | 6.3 MPa | 2.75 kW | 220V / 50-60Hz | PE, PP, PVDF |
| JQH250 | 90mm – 250mm | 90, 110, 125, 140, 160, 180, 200, 225, 250 | 6.3 MPa | 4.85 kW | 220V / 380V | PE, PP, PVDF |
| JQH315 | 90mm – 315mm | 90, 110, 140, 160, 180, 200, 225, 250, 280, 315 | 6.3 MPa | 5.85 kW | 380V / 50-60Hz | PE100, PE80, PP |
| JQH500 | 250mm – 500mm | 250, 280, 315, 355, 400, 450, 500 | 8.0 MPa | 9.50 kW | 380V / 50-60Hz | PE, PP, HDPE |
| JQH630 | 315mm – 630mm | 315, 355, 400, 450, 500, 560, 630 | 8.0 MPa | 12.35 kW | 380V / 50-60Hz | PE100, HDPE, PP |
| JQH1200 | 630mm – 1200mm | 630, 710, 800, 900, 1000, 1200 | 16.0 MPa | 28.5 kW | 380V / 3-Phase | HDPE, PE100 |
| JQH2250 | 1600mm – 2250mm | 1600, 1800, 2000, 2250 | 20.0 MPa | 75.0 kW | 380V / 415V 3-Phase | HDPE PE100 High SDR |
The 5-Stage Hydraulic Butt Fusion Sequence
Executing reliable PE welds demands adherence to calibrated thermal cycles. According to what is HDPE butt fusion guidelines and PE butt fusion process specifications, our hydraulic system guides the operator through five controlled steps:
Planing & Facing
Pipe ends are planed simultaneously using the motorized milling cutter to remove oxidation and establish parallel joining surfaces.
Alignment & Drag
High-low misalignment is verified (<10% wall thickness). Hydraulic drag pressure is measured and added to nominal interfacial pressure.
Heating & Bead Up
The PTFE heating plate (200°C–230°C) is inserted. Initial bead formation is established under pressure, followed by low-pressure heat soak.
Changeover & Fusion
Heating plate is removed within minimal switchover seconds. Pipe ends are brought together under smooth, calculated fusion pressure.
Cooling Under Load
The joint is held under active hydraulic pressure for the full duration specified by standard tables before unclamping.
State-of-the-Art Production & Massive Inventory
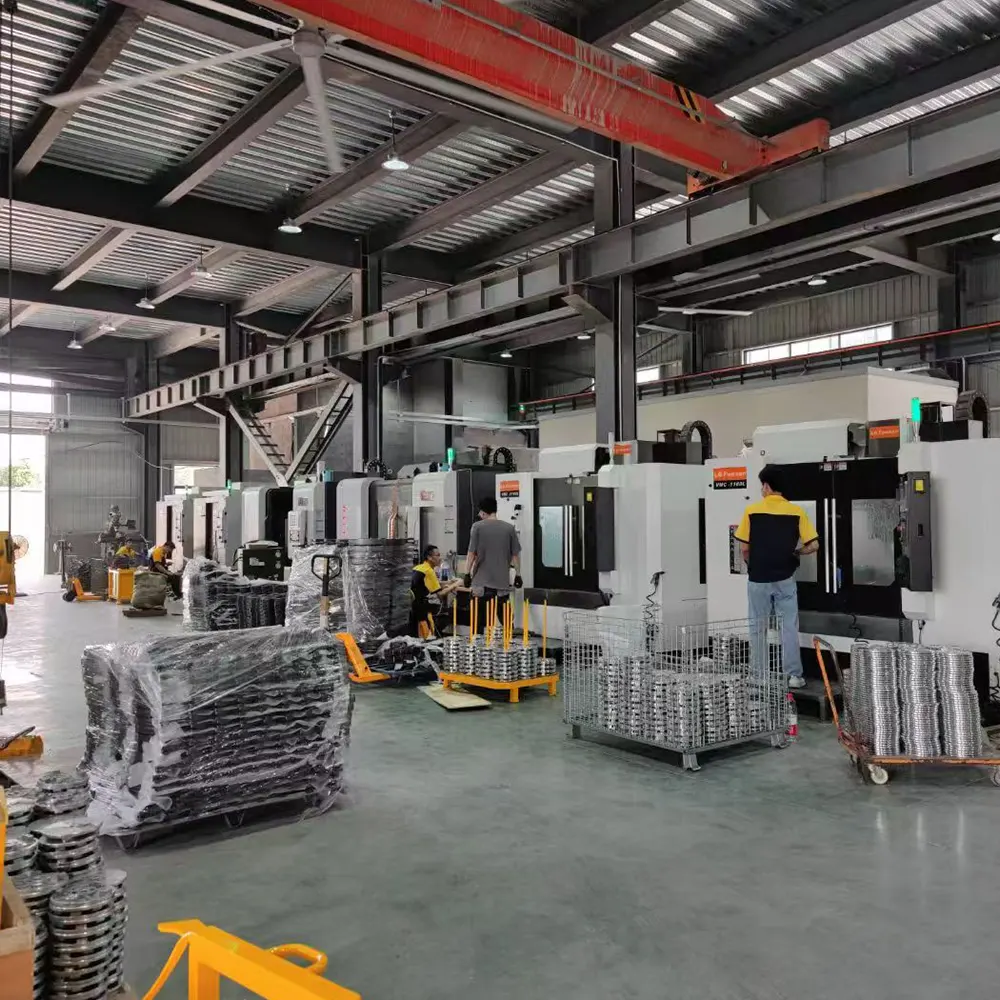
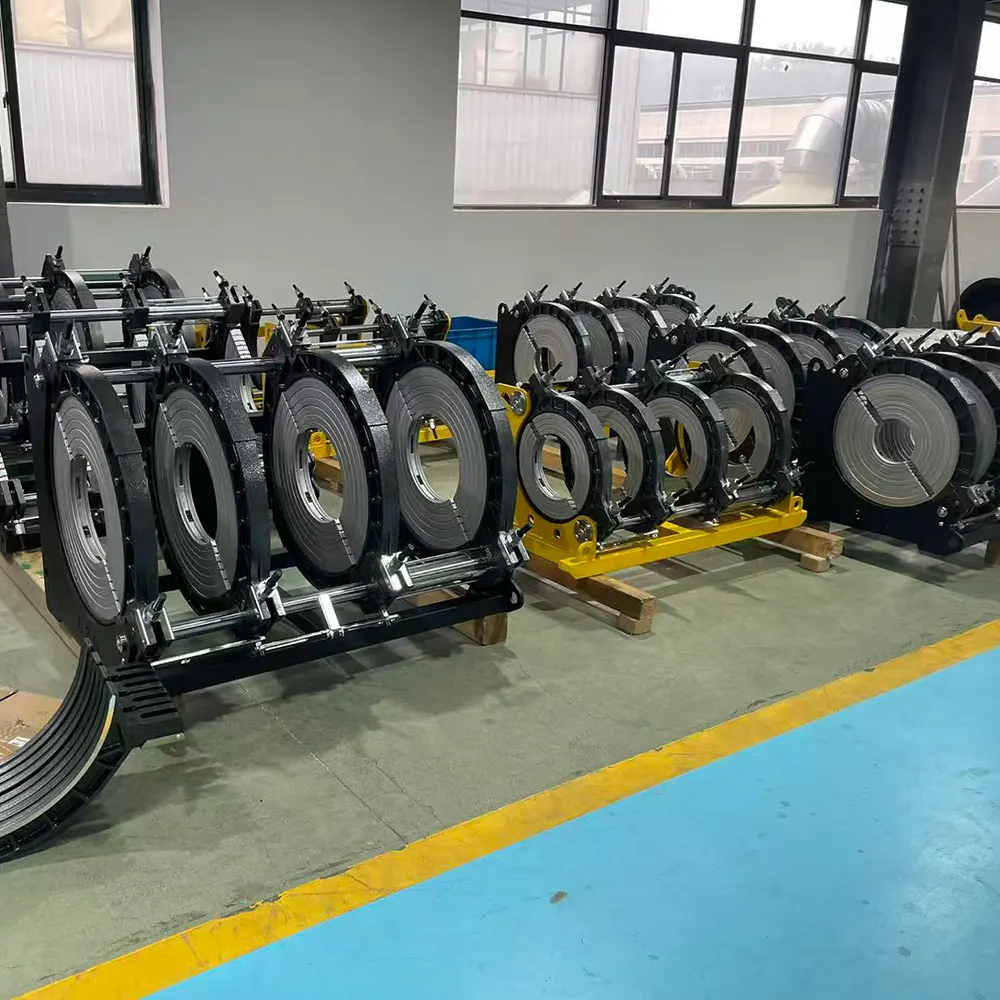
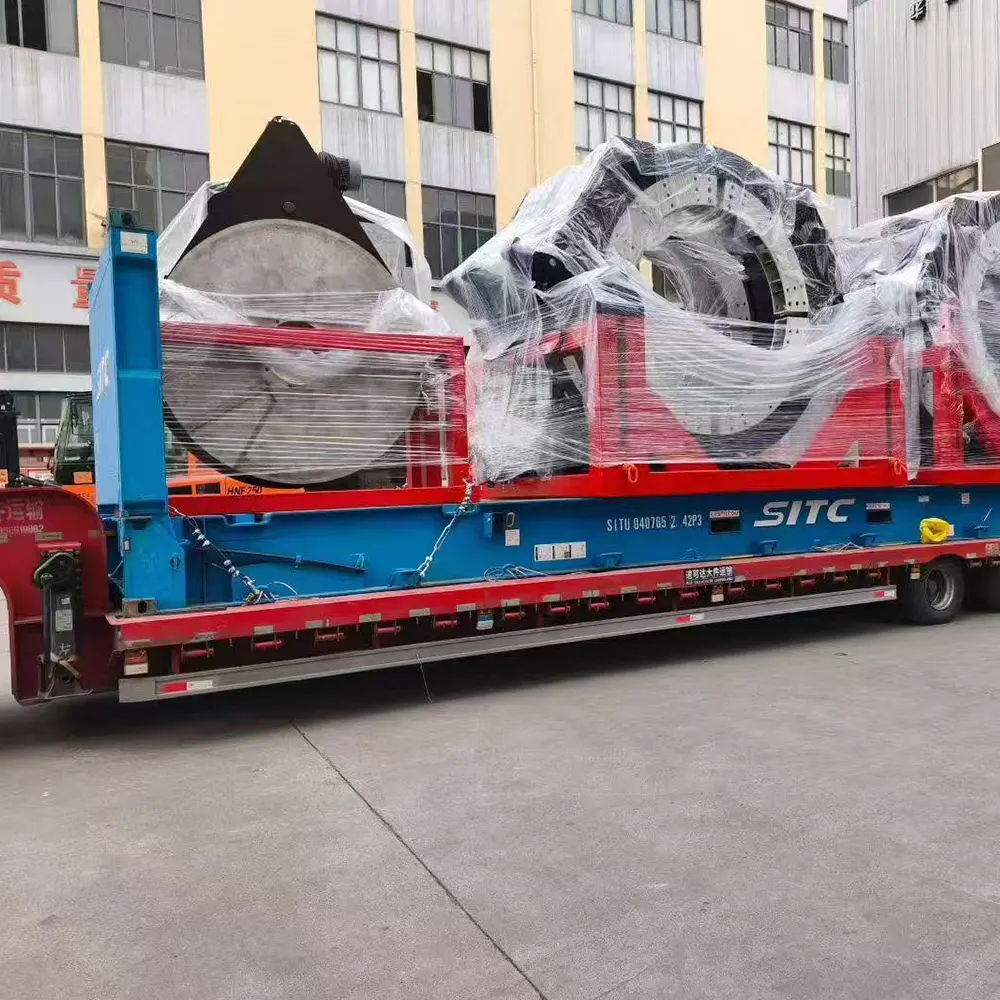
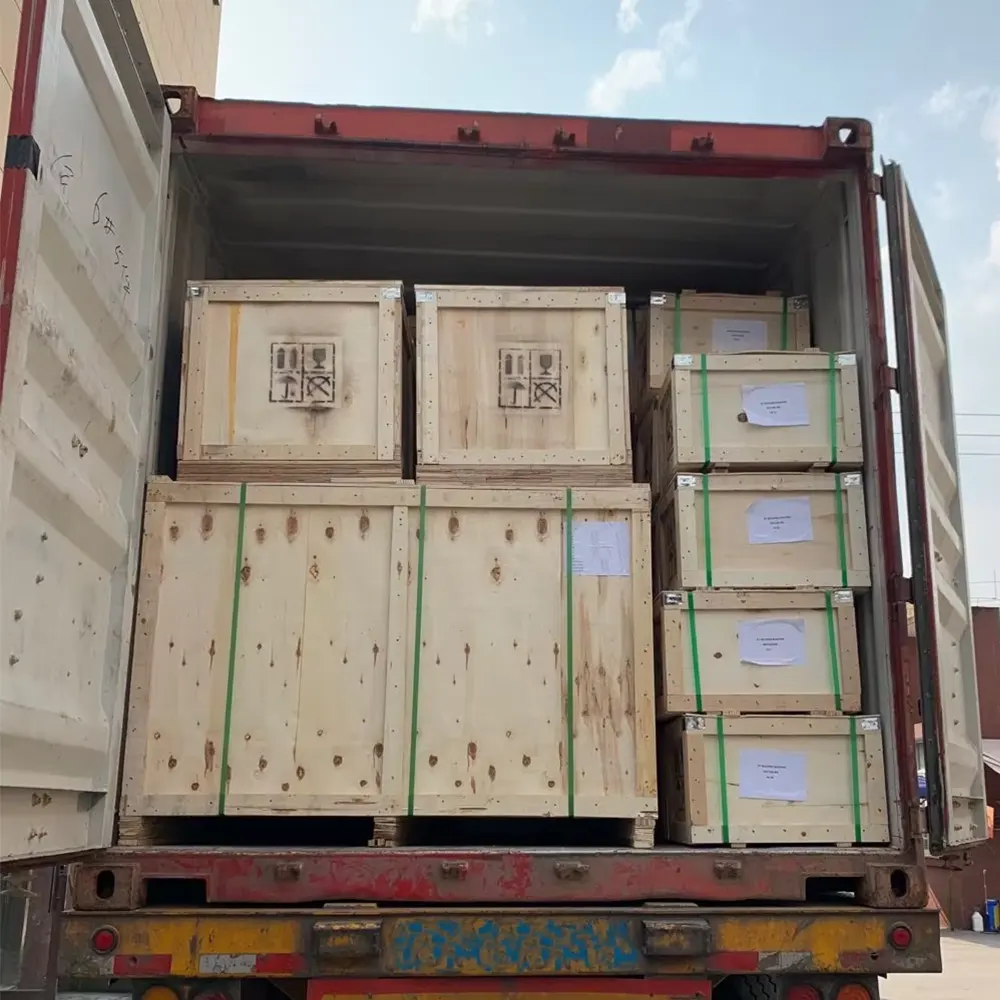
With large-scale precision machining centers and continuous production lines in Zhengzhou, Henan, JQ-Fusion maintains a consistent inventory of finished hydraulic butt welders and precision cast aluminum inserts. All machinery undergoes strict hydro-testing, electrical safety verification, and temperature uniformity audits before dispatch.
Global Quality Certifications
Meeting ISO, CE, and SGS international conformity benchmarks for global piping projects.
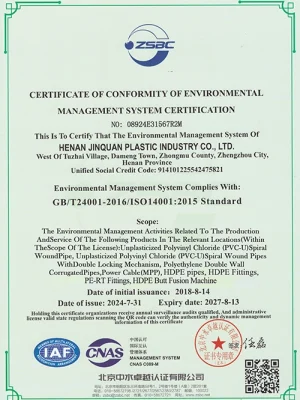
ISO 9001:2015 Quality Management
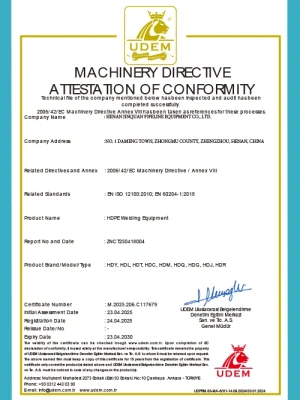
CE Machinery Compliance
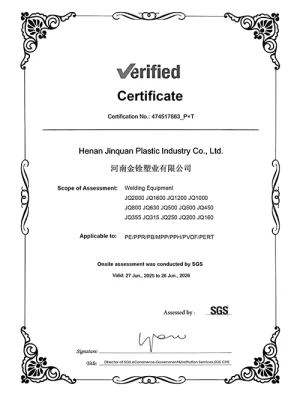
SGS Verified Manufacturer
Engineered for Harsh Pipeline Environments
Field conditions for pipeline contractors are rarely ideal. Whether dealing with desert dust, sub-zero trenching, or high-humidity marine conditions, our hydraulic PE pipe welding machines deliver consistent joint integrity.
Pressure-Retention Technology
Integrated hydraulic accumulators maintain seamless interfacial force throughout long cooling cycles without causing hydraulic pump overheating or power drain.
Full Traceability Compatibility
Equipped with communication interfaces ready for external data logging systems meeting PE fusion traceability ISO 12176-4 standards for public utility audits.
OEM & ODM Customization
We customize clamping insert sizes, machine brand colors, corporate tagging, and electronic languages for international equipment distributors and leasing fleets.
Infrastructure Powered by JQ-Fusion Machinery
Polyethylene pipelines have become the worldwide benchmark for leak-free, corrosion-resistant transport of water, gas, slurry, and chemicals. Our hydraulic fusion welders serve essential sectors across five continents:
Potable Water & Municipal
Connecting bulk supply mains and sewage interceptors conforming to ISO 4427 PE water pipes without mechanical couplers or gasket failures.
Natural Gas Distribution
Zero-leakage jointing for medium and high-pressure fuel networks compliant with ASTM D2513 PE gas pipe standards.
Mining & Slurry Transport
Heavy-duty, thick-wall PE100 butt fusion resisting aggressive slurry abrasion and chemical tailings in demanding mine sites.
Industrial & Marine Dredging
Corrosion-proof cooling pipes, desalination intakes, and marine dredging discharge strings compliant with industrial PE piping systems.
Expert Technical Guidance for Pipe Fusion
How is hydraulic welding pressure calculated for different pipe diameters?
Hydraulic gauge pressure ($P_{gauge}$) equals the theoretical interfacial fusion pressure ($P_{int}$, usually 0.15 MPa per ISO 21307) multiplied by the total annular cross-sectional area of the pipe, divided by the total effective area of the machine’s hydraulic cylinders, plus the measured dynamic drag pressure ($P_{drag}$).
Why is measuring drag pressure critical prior to each weld?
Drag pressure compensates for the physical frictional resistance of the heavy pipe resting on the ground or pipe rollers, as well as the internal friction of the machine carriage. Without adding drag pressure, the actual force applied to the melt zone will be insufficient, causing cold welds.
What is the difference between Hydraulic and Manual Butt Fusion?
While manual butt fusion machines rely on hand levers or screw gears for smaller pipes (≤160mm), hydraulic machines provide constant, measurable, and repeatable hydraulic clamping force necessary for larger diameters (≥160mm) and high SDR thick-wall pipes.
Can different PE pipe grades (PE80 and PE100) be joined together?
Yes, according to PE pipe compatibility guidelines, PE80 and PE100 pipes with similar melt flow rates (MFR 190°C/5kg between 0.2 and 1.4 g/10min) can be fused using standard parameters under qualified operator control.
Partner with an Experienced Fusion Machine Manufacturer
Ready to upgrade your pipeline jointing operations with high-precision hydraulic butt fusion equipment? Contact our engineering team for factory-direct quotations, technical parameter verifications, or custom OEM distribution partnerships.
- Email: [email protected]
- Phone / WhatsApp: +86 15093385787
- Headquarters: Zhengzhou, Henan Province, China