High-Performance HDPE Pipe Welding Equipment for Zero-Leak Joints
Engineered for extreme environmental resilience and micron-level mechanical alignment. Discover world-class butt fusion welding machines, CNC automatic systems, and electrofusion technology certified to international ISO 21307 butt fusion procedures and ASTM F2620 heat fusion protocols.
The Metallurgy of Polyethylene: Creating Homogeneous Monolithic Pipelines
High-Density Polyethylene (HDPE 100 / PE 100-RC / PE 4710) jointing relies on precise thermal chain entanglement rather than simple bonding. When executed with dedicated HDPE pipe welding equipment, the resulting weld zone exhibits tensile and burst characteristics equivalent to or exceeding the original pipe wall.
Thermodynamic Chain Interdiffusion
During the heating phase (200°C–230°C depending on ISO 21307 criteria), polymer crystals melt into an amorphous state. Controlled interfacial pressure forces the semi-crystalline chains across the interface to interlock, forming a uniform molecular matrix devoid of structural boundaries.
Interfacial Pressure Dynamics
Precision hydraulic valving ensures exact compliance with PE butt fusion process specifications. Accurate calculation of pipe cross-sectional area against hydraulic cylinder area prevents under-melt porosity and avoids excessive flash squeeze-out that weakens the joint root.
Cooling Kinetics & Recrystallization
Controlled in-clamp cooling under designated holding pressure is vital. Premature unclamping or artificial quenching induces thermal residual stresses and void formation. Our machines enforce strict cooling cycles adhering strictly to ASTM F2620 guidelines.
Industrial Butt Fusion & Jointing Machine Classifications
JQ-Fusion manufactures a broad spectrum of fusion joining systems, engineered to satisfy high-pressure pipeline integrity demands from compact municipal service lines to massive 2500mm transmission headers.
Hydraulic Butt Fusion Welding Machines
Engineered for trench and cross-country infrastructure, our hydraulic systems leverage high-strength cast aluminum clamps and rapid-coupling hydraulic power units. Ideal for water utilities conforming to ISO 4427 PE water pipes and gas systems conforming to ISO 4437-1.
- Pressure range up to 160 bar with non-leak quick-disconnect valving.
- Independent high-precision temperature control for PTFE-coated heating mirrors.
- Available for diameters from 160mm up to 2250mm extra-large pipes.
Working Size Range: 160mm – 2250mm (DN160 to DN2250)
Heater Max Temp: 270°C with digital PID loop control (±3°C variance)
Chassis Structure: Rigid torsional steel frame with reinforced 4-clamp setup
Standard Compatibility: Meets ISO 12176-1 and DVS 2207-1
Typical Applications: Long-distance water conveyance, industrial outfalls, mining slurries.
CNC Automatic Butt Fusion Systems
Automated fusion units eliminate human error by locking down fusion parameters. The CNC controller calculates interfacial pressure, monitors ambient temperature, tracks heat soak, and records every weld record according to PE fusion traceability protocols.
- Pre-programmed standards: ISO 21307 High/Low Pressure, ASTM F2620, DVS 2207-1.
- Built-in data memory logging over 2,000 fusion cycles with USB/Bluetooth export.
- Automatic heating plate ejection system reduces switchover time to milliseconds.
Standard Sizes: 160mm up to 630mm
Operator Verification: Barcode scanner and badge reader conforming to ISO 12176-3
Pressure Auto-Correction: Dynamic drag pressure sensing during each cycle
Audit Trail: Full PDF/Excel reporting with pass/fail quality criteria
Typical Applications: Natural gas transmission grids, nuclear cooling circuits, hazardous chemical lines.
Multi-Angle Pipe Fitting Fusion Machines
Designed specifically for workshop prefabrication of elbow, tee, cross, and wye fittings according to butt-fused PE fittings specifications. Provides flawless mitre cutting and jointing under strict factory conditions.
- Fabricate 0° to 90° elbows, 45° and 60° equal and reducing tees and crosses.
- Equipped with specialized clamping jigs to eliminate fitting ovality and wall thinning.
Available Diameters: 315mm, 450mm, 630mm, 800mm, 1200mm, 1600mm
Fitting Types: Segmented Bends, Equal Tees, 45°/60° Y-branches, Crosses
Structure: Integrated heavy steel bed with sliding linear guides
Compliance: ISO 4427-3, ISO 4437-3, ASTM F2206 standard fabricated fittings.
Electrofusion & Manual Butt Fusion Equipment
For tie-ins, repairs, and confined urban trenches where butt fusion rigs cannot maneuver, our electrofusion units (ASTM F1290 electrofusion) deliver precise voltage control, while manual screw-type and lever-type butt welders provide ultra-portable service line jointing.
- Electrofusion units with optical scanner reading 24-bit barcode standards.
- Manual butt welders with compact two-ring and four-ring lightweight chassis.
Electrofusion Output: 8V – 48V stabilized voltage, up to 3.5kW – 4.5kW output
Manual Welder Sizes: 40mm – 160mm / 63mm – 200mm / 90mm – 250mm
Portability: Handheld & backpack transport options for mountain & tight city civil works
Compatibility: Couplers, saddles, tapping tees compliant with ASTM F1055 electrofusion fittings.
Featured Heavy-Duty Butt Fusion & Workshop Welding Units
Browse our most widely specified HDPE pipe welding equipment models, proven across global municipal, gas grid, trenchless HDD, and offshore operations.
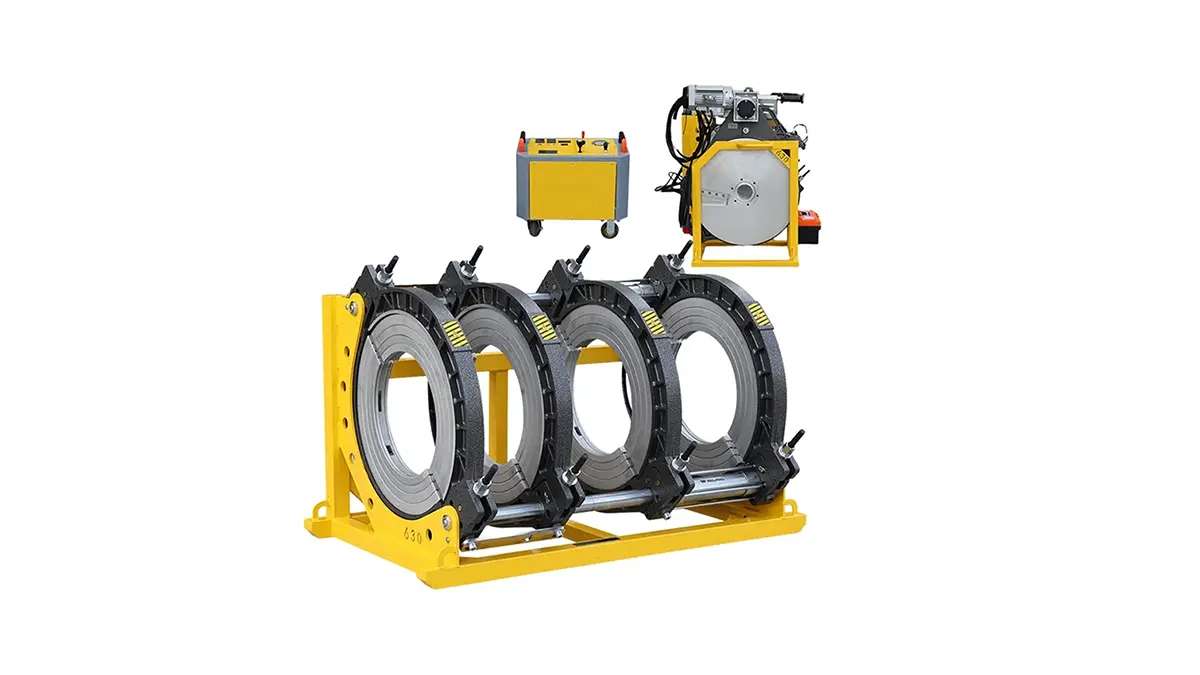
JQH630mm Hydraulic Butt Fusion Machine
Power: 12.35 kW | Voltage: 380V
Application: Main trunk potable water & industrial outfall lines.
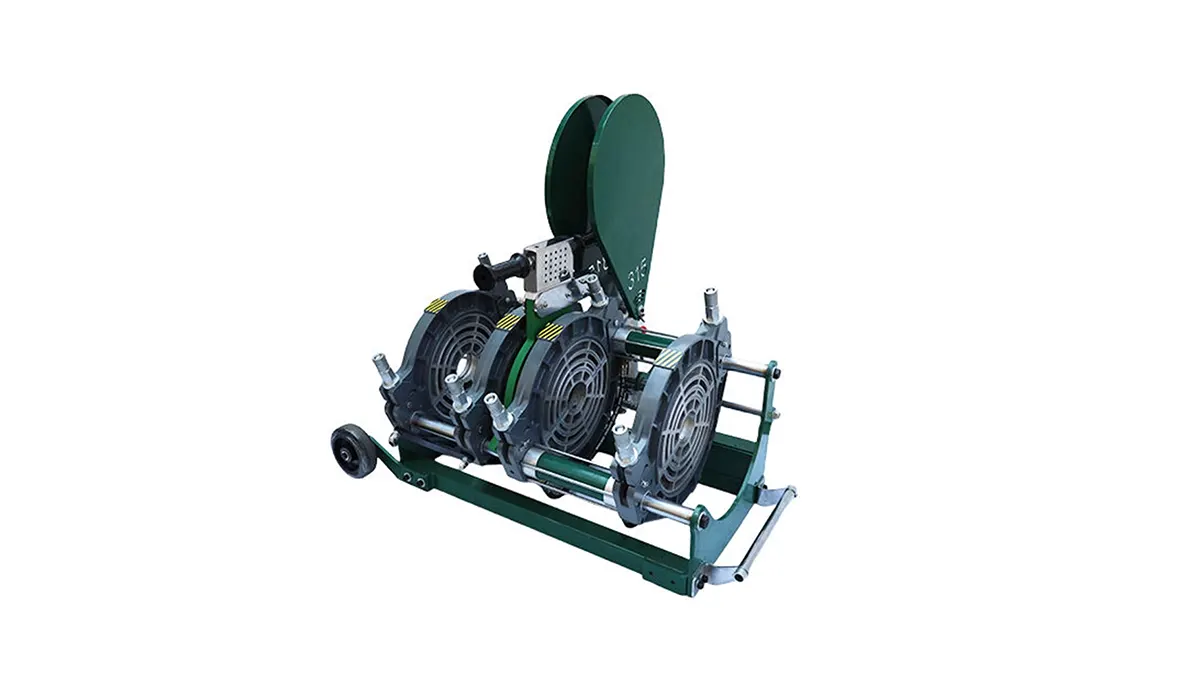
JQA315mm CNC Automatic Butt Fusion Welder
Features: Auto data logging & GPS
Application: High-pressure natural gas & hazardous fluids.
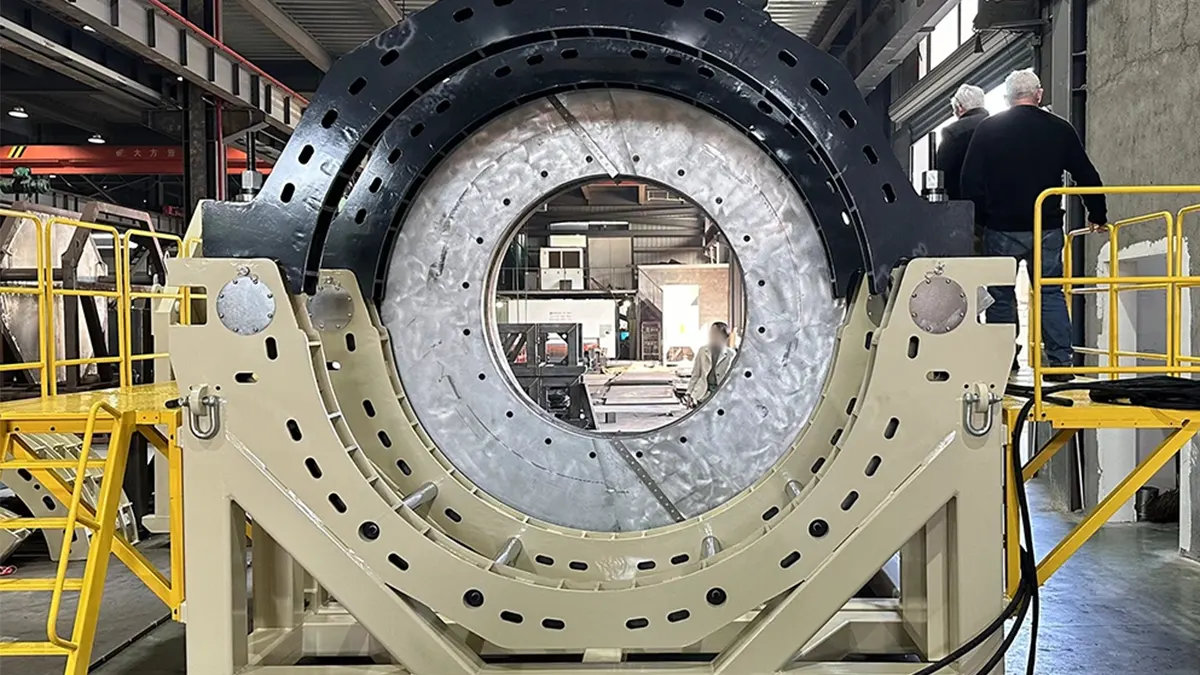
JQH2250mm Ultra-Large Hydraulic Fusion Machine
Features: Heavy crane hoist & dual ram
Application: Deep sea intakes, mega mining conduits.
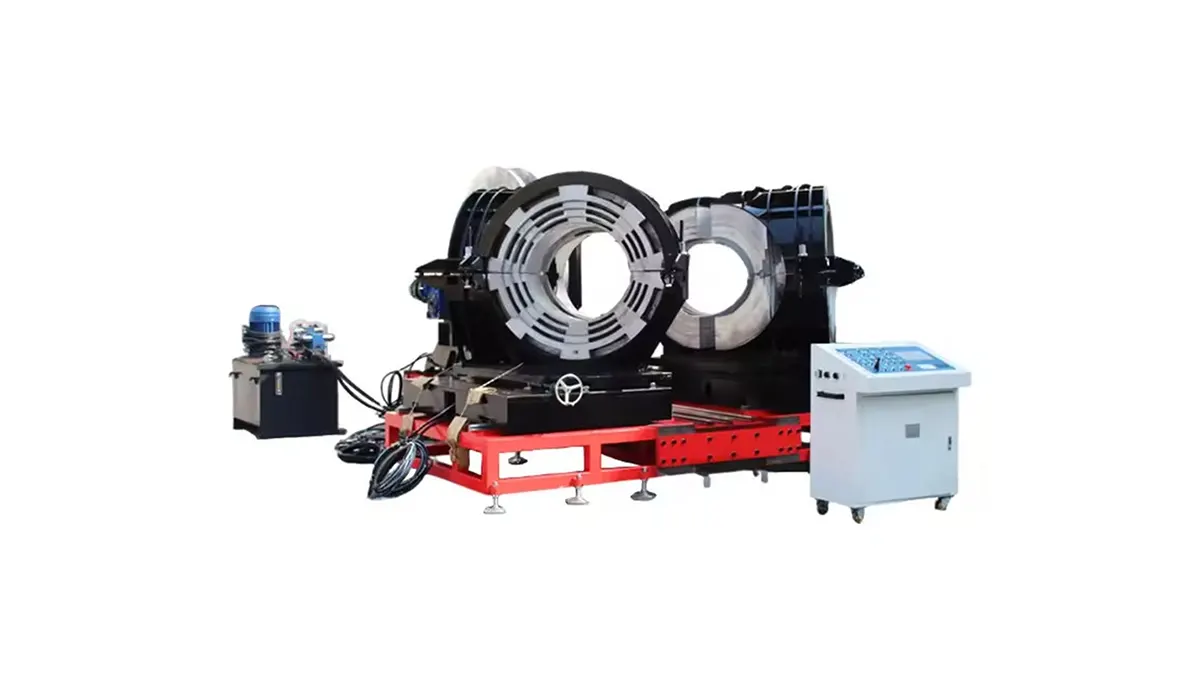
JQMA630 Multi-Angle Fitting Fabricator
Fitting Types: 90° Elbows, Tees, Crosses
Application: Factory workshop pre-fabrication.
Equipment Evaluation: Manual vs Hydraulic vs CNC Automatic vs Electrofusion
Selecting the appropriate HDPE pipe welding equipment depends on project pressure ratings, diameter scope, environmental constraints, and quality compliance mandates.
| Technology Type | Applicable Pipe Range | Joint Efficiency | Data Traceability | Operator Dependency | Primary Standard Compliance |
|---|---|---|---|---|---|
| Hydraulic Butt Fusion | 160mm – 2500mm | 100% (Full Strength) | Manual Gauge / Optional Logger | Medium | ISO 21307, ASTM F2620, DVS 2207 |
| CNC Automatic Butt Fusion | 160mm – 630mm | 100% (Certified Repeatable) | Integrated Automatic Data Recording | Low (Error-Proof Interlock) | ISO 12176-1, ISO 21307, PHMSA Safety Rules |
| Workshop Multi-Angle Machine | 315mm – 1600mm | 100% (Factory Fabricated) | Digital Angle & Pressure Record | Medium | ASTM F2206, ISO 4427-3 |
| Electrofusion Control Box | 20mm – 800mm | 95% – 100% (Coupler Bound) | Barcode Scanner Traceability | Low to Medium | ISO 12176-2, ASTM F1290 |
| Manual Butt Fusion | 40mm – 250mm | 90% – 100% (SDR Dependent) | Manual Inspection Checklist | High | DVS 2207, Local Low-Pressure Guidelines |
1. Bead-Up & Drag Compensation
Continuous dynamic monitoring of drag pressure ($P_{text{drag}}$) is mandatory. True fusion gauge pressure must equal theoretical fusion pressure plus line drag to avoid cold joints.
2. Heat Soak & Low-Pressure Transition
Zero-pressure contact during soaking allows uniform heat depth without squeezing out the melted cushion. Plate removal must take < 5 to 10 seconds to avoid oxidation.
3. Pressure Cooling Under Clamping
Cooling must occur strictly under full fusion pressure until the weld core drops below crystalline transition temperature, verified via PPI technical guidance.
Where Joint Integrity Is Non-Negotiable
Modern infrastructure projects rely on continuous, leak-free polyolefin pipelines. JQ-Fusion equipment powers mission-critical pipelines worldwide.
Municipal Water & Desalination
Butt-fused HDPE pipelines eliminate joint infiltration and exfiltration in drinking water supply, conforming strictly to PE pressure pipe standards and AWWA C906. Smooth inner bores reduce head loss and energy consumption.
Natural Gas Distribution Grids
Gas distribution demands zero failure tolerance. Our CNC butt fusion and electrofusion systems comply with ASTM D2513 PE gas pipe and ISO 4437-2 regulations, guaranteeing comprehensive traceability for gas utilities.
Mining Slurry & Industrial Chemical Lines
Abrasive tailings and aggressive chemical processing lines rely on thick-walled (SDR 7 / SDR 9) PE100 pipes. Our hydraulic equipment provides massive clamping force to align heavy schedules without ovality or slip according to industrial PE piping systems standards.
Engineering Butt Fusion Excellence for Global Infrastructure
JQ-Fusion is an established global manufacturer dedicated to the design and precision engineering of HDPE pipe welding machines. Covering manual, hydraulic, and CNC automatic butt fusion systems from 40mm up to 2500mm diameters, we equip piping contractors, gas utilities, and industrial fabricators worldwide.
With strategic inventory hubs, specialized testing rigs, and rapid OEM/ODM design capabilities, our engineering teams ensure that your pipeline installations achieve zero-leak joint reliability every time. Learn more on our distributor partnership program or download our complete product catalog.
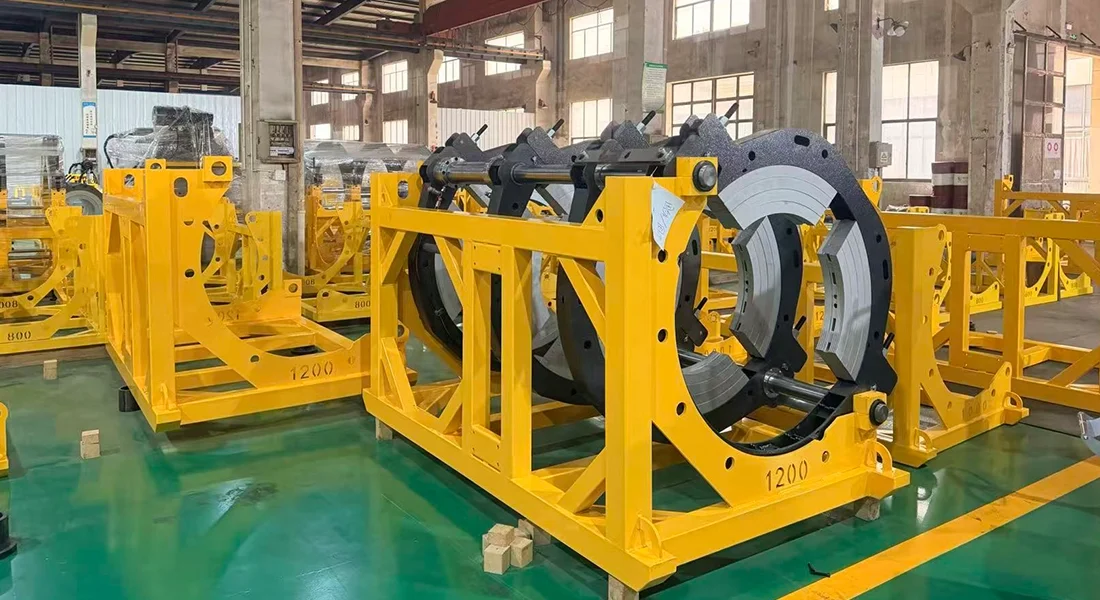
Certified Global Compliance
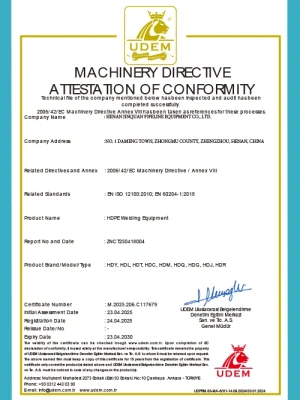
CE Machinery Safety Compliance
ISO 9001:2015 Quality Management
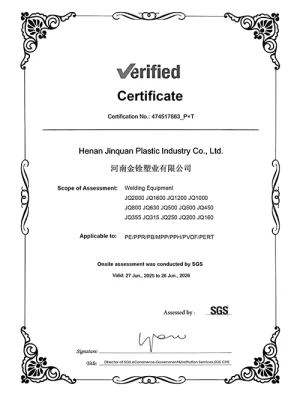
SGS Audited Manufacturing Standards
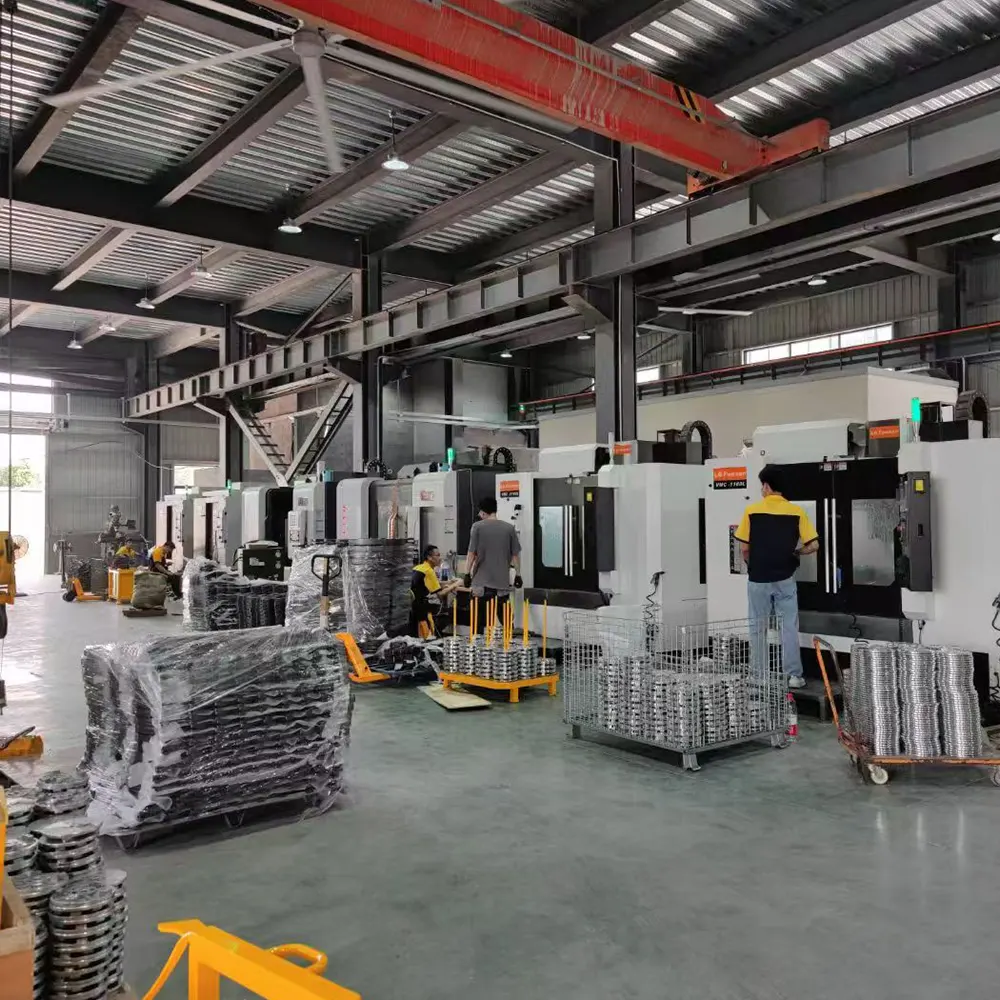
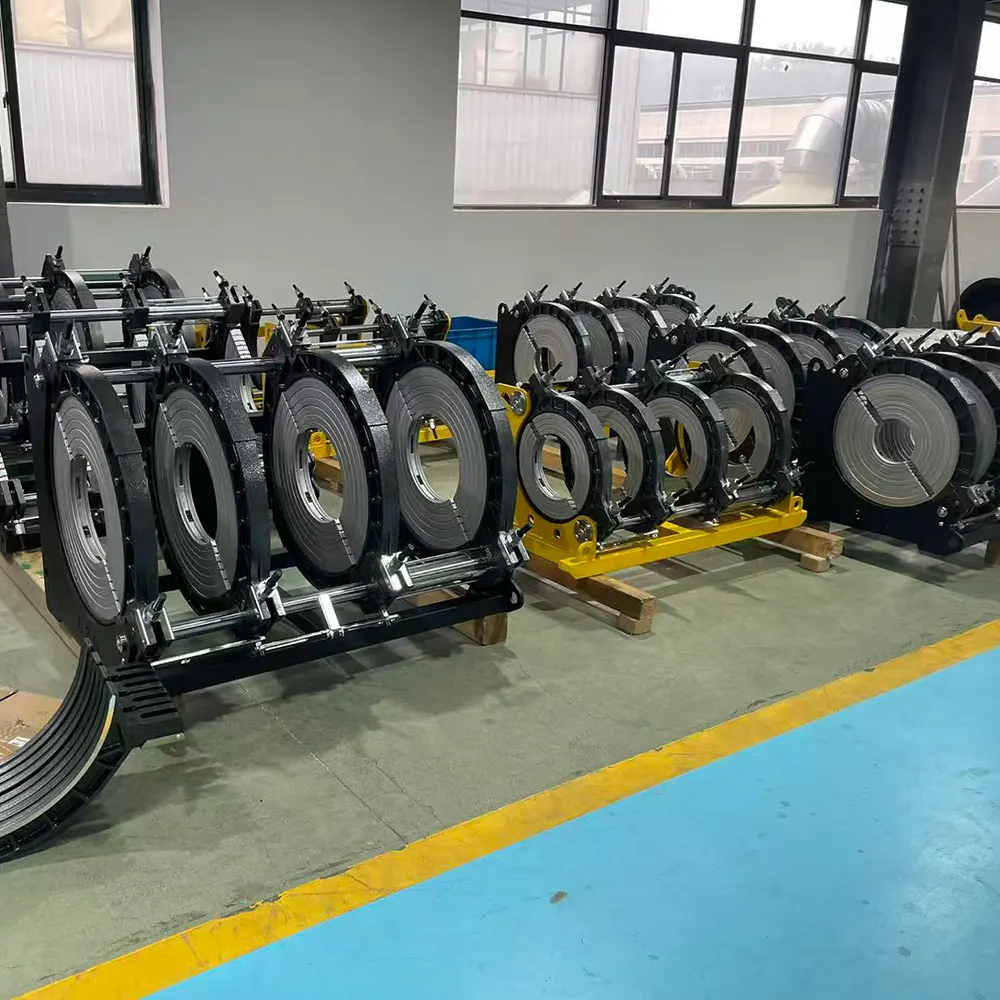
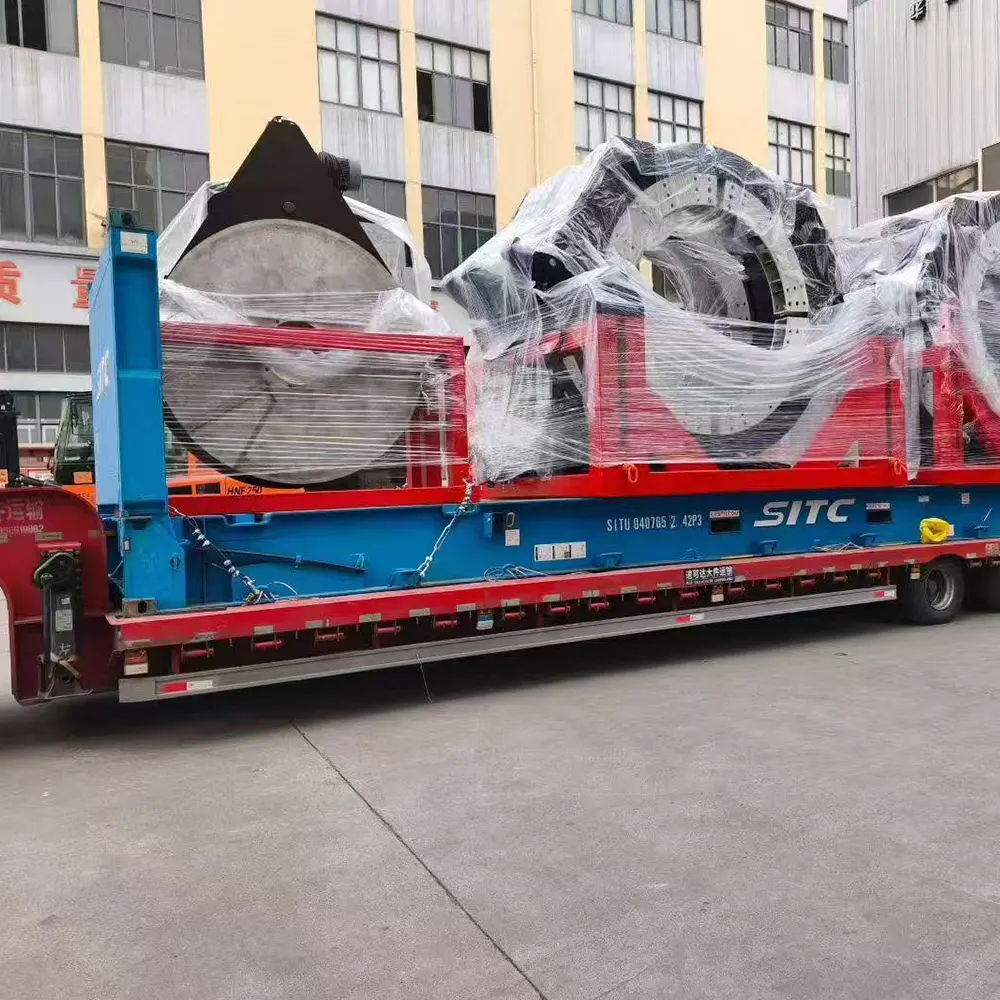
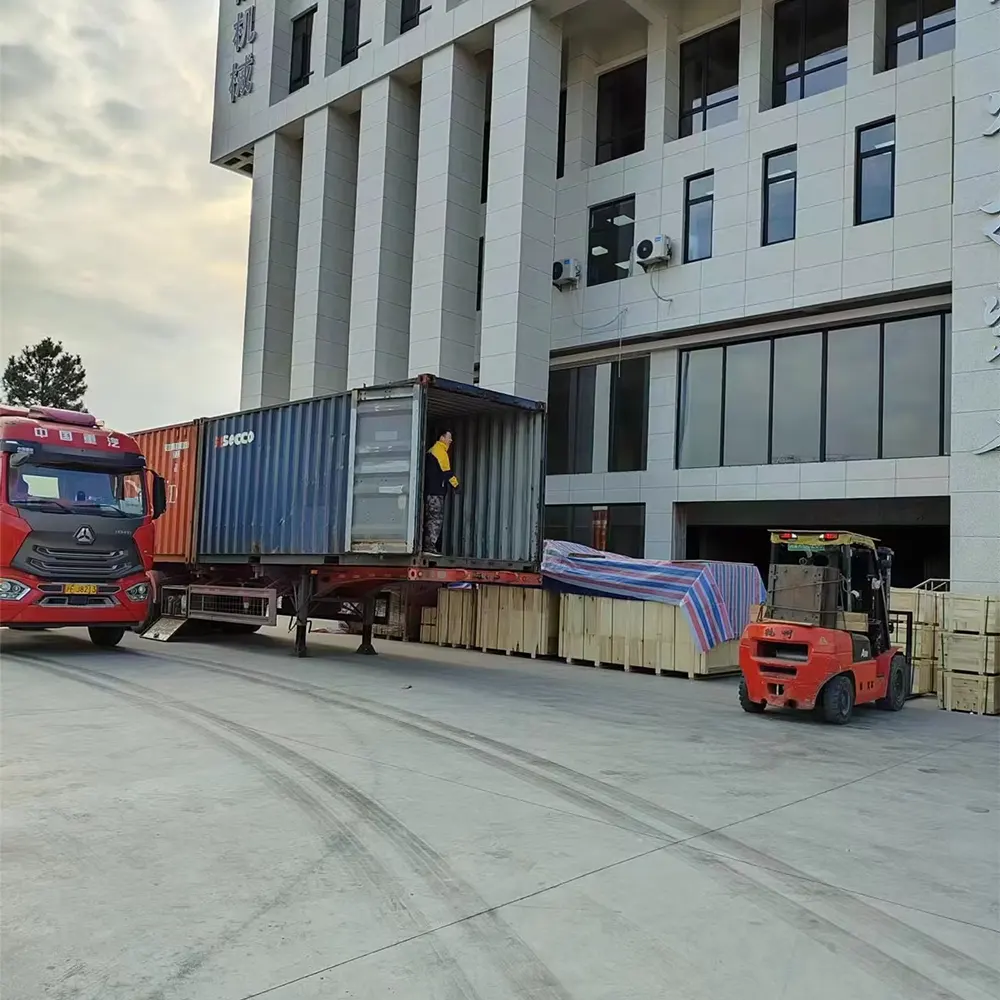
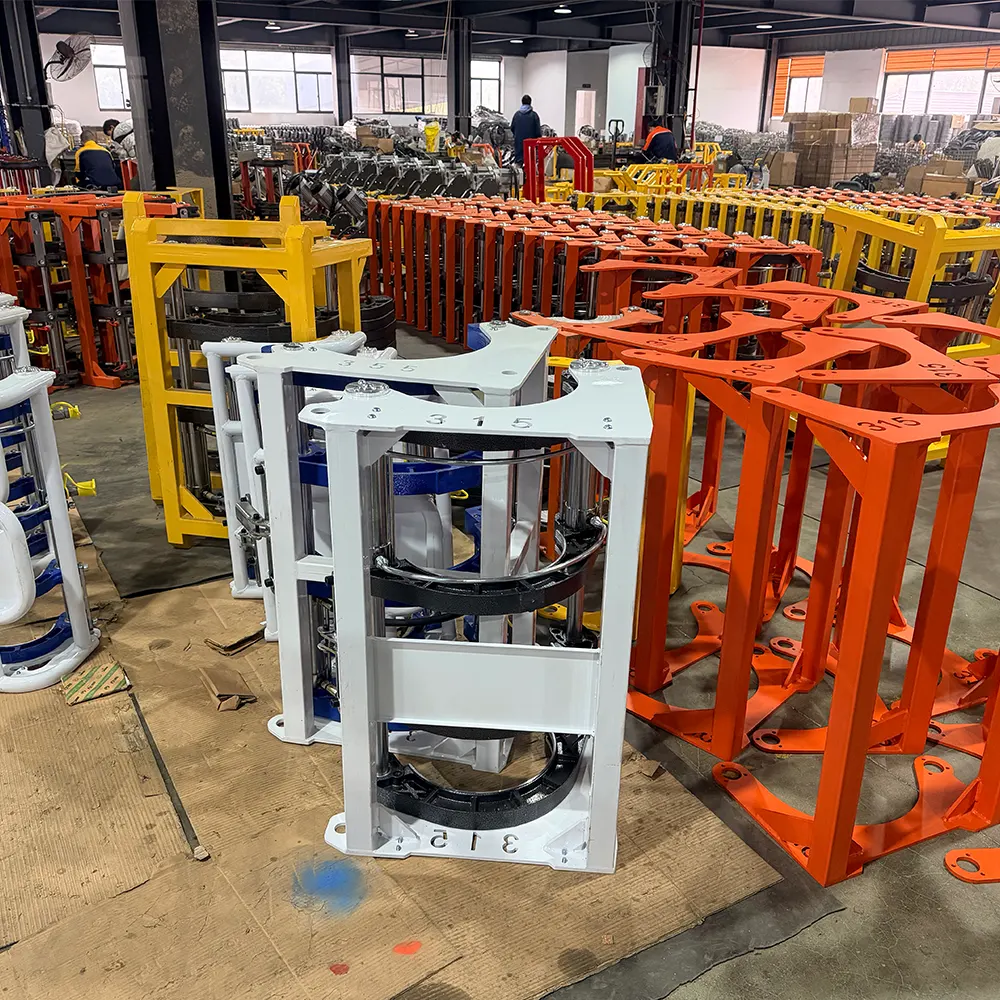
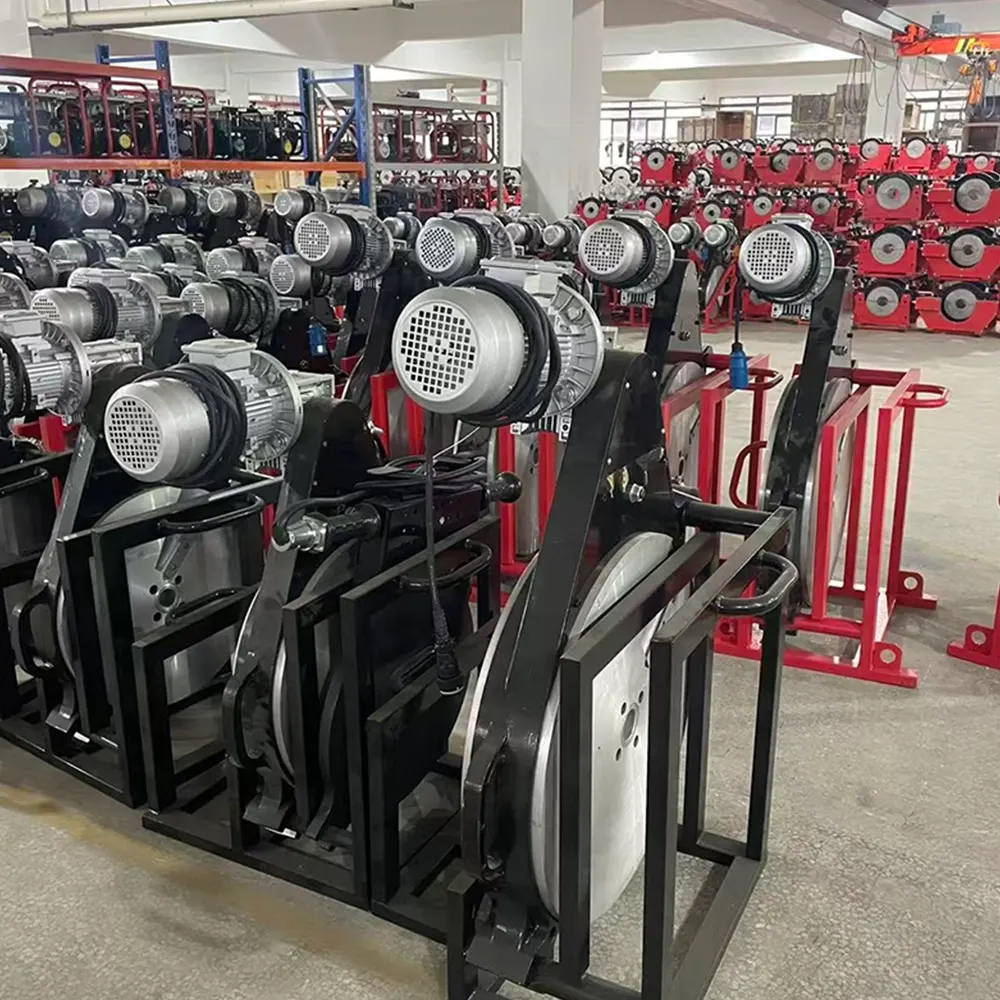
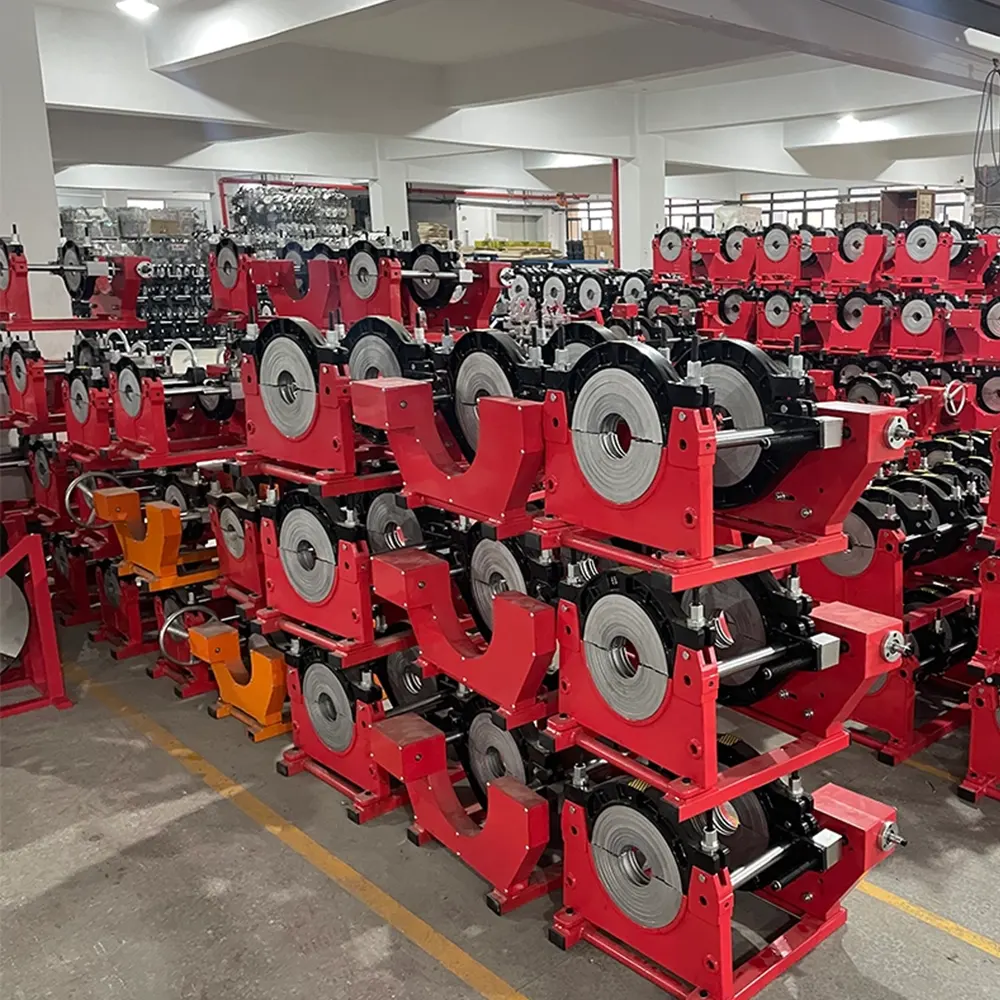
Ready-to-Ship Inventory & Modern Assembly Facility
Field Welding Workflow & Non-Destructive Quality Verification
Executing flawless butt welds demands rigorous adherence to qualified procedures. Follow these 4 essential stages defined by PE pipe jointing best practices.
Facing & Alignment
Clamp pipe ends, adjust high-low misalignment to <10% of wall thickness, and plane pipe faces until continuous shavings emerge on both sides.
Bead-Up Formation
Insert the heated PTFE plate (220°C ± 10°C). Apply calculated drag plus fusion pressure until a uniform melt bead appears around the entire pipe circumference.
Heat Soak & Rapid Dwell
Reduce pressure to zero for the heat soak duration. Rapidly open clamps, withdraw the heater, and bring pipe ends together within allowable switchover seconds.
Cooling & Hydrostatic Check
Maintain full fusion pressure throughout cooling. Perform external bead debagging and field pressure testing in accordance with ASTM F2164 leak testing.
Frequently Asked Questions & Engineering Consultation
Find quick answers regarding equipment selection, parameter calculation, and global delivery times. Contact our engineering team for instant support.
How do I calculate true fusion pressure on hydraulic machines?
True Gauge Pressure = (Interfacial Pressure × Pipe Annular Area / Hydraulic Cylinder Effective Area) + Drag Pressure ($P_{text{drag}}$). Drag pressure must be measured immediately before facing each joint to ensure full interfacial molecular contact.
Can different SDR ratings or PE grades be butt-welded together?
According to PE pipe compatibility guidelines, pipes with identical SDR (wall thickness) can be welded if their Melt Flow Rate (MFR) falls within 0.2 to 1.4 g/10 min. Different SDR pipes require machining or transition electrofusion fittings.
Do JQ-Fusion CNC welders support custom utility welding recipes?
Yes. While pre-loaded with ISO 21307, ASTM F2620, and DVS 2207-1 standards, our CNC systems permit password-protected custom parameters for specialized polymer blends like PE-RT or multi-layer pipes.
What is the standard lead time for export orders?
With our continuous inventory of standard models (160mm through 630mm hydraulic and CNC welders), dispatch can take place within 48 to 72 hours. Large-diameter machines (800mm to 2250mm) and custom-voltage models ship within 7–15 working days.
Contact JQ-Fusion
Our multilingual pipeline welding specialists and application engineers are on standby 24/7 to support your bidding, procurement, and technical queries.