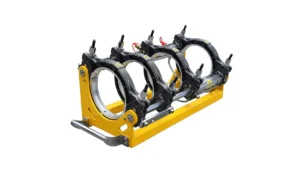
Demystifying Automatic Butt Fusion Systems in Modern HDPE Pipelines
High-Density Polyethylene (HDPE) has revolutionized modern utility networks, from high-pressure water mains to combustible gas distribution and industrial mining slurry lines. However, pipeline longevity is entirely dictated by joint integrity. An Automatic Butt Fusion Machine eliminates the critical risks of human error, manual miscalculations, and inconsistent thermal dwell times by leveraging high-speed microprocessors and electro-hydraulic feedback loops.
CNC Closed-Loop Architecture
Unlike traditional manual or standard hydraulic rigs, an automatic CNC welder dynamically samples actual cylinder drag, ambient humidity, and pipe temperature, automatically recalculating heating, soaking, changeover, and cooling pressures according to certified international standards.
Deterministic Joint Reliability
The automatic system prevents premature release during critical cooling cycles. Joint parameters cannot be manipulated on-site without supervisory override, guaranteeing strict adherence to ISO 21307 butt fusion procedures and regional engineering specifications.
Cloud-Ready Data Logging
Every weld cycle compiles a comprehensive cryptographic log including joint serial, heating plate surface temperature, peak bead-up pressure, drag compensation, and technician ID, complying thoroughly with PE fusion traceability protocols.
Automated 6-Phase Fusion Workflow
Understanding the sequence executed by an Automatic Butt Fusion Machine demonstrates why high-density piping contractors transition away from manual oversight. Every stage operates under strict mathematical tolerances:
Auto Drag & Facing
The system senses cylinder resistance (drag pressure) dynamically and adjusts the electric planer to mill square pipe ends, maintaining uniform shavings until flush contact is verified by optical sensors.
Bead-Up Formation
The heating mirror is positioned, and the hydraulic unit applies initial fusion pressure (Drag + Interfacial Pressure) until a consistent polymer melt bead forms uniformly around the pipe OD.
Heat Soak Dwell
Pressure automatically decays to soaking level (≤0.05 MPa), allowing thermal energy to permeate the pipe end walls without displacing molten polyethylene material.
Ultra-Fast Changeover
Automated clamps separate the carriage, the heating plate auto-ejects, and the carriage closes within specified milliseconds to prevent interfacial oxidation or premature cooling.
Joining & Ramping
The hydraulic system smoothly ramps joining pressure to the target value according to ASTM F2620 heat fusion or ISO specifications, creating homogenous molecular bonding.
Controlled In-Clamp Cooling
The machine locks pressure throughout the full cooling duration. Early removal triggers an audible fault and generates a failed weld certificate in the internal memory log.
Comparison: Manual vs. Hydraulic vs. CNC Automatic Butt Fusion
Evaluate how different machine classes align with project tolerances, safety standards, and QA/QC requirements across water and gas pipeline construction.
| Evaluation Parameter | Manual Butt Fusion | Standard Hydraulic Machine | CNC Automatic Butt Fusion Machine |
|---|---|---|---|
| Operator Dependency | Extreme (Subjective force/timing) | Moderate (Manual valve control) | Zero (Microprocessor controlled) |
| Pressure Calibration | Manual mechanical gauge | Analog/Digital hydraulic gauge | Closed-loop electronic sensor |
| Dynamic Drag Compensation | Not possible | Operator manual calculation | Automatic transducer sensing |
| Cooling Phase Enforcement | Manual stopwatch | Manual timer / Operator alert | Hardware clamp interlock |
| Traceability & Logging | Manual logbook handwriting | Optional external data recorder | Integrated ISO 12176-4 USB/Cloud |
| Joint Failure Risk Index | High (Human fatigue factor) | Moderate | Virtually Zero (<0.01%) |
| Primary Project Scope | Non-pressure drain & drainage | Standard water supply piping | High-pressure Gas, Slurry & Water |
Featured Automatic Butt Fusion Machines (JQA Series)
Explore JQ-Fusion’s heavy-duty CNC automatic butt fusion welding machines, engineered for field ruggedness and surgical fusion accuracy from 50mm up to 630mm.
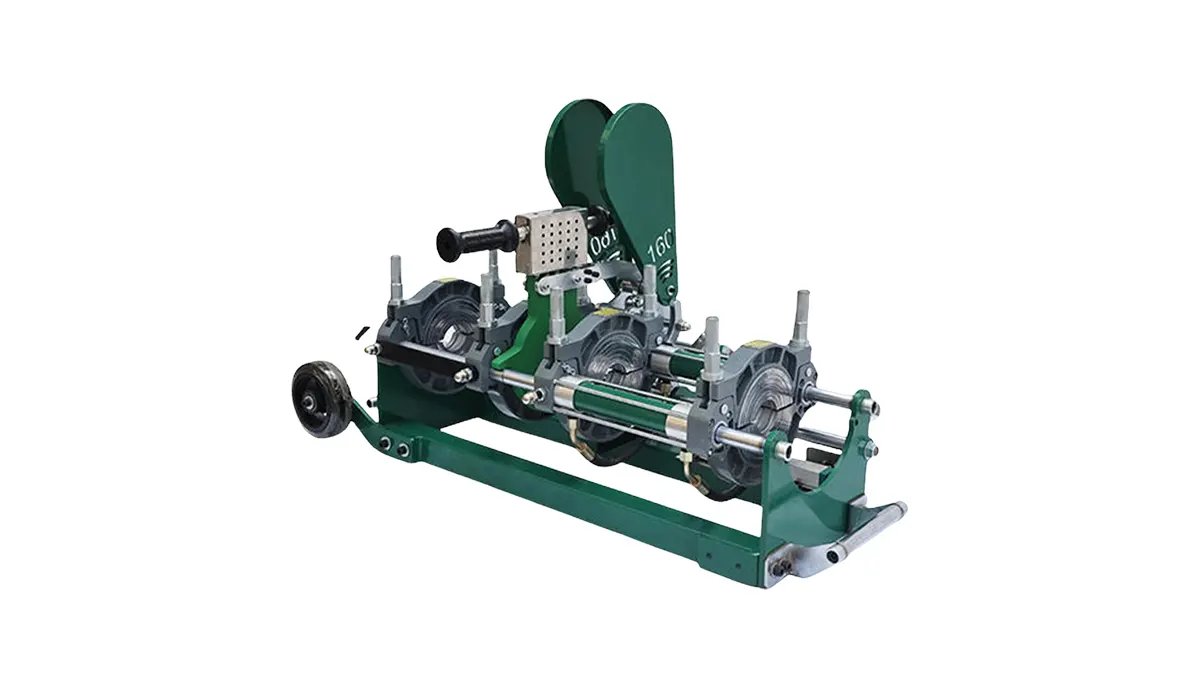
JQA160mm Automatic Butt Fusion Machine
- Welding Range: 50mm – 160mm
- Standard Power: 2.45 kW / 220V
- Data Storage: 2000+ Cycles
- Applicable Material: PE100, PE80, PP, PVDF
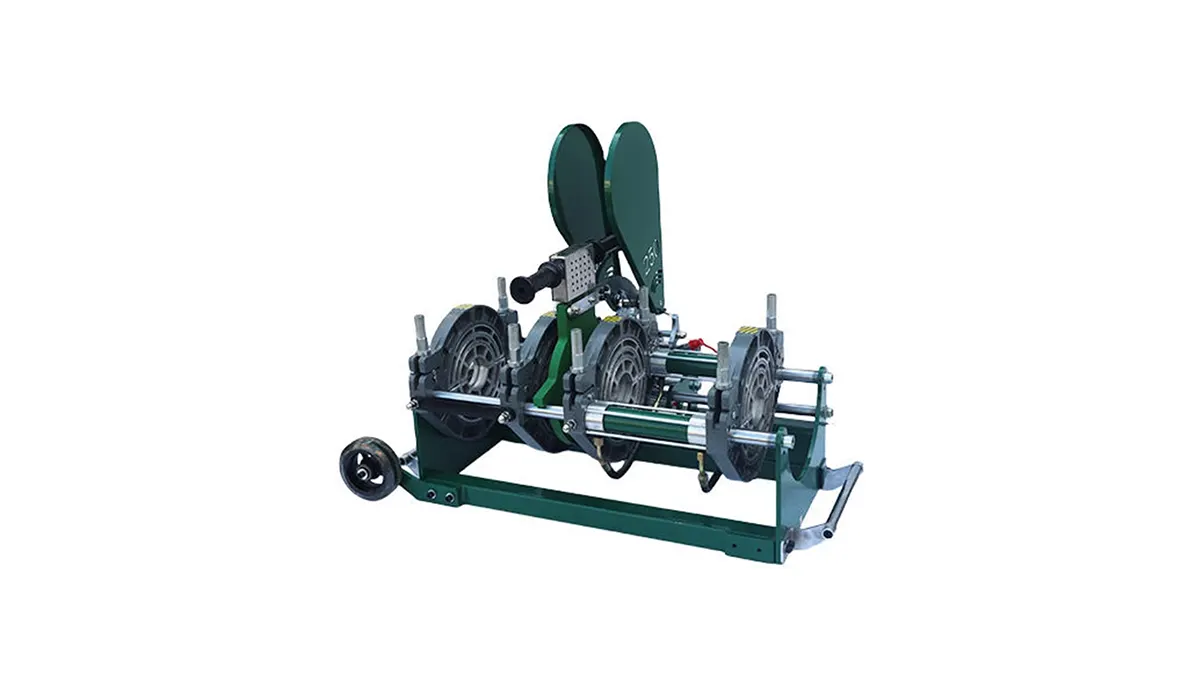
JQA250mm Automatic Butt Fusion Machine
- Welding Range: 90mm – 250mm
- Standard Power: 3.85 kW / 220V
- Hydraulic Unit: Servo Proportional Valve
- Standard Standard: ISO 21307 / DVS 2207
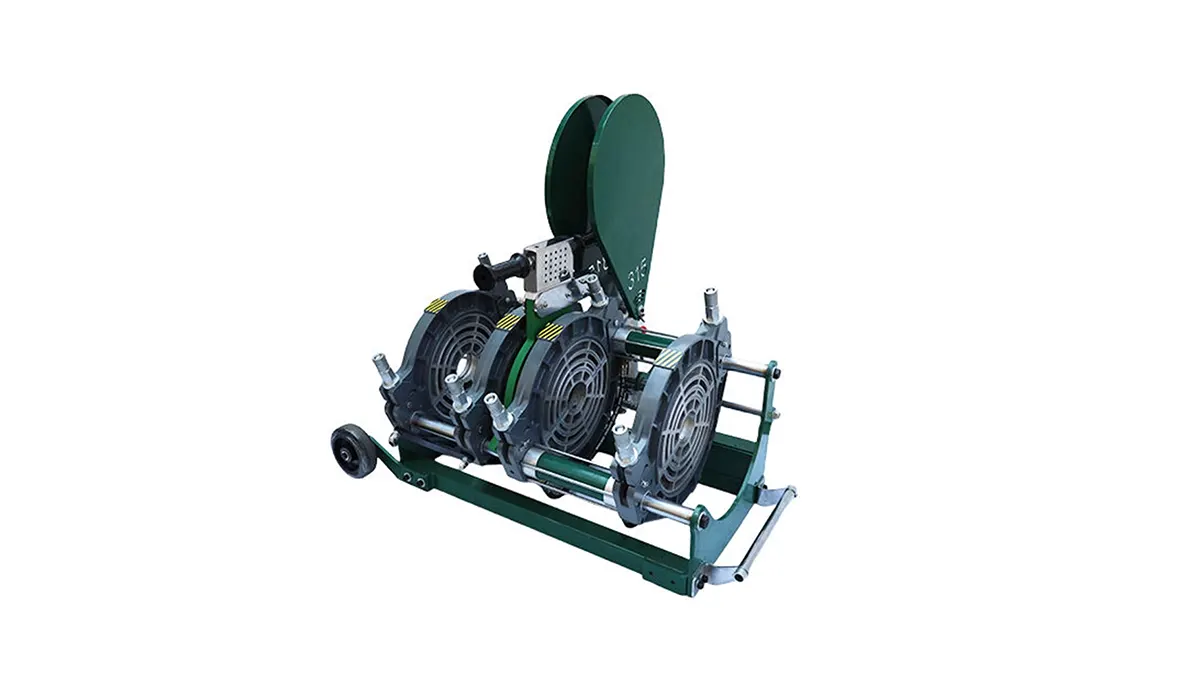
JQA315mm Automatic Butt Fusion Machine
- Welding Range: 90mm – 315mm
- Standard Power: 4.85 kW / 220V/380V
- Hydraulic Pressure: 0 – 6.3 MPa
- Controller: Touch HMI PLC System
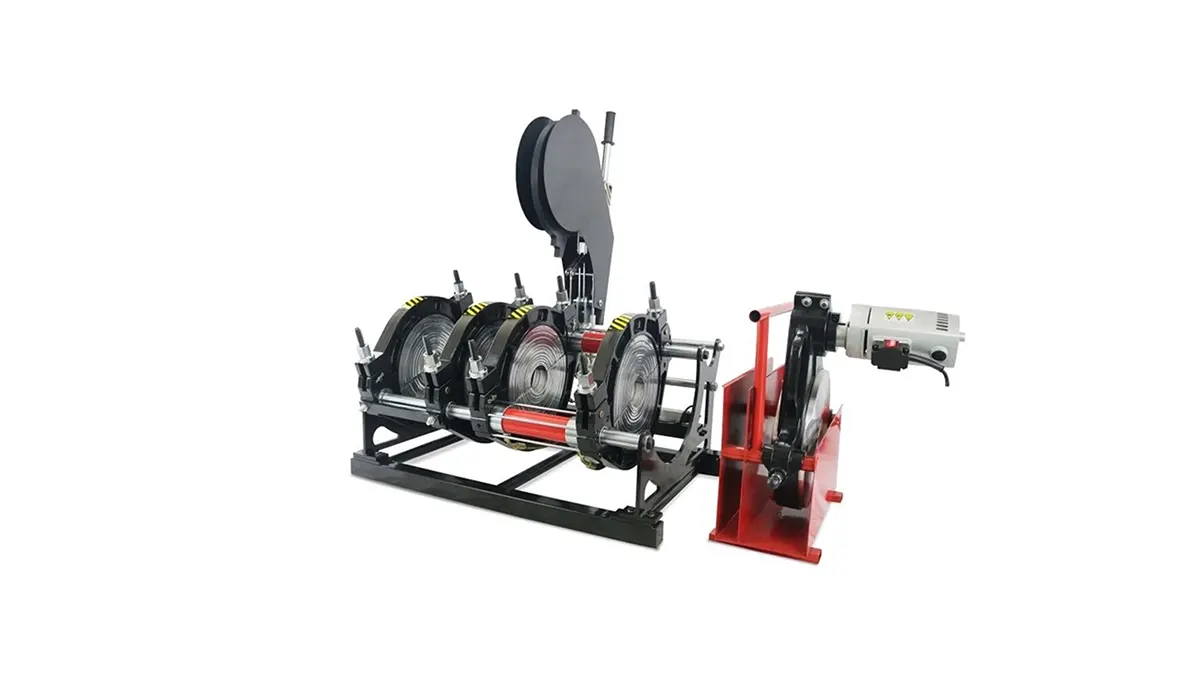
JQA355mm Automatic Butt Fusion Machine
- Welding Range: 110mm – 355mm
- Standard Power: 5.85 kW / 380V
- Plate Extraction: Automatic Spring/Hydraulic
- Certification: CE / ISO / SGS
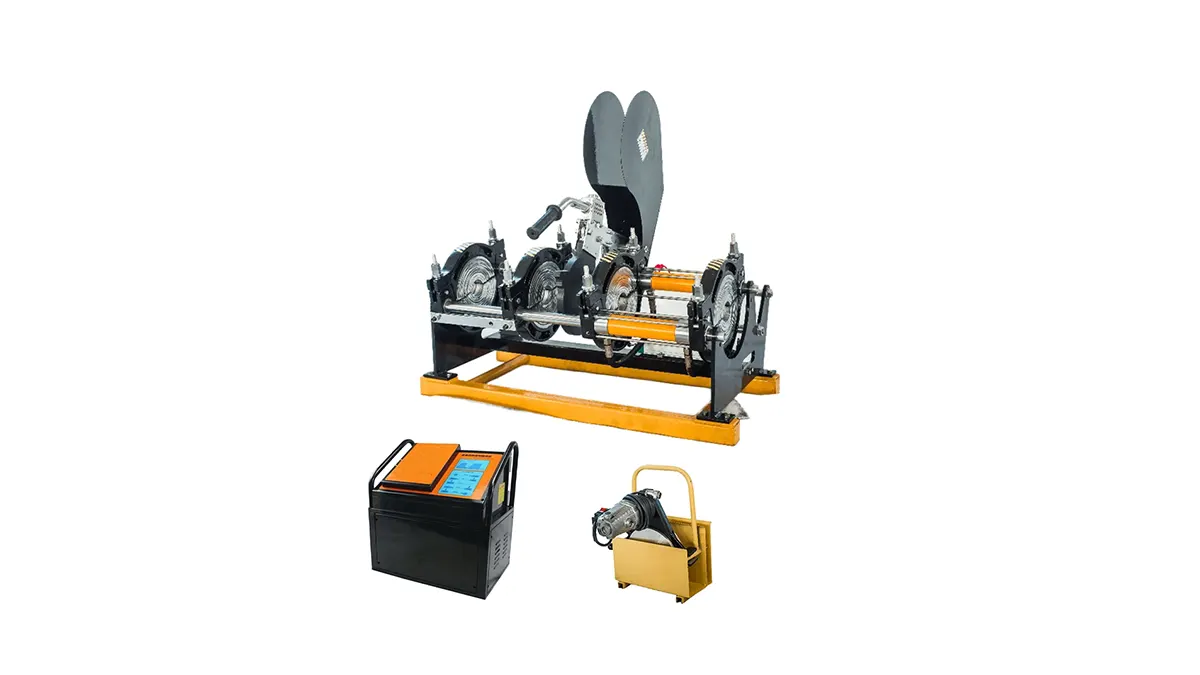
JQA500mm Automatic Butt Fusion Machine
- Welding Range: 250mm – 500mm
- Standard Power: 9.5 kW / 380V
- Clamping: Hydraulic Top Clamps Option
- Protocol: Multi-Standard Preloaded
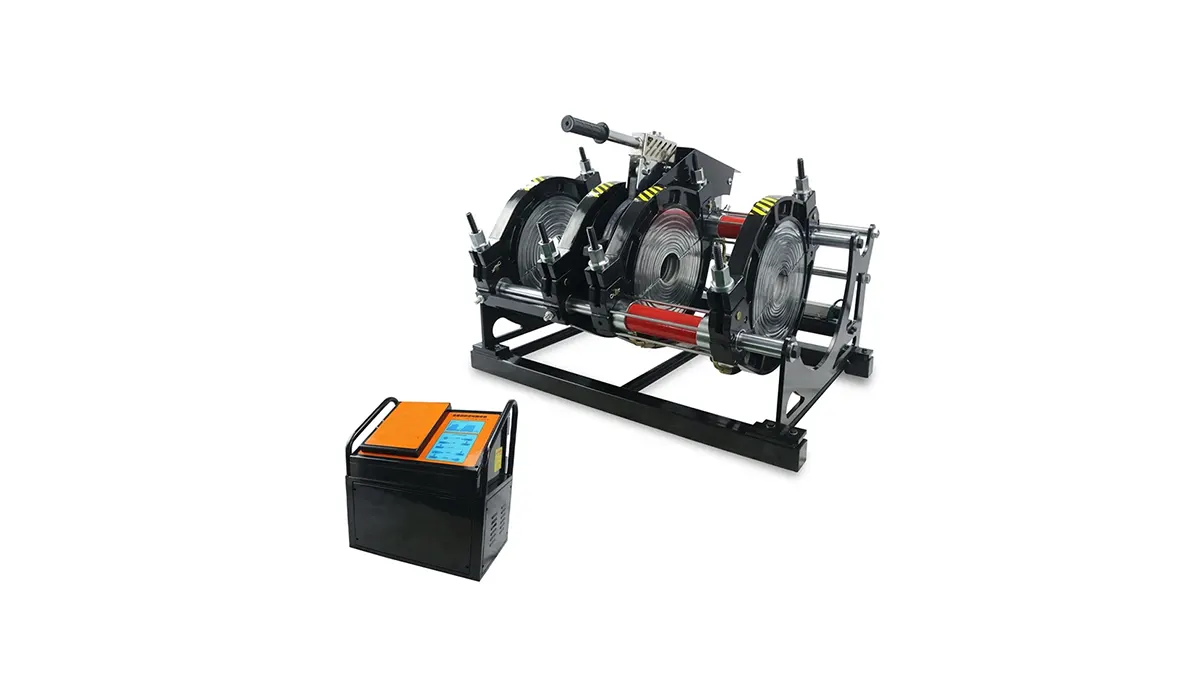
JQA630mm Automatic Butt Fusion Machine
- Welding Range: 315mm – 630mm
- Standard Power: 12.35 kW / 380V
- Chassis: Reinforced 4-Clamp Frame
- Interface: Multilingual Touchscreen
Global Standards & Parameter Governance for HDPE Butt Fusion
Industrial-grade thermoplastic pipelines demand strict alignment with international harmonized standards. JQ-Fusion automatic machines incorporate native algorithms adhering strictly to global pipeline design authorities.
Major Global Fusion Standards Supported
An automatic butt fusion system comes pre-programmed with exact formulas for calculating interfacial area based on outer diameter (OD) and wall thickness ratio (SDR), supporting:
- ISO 21307: Covers single low-pressure, dual low-pressure, and high-pressure butt fusion procedures for ISO 4427 PE water pipes and gas networks.
- ISO 12176-1: Sets stringent manufacturing thresholds for PE butt fusion equipment standard hardware, sensors, and structural deflection limits.
- ASTM F2620: Standard Practice for Heat Fusion Joining of Polyethylene Pipe and Fittings across North American municipal and energy sectors (ASTM D2513 PE gas pipe).
- DVS 2207-1: The benchmark German standard for welding thermoplastics, governing precise thermal plate soaking durations.
- PPI Technical Guidelines: Detailed guidance from the PE butt fusion process literature published by the Plastics Pipe Institute.
Why Pressure Formulas Require Real-Time CNC Computing
The exact hydraulic gauge pressure ($P_{gauge}$) required during fusion is mathematically calculated as:
In standard manual setups, operators often overlook variations in Drag Pressure caused by terrain slope, pipe roller friction, or long pulling runs. An Automatic Butt Fusion Machine measures drag precisely at every single joint and updates hydraulic output instantaneously.
Critical Industries Relying on Automatic Butt Fusion
Wherever joint failure leads to hazardous leaks, costly downtime, or environmental catastrophes, automatic CNC butt fusion is the mandatory joining methodology.
Natural Gas Transmission
Complies with zero-leakage mandates on PE gas piping systems. Automatic logging ensures regulatory audit compliance for gas utility operators worldwide.
Municipal Water Infrastructure
Supports large-diameter potable water transmission, sewage mains, and intake pipelines using robust ASTM F714 PE pipe materials without internal bead constriction.
Mining & Slurry Transport
Thick-walled HDPE pipelines subjected to high abrasive stress rely on CNC thermal soaking to prevent embrittlement in industrial PE piping systems.
Trenchless HDD Pullback
Horizontal Directional Drilling exerts immense tensile strain on fused strings. Automatic machines ensure 100% parent-pipe strength across every welded seam.
Factory Precision, Quality Assurance & Global Certifications
At JQ-Fusion, every automatic fusion machine undergoes multi-stage dynamic calibration, including clamp alignment laser checks, hydraulic pressure holding tests, and heating plate thermal imaging before packing.
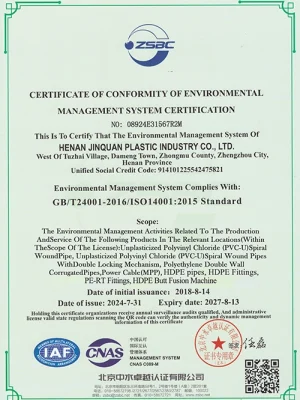
ISO Quality Management
Manufactured under strict ISO 9001 quality management systems guaranteeing component longevity.
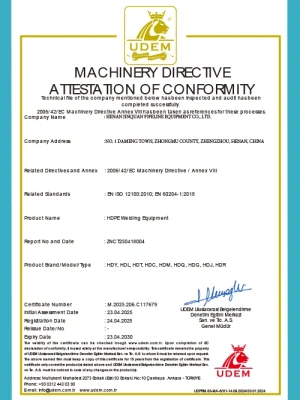
CE European Conformity
Full compliance with low voltage, electromagnetic compatibility, and machinery safety directives.
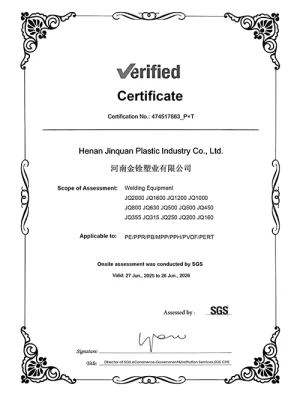
SGS Verified Facility
Independently verified manufacturing standards, electrical assemblies, and hydraulic pressure testing.
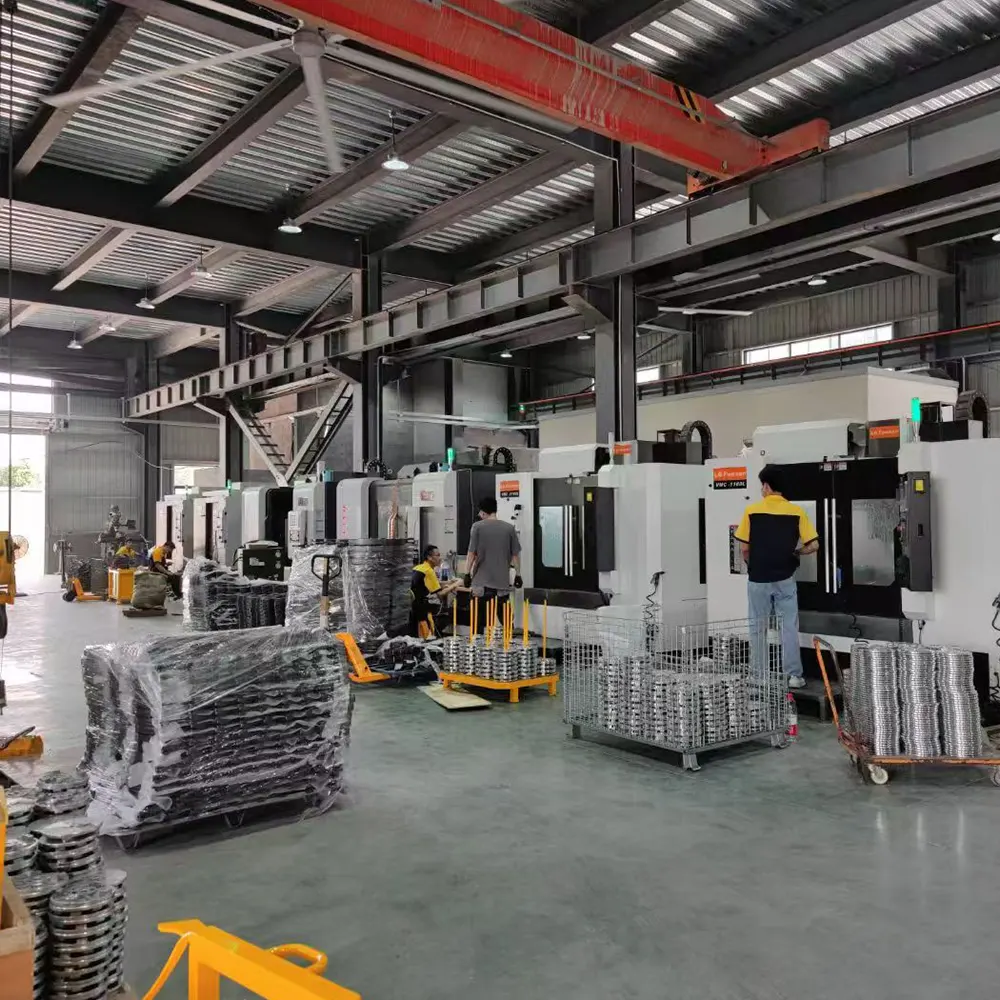
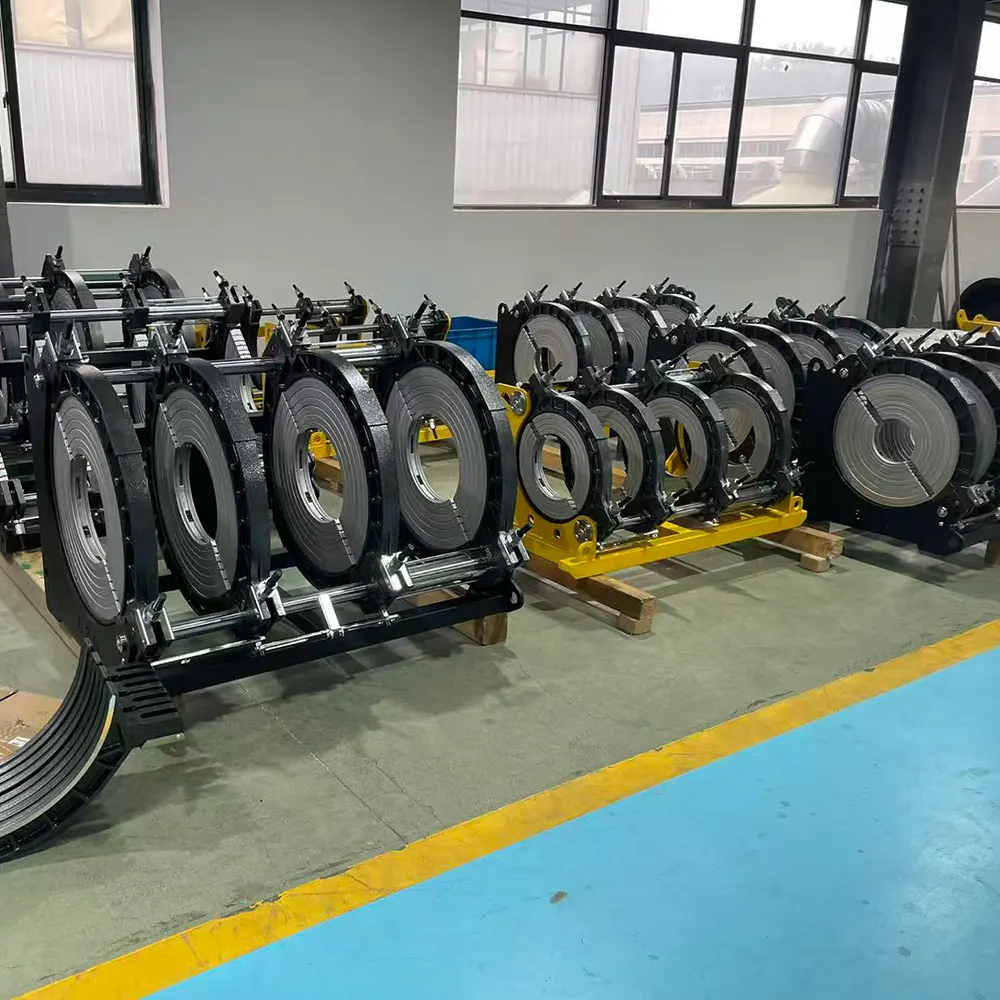
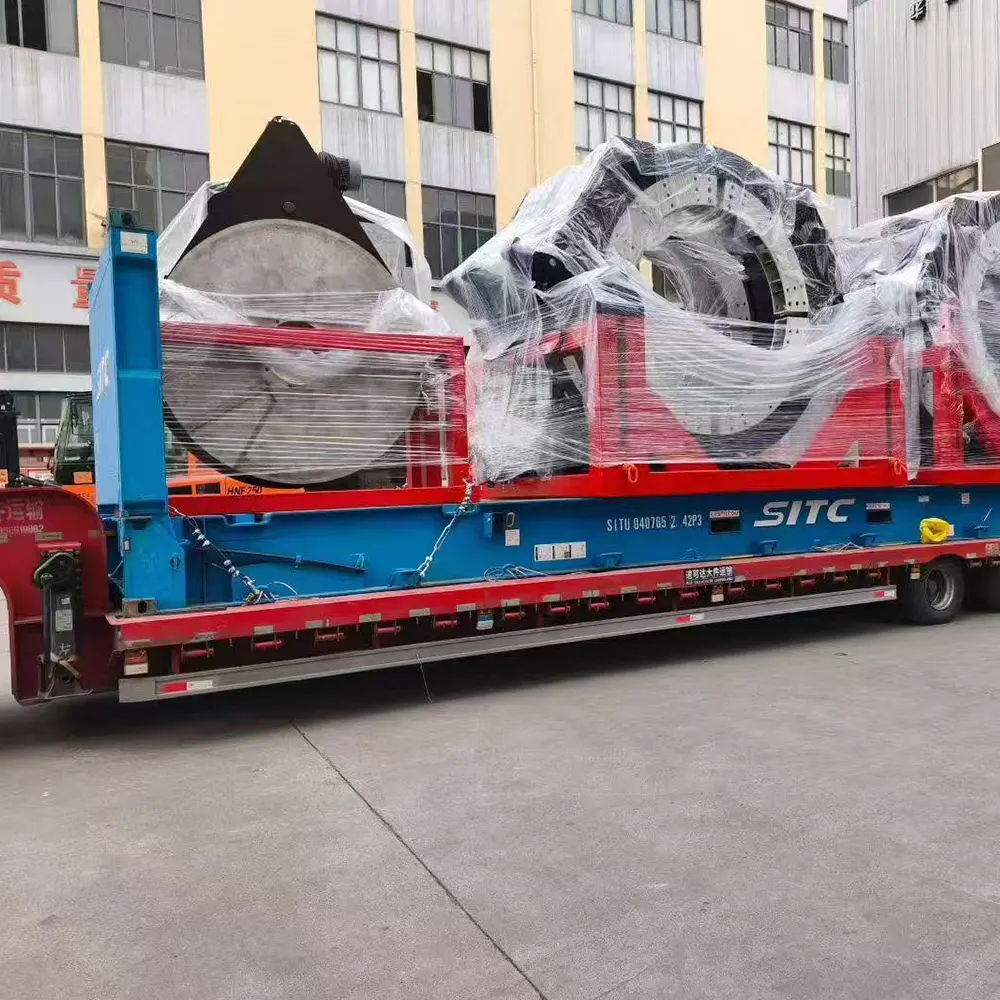
Factory Inventory & Ready-to-Ship Production Line
With a massive standardized stock of hydraulic frames, CNC power packs, and aluminum insert clamps, JQ-Fusion guarantees short lead times for urgent project mobilizations.
Preventative Maintenance & Field Calibration Protocol
To maintain micro-millimeter precision and extend machine operational lifespan across tough outdoor environments, follow these engineering best practices:
1. Heating Plate PTFE Care
Clean the Teflon heating surfaces before every weld using non-synthetic lint-free cloths and approved isopropanol solvent. Never use wire brushes or metallic blades that degrade PTFE coating uniformity.
2. Hydraulic Fluid Hygiene
Monitor hydraulic oil cleanliness and viscosity quarterly. Ensure anti-wear hydraulic oil (ISO VG 46 or 32 for cold climates) is free from dirt, dust, and moisture ingress to protect proportional valves.
3. Planer Blade Indexing
Inspect facing tool blades regularly. Dulled or chipped dual-edge blades create uneven frictional heat and irregular end gaps, which compromise automated alignment calculations.
Frequently Asked Questions (FAQ)
Detailed answers to essential technical, operational, and standard compliance questions regarding Automatic Butt Fusion Machines.
1. What is the primary difference between a hydraulic butt fusion machine and an automatic butt fusion machine?
A standard hydraulic butt fusion machine requires the operator to manually read pressure charts, adjust pressure regulator valves, track timers for heating and cooling, and manually open/close clamps. In contrast, an Automatic Butt Fusion Machine (CNC) utilizes a programmable logic controller (PLC) and servo-controlled hydraulic valves that automatically compute pipe dimensions, measure drag, regulate pressure curves, manage changeover times, lock cooling cycles, and export complete weld logs without human variance.
2. How does the CNC automatic machine account for outdoor temperature extremes?
JQ-Fusion automatic units are equipped with ambient temperature sensors. The internal controller automatically adjusts heating durations and provides environmental compensation offsets according to ISO/DVS standards when operating in cold weather or desert conditions.
3. Can the automatic butt fusion machine weld different types of thermoplastic materials?
Yes. The system supports pre-configured and customizable parameter sets for HDPE (PE80, PE100, PE-RT), Polypropylene (PP, PP-R, PP-H), and PVDF. The operator simply selects the resin grade, diameter, and SDR from the touchscreen menu.
4. How are joint records exported and verified for QA/QC compliance?
Weld data can be exported via USB flash drive or optional wireless transmission in encrypted PDF or CSV formats. The data record includes machine serial number, operator ID, GPS coordinates, timestamp, target vs. actual pressure profiles, temperature graphs, and joint acceptance pass/fail status compliant with ISO 12176-4.
5. Does an automatic machine require specialized operator training?
While automatic machines eliminate manual calculation mistakes, operators should be trained in proper pipe alignment, clamping torque, facing inspection, and basic machine maintenance according to heat fusion operator qualification guidelines. JQ-Fusion provides comprehensive video manuals and technical support.
Upgrade Your Pipeline Fleet with CNC Automatic Butt Fusion Machines
Partner directly with JQ-Fusion, the leading manufacturer of automated thermoplastic pipe welding systems. Get direct factory pricing, OEM/ODM customization, and responsive global technical support.
- Email: [email protected]
- Phone: +86 15093385787
- Facility: Zhengzhou, Henan, China